
Diamond wire cutting for metal sections, cable, wire rope and composite-metal stacks. This page covers where wire beats abrasive and where it does not.
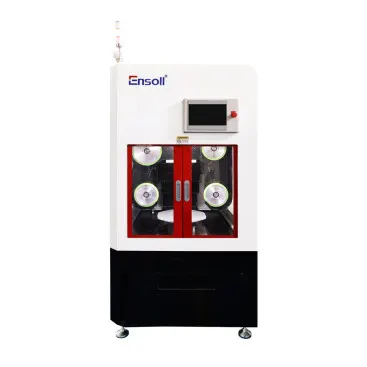
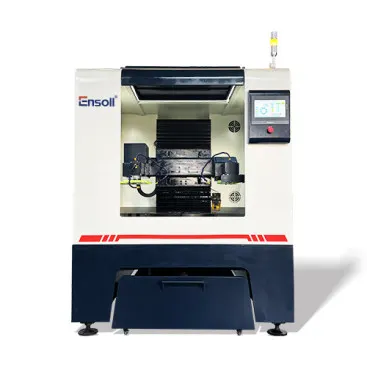
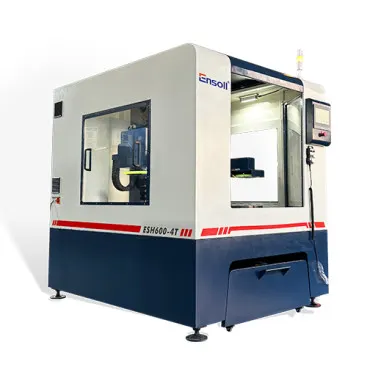
When wire beats an abrasive wheel on metal
Abrasive cutting is cheap and forgiving, and on plain carbon steel up to about 50 mm it remains the right answer. Wire wins in four specific situations:
- Heat-affected zone matters — abrasive cutting burns; a cooled wire cut leaves a HAZ measured in tens of microns.
- The section is mixed — steel bonded to rubber, copper inside a jacket, wire rope inside a ferrule. Abrasive smears these; wire separates them.
- The cut must be straight and burr-free — for subsequent welding or for cable terminations, the burr from an abrasive wheel is a defect.
- The part cannot be moved to a saw — portable loop saws cut in place.
Cable and wire rope specifically
Cutting cable is a different problem from cutting solid: the strands move. If the wire loads the rope before it has been restrained, the strands splay and the termination fails. The standard sequence is to bind the rope on both sides of the cut line, cut through the bindings, and only then release.
| Workpiece | Wire Ø | Note |
|---|---|---|
| Steel wire rope, 6–50 mm | 0.6–1.2 mm | Bind both sides; cut through the binding |
| Armoured / lead-sheathed cable | 0.8–1.4 mm | Expect wire consumption at the steel-to-lead transition |
| Aluminium conductor | 0.6–1.0 mm | Loads the wire — reduce feed, increase coolant |
| Metal-composite stack | 0.5–0.9 mm | Feed must be set for the hardest layer |
Soft metals are the hard case
Aluminium, copper and lead do not cut — they smear. The wire loads, the abrasive dulls within metres, and the cut degenerates into a plough. Counter-intuitively the fix is not a finer wire but a coarser, more open abrasive with heavier coolant flow, so the chip leaves the kerf instead of welding to the wire.
What to measure on the first cut
Cut a scrap piece of the same construction, then check: burr height at the exit, HAZ on a polished cross-section, wire diameter loss, and whether the cut face shows a change in finish at any layer boundary. That last one tells you where the feed needs to change.
자주 묻는 질문
Can I cut hardened steel with diamond wire?
예, and the harder the better — diamond wire performs best where the material cannot smear. Above 50 HRC the cut is clean and the HAZ is minimal.
Is diamond wire slower than a bandsaw on steel?
On solid mild steel, 네, considerably. The case for wire on metal is never throughput; it is cut quality, mixed sections and in-place cutting.
How do I stop the wire loading on aluminium?
Coarser abrasive, higher wire speed, much higher coolant flow, and a feed low enough that the chip clears before it welds. If it still loads, the coolant is not reaching the kerf.