Präzises Schneiden von magnetischem Material mit Diamantdrahtschlinge: 2 mm-Testdaten
Sample testing for a European client (Company P) · Ring diamond wire cutting process
Überblick
This report documents precision slicing of magnetic material using a ring diamond wire cutting system. The evaluation covers equipment and wire selection, cutting methodology, process parameters, and the resulting thickness uniformity, Maßgenauigkeit, surface quality and edge integrity of the sliced parts. Test results indicate that a gantry-type ring diamond wire machine, oil-based cooling and lubrication, and appropriately matched process parameters deliver stable, high-precision slicing of magnetic material.
1. Test Specimen
| Parameter | Wert |
|---|---|
| Material | Magnetic material |
| Härte | approx. 6–7 Mohs |
| Werkstückabmessungen | 60 mm × 26.0 mm × 3.0 Mm |
| Target slice dimensions | 2.0 mm × 26.0 mm × 3.0 Mm |
2. Equipment and Wire Selection
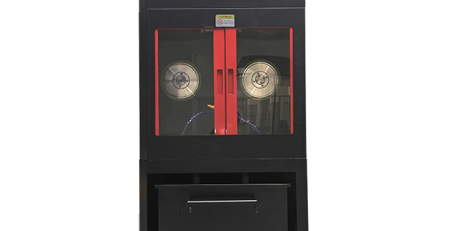
Equipment: ESO-GM. In view of the hard-brittle characteristics of magnetic material and the requirement to slice at a 2 mm schneiden, Ensoll selected the ESO-GM gantry-type ring diamond wire cutting system with a top-down vertical feed. The gantry configuration maintains a stable wire trajectory and slice dimensional accuracy.
Kühlmittel: oil-based cutting. Cutting oil is used as the cooling and lubricating medium. It improves lubrication and heat dissipation in the contact zone between the diamond wire and the magnetic material, reduces friction resistance and localised heat accumulation during cutting, and limits fluctuation in cutting load and its effect on the material. This helps suppress chipping, micro-cracking and surface damage.
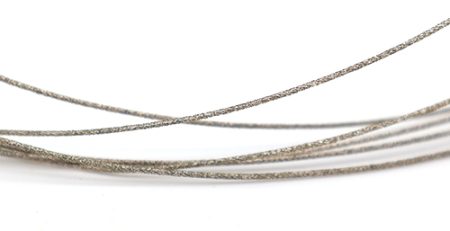
Draht: fully plated. A fully plated diamond wire was selected. Die plattierte Konstruktion verbessert die Bindungsfestigkeit zwischen den Diamantkörnern und dem Drahtkern und sorgt für eine gleichmäßigere Kornverteilung. Dies gewährleistet eine kontinuierliche und stabile Materialabtragsrate, reduziert Kornverlust und Drahtverschleiß, und trägt zu weniger Absplitterungen, micro-cracking and surface damage when slicing magnetic material.

3. Schneidverfahren und Gerätevorteile
Portal-Schneidkonfiguration. Die Portalkonstruktion bietet eine hohe Gesamtsteifigkeit und Laufruhe. The top-down vertical feed helps keep the diamond wire trajectory stable and reduces the influence of changes in cutting force on kerf position and dimensional accuracy in the magnetic material. The machine is equipped with a mist-extraction system that promptly removes mist generated during cutting.
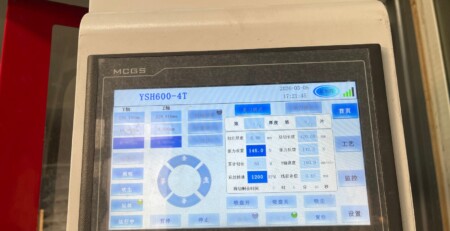
Intelligente Spannungsregelung. Das System passt die Spannung des Diamantdrahts in Echtzeit an die Schneidbedingungen an und unterstützt sowohl Konstantspannungs- als auch Variabelspannungsmodi, hält das Drahtlaufen stabil. Stable wire tension reduces fluctuation in the cutting trajectory and limits localised uneven loading and the risk of wire breakage caused by tension variation, which in turn reduces defects in the magnetic material.
Drahtbruchspeicher. Wenn der Diamantdraht reißt oder die Maschine abnormal stoppt, Das System zeichnet automatisch die aktuelle Bearbeitungsposition und den zugehörigen Betriebszustand auf. Nach dem Drahtwechsel, cutting resumes from the recorded position, reducing dimensional deviation and material loss caused by re-positioning and repeat machining. This improves the continuity of magnetic material slicing and lowers the risk of repeated cutting.
Hochsteifes einteiliges Graugussgestell. The one-piece cast iron frame provides high structural stiffness and vibration resistance, reducing the effect of machine vibration and structural deformation on the wire trajectory during machining. For a hard-brittle material such as magnetic material, the high-rigidity frame helps damp vibration and fluctuation in cutting force during the cut and keeps the diamond wire running stably.
4. Prozessparameter und Kühlmethode
| Parameter | Wert |
|---|---|
| Drahtdurchmesser (Mm) | 0.35 × 1880 |
| Drahtvorschubgeschwindigkeit (mm/min) | 2 |
| Schnittbreite (Mm) | 60 |
| Drahtspannung (N) | 140 |
| Drahtgeschwindigkeit (M/s) | 26 |
| Drahtbogenzeit (s) | 60 |

5. Schneidleistung und Ergebnisse

5.1 TTV-Testdaten (Einheit: Mm)
Gesamt-Dickenvariation (TTV) wurde mithilfe eines Neun-Punkte-Rasters gemessen, dual-probe thickness gauging method on a vacuum-chuck stage. The measurement was applied to magnetic material slices produced by ring diamond wire cutting. Before measurement the instrument was thermally stabilised and calibrated against a standard thickness block. Die nominelle Scheibendicke betrug 2.000 Mm.
| Probe | Neun-Punkte-Stärkemessungen | TMax | TMin | TTV |
|---|---|---|---|---|
| S01 | 1.992, 1.996, 1.998 1.995, 2.000, 2.003 1.997, 2.004, 2.006 |
2.006 | 1.992 | 0.014 |
| S02 | 1.988, 1.993, 1.997 1.995, 2.001, 2.004 1.999, 2.006, 2.008 |
2.008 | 1.988 | 0.020 |
| S03 | 1.985, 1.990, 1.994 1.992, 1.998, 2.002 1.996, 2.004, 2.009 |
2.009 | 1.985 | 0.024 |
| S04 | 1.994, 1.997, 2.000 1.996, 2.001, 2.004 1.999, 2.005, 2.007 |
2.007 | 1.994 | 0.013 |
| S05 | 1.989, 1.994, 1.997 1.993, 1.999, 2.003 1.996, 2.005, 2.010 |
2.010 | 1.989 | 0.021 |
Bewertung. Nine-point grid measurement was applied to five magnetic material slices. TTV values were 0.014, 0.020, 0.024, 0.013 und 0.021 Mm, spanning 0.013–0.024 mm across the batch, with a mean TTV of approximately 0.018 mm bei einem 2.000 mm Nennstärke. The results confirm good thickness uniformity in magnetic material slicing.
5.2 Dicken-Toleranz-Daten (Einheit: Mm)
Thickness tolerance was derived from the nine-point thickness data, Verwendet 2.000 mm wie die Nenndicke. The positive and negative thickness deviation were calculated at each measurement position and the results from all five samples were aggregated. The maximum positive deviation, maximum negative deviation and overall deviation range were then determined to evaluate thickness consistency.
| Probe | Mittlere Dicke | Dickenabweichung |
|---|---|---|
| S01 | 1.999 | −0.001 |
| S02 | 1.999 | −0.001 |
| S03 | 1.997 | −0.003 |
| S04 | 2.000 | 0.000 |
| S05 | 1.998 | −0.002 |
| Maximale positive Abweichung | — | +0.010 Mm |
| Maximale negative Abweichung | — | −0.015 mm |
| Dicken-Toleranzbereich | — | ±0.0125 mm |
Bewertung. Gegenüber einer nominalen Dicke von 2.000 Mm, the five slices showed mean thicknesses of 1.997–2.000 mm, with small average deviations across the batch. Over all measurement points the thickness deviation ranged from −0.015 mm to +0.010 Mm, with a maximum absolute deviation of 0.015 Mm.
5.3 Oberflächenrauheit Ra-Daten (Einheit: μm)
Oberflächenrauheit (Ra) was measured by stylus profilometry on the magnetic material slices after ring diamond wire cutting. Representative measurement positions were taken at the centre and on both sides along the cut end face, surface profile data was acquired with a stylus profilometer, and the roughness parameter Ra was recorded at each position.
| Probe | Centre | Mid-left | Mid-right | Mittlerer Ra |
|---|---|---|---|---|
| S01 | 0.52 | 0.56 | 0.49 | 0.52 |
| S02 | 0.48 | 0.53 | 0.50 | 0.50 |
| S03 | 0.61 | 0.66 | 0.58 | 0.62 |
| S04 | 0.46 | 0.51 | 0.48 | 0.48 |
| S05 | 0.55 | 0.59 | 0.53 | 0.56 |
Bewertung. Mean Ra across the five samples ranged from 0.48 An 0.62 μm, mit allen einzelnen Messwerten zwischen 0.46 und 0.66 μm. The narrow spread across the three measurement positions on each slice indicates a uniform surface finish along the cut face.
5.4 Edge Chipping Data (Einheit: μm)
Edge chipping was quantified by optical imaging on a toolmaker’s microscope. Specimen edges were cleaned before measurement and the magnification and measurement scale of the instrument were calibrated. The slice edge was then inspected under the microscope, identifiable chipping defects were located and measured at four points per sample, and the maximum value was retained.
| Probe | Point 1 | Point 2 | Point 3 | Point 4 | Max. Absplitterungen |
|---|---|---|---|---|---|
| S01 | 4.2 | 5.1 | 4.8 | 5.6 | 5.6 |
| S02 | 3.8 | 4.6 | 5.2 | 4.4 | 5.2 |
| S03 | 5.6 | 6.8 | 7.5 | 6.2 | 7.5 |
| S04 | 3.5 | 4.1 | 4.6 | 3.9 | 4.6 |
| S05 | 4.9 | 5.7 | 6.3 | 5.2 | 6.3 |
Bewertung. Toolmaker’s microscope inspection of the five magnetic material slices gave maximum chipping values of 5.6, 5.2, 7.5, 4.6 und 6.3 μm, with an overall maximum of 7.5 μm. S04 showed the best edge integrity and S03 the largest chipping at 7.5 μm.

6. Schlussfolgerung
The good results obtained in this high-precision slicing trial of magnetic material stemmed mainly from the combined effect of a purpose-built cutting machine, the cooling and lubrication method, and correctly matched process parameters. Magnetic material is relatively hard with a degree of brittleness. During ring diamond wire cutting the abrasive grains act continuously on the material surface, and material removal is affected by cutting load, wire running condition and the machining parameters.
Equipment. An ESO-GM gantry-type ring diamond wire cutting system was used. The gantry structure provides high overall rigidity and running stability and gives reliable mechanical support for workpiece clamping and continuous wire travel. Stable motion and feed control keep the diamond wire on the programmed path throughout the cut.
Kühlung und Schmierung. Cutting oil was used as the cooling and lubricating medium. During cutting the diamond wire remains in continuous contact with the workpiece and the abrasive grains grind the material continuously, generating friction heat in the contact zone. Cutting oil improves lubrication at the cutting interface, carries away part of the cutting heat, and reduces friction between the wire and the workpiece, which helps limit thermal effects and edge damage.
Process parameters. Drahtgeschwindigkeit, feed rate and other key parameters were matched to the hardness, brittleness and target slice thickness of the magnetic material. Parameters were set to maintain stable wire travel and continuous material removal, avoiding feed rates high enough to raise cutting load, or a mismatch between wire speed and feed rate that would degrade slice quality.
Insgesamt. Taken together with slice dimensional accuracy, Dickenabweichung, Oberflächenrauheit (Ra) and cut-edge quality, the combination of the ESO-GM gantry cutting machine, oil-based cooling and lubrication, and appropriately matched process parameters allows ring diamond wire cutting to meet the precision slicing requirements for this magnetic material.