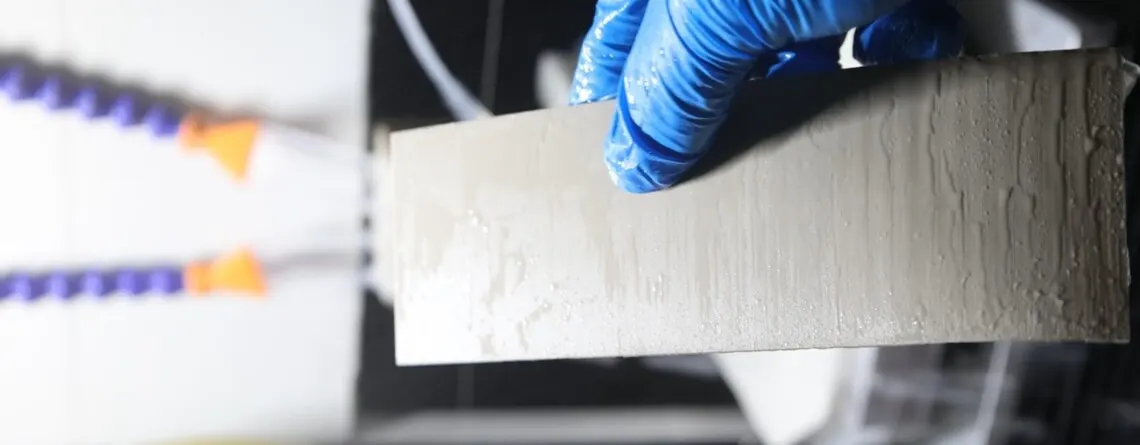
PEEK vs Espuma PMI: Comparação de Corte com Fio de Diamante
Abstrair: PEEK and PMI foam sit at opposite ends of the material spectrum that a
Loop de fio de diamante has to handle – one is a dense, tough thermoplastic, the other a
low-density cellular structural foam. This comparison sets Ensoll’s two published slicing tests side by side:
uma 200 mm x 60 mm x 60 mm PEEK block cut into 6.5 mm slices with cutting fluid, and four 400 mm x 400 mm PMI
foam slices cut to 0.8 mm dry. It compares the failure modes, the parameter sets
(uma máquina de serra de fio diamantado dedicada in both cases) and the measured quality results, and gives the
rule for deciding which starting point to use.
Principais Conclusões
- PEEK is limited by cutting heat (it is a thermoplastic that softens at the kerf); PMI foam is limited by cutting load (its cell skeleton compresses and tears).
- PEEK was cut wet at a 3 avanço mm/min; PMI foam was cut dry at 100 mm/min – a two-order-of-magnitude difference in feed rate for essentially the same wire speed.
- PEEK: TTV 0.072-0.098 milímetro (mean 0.085 milímetro), tolerance +/-0.037 milímetro, Ra 0.76-0.95 μm, chipping max 6.7 μm, on 6.5 mm slices.
- Espuma PMI: TTV 0.013-0.050 milímetro (mean 0.036 milímetro), tolerance +/-0.043 milímetro, Ra 0.68-0.82 μm, chipping max 7.1 μm, on 0.8 mm slices.
- Os dois conjuntos de parâmetros não são intercambiáveis – o diâmetro do fio, tensão, a taxa de alimentação e o método de arrefecimento são todos diferentes.
Dois Materiais, Dois Modos de Falha Diferentes
A razão pela qual PEEK e espuma de PMI necessitam de diferentes definições de processo não é apenas a dureza – é o que acontece quando
a janela de processo é excedida.
O PEEK é um termoplástico de alto desempenho com elevada tenacidade, resistência ao desgaste e resistência ao calor. Sob
o corte com fio de diamante tem um mecanismo de remoção diferente dos materiais duros e frágeis: porque o material tem
plasticidade e tenacidade, A ação contínua dos grãos abrasivos gera calor de corte. Se esse calor
não puder dissipar-se, a zona de usinagem amolece localmente e a resistência de corte aumenta, produzindo
desvio dimensional, rebarbas nas arestas e qualidade de superfície degradada. A variável de controlo é portanto
temperatura.
Espuma de PMI é uma espuma estrutural de alto desempenho com baixa densidade, a uniform cellular structure and good
specific strength and stiffness. Its porous interior gives a removal behaviour quite unlike a dense material:
the abrasive grains act on the foam skeleton, and if the cutting load is too high or the parameters are poorly
matched, the cells are compressed and torn and the cut face becomes uneven, which feeds directly into slice
thickness and surface quality. A variável de controlo é portanto load.
Material and Workpiece Comparison
| Item | PEEK | Espuma PMI |
|---|---|---|
| Material class | High-performance thermoplastic | High-performance structural foam |
| Dureza | Approximately MH 6.5 | Approximately MH 2 |
| Tamanho da peça | 200 mm x 60 mm x 60 milímetro | 400 mm x 400 mm x 50 milímetro |
| Slice produced | 6.5 mm x 60 mm x 60 milímetro | 400 mm x 400 mm x 0.8 milímetro |
| Densidade | Dense, solid | Baixa densidade, cellular |
| Governing failure mode | Cutting heat – local softening, burrs | Carga de corte – cell compression and tearing |
| Arrefecimento | Cutting fluid (continuous) | Dry cutting |
Parameter Comparison
| Parâmetro | PEEK | Espuma PMI |
|---|---|---|
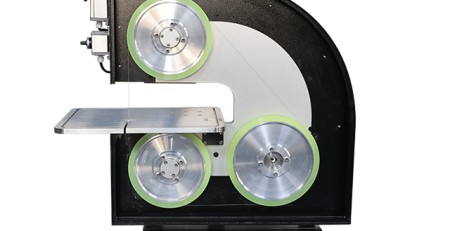
| Máquina | ESO-GM gantry-type | ESH600-4T horizontal |
| Wire diameter x loop length (milímetro) | 0.35 x 1880 | 0.60 x 3460 |
| Tipo de fio | Fully coated | Fully coated |
| Velocidade de alimentação (mm/min) | 3 | 100 |
| Largura de corte (milímetro) | 2 | 400 |
| Tensão do fio (N) | 150 | 145 |
| Velocidade do fio (M) | 24 | 25 |
| Wire-bow tensioning time (s) | 60 | 60 |
| Carga de corte (N·m) | 17 | 17 |
Result Comparison
| Medir | PEEK (6.5 mm slices) | Espuma PMI (0.8 mm slices) |
|---|---|---|
| Variação total de espessura (TTV) | 0.072-0.098 milímetro, mean 0.085 milímetro | 0.013-0.050 milímetro, mean 0.036 milímetro |
| Tolerância de espessura | +/-0.037 mm contra 6.500 mm nominais | +/-0.043 mm contra 0.800 mm nominais |
| Rugosidade média da superfície Ra | 0.76-0.95 μm (means 0.80-0.91 μm) | 0.68-0.82 μm |
| Quebra máxima da aresta | 6.7 μm (range 4.2-6.7 μm) | 7.1 μm (range 5.5-7.1 μm) |
| Sample count | 3 slices | 4 slices |
Reading the Differences: Three Rules
Rule 1 – Materiais dominados pela temperatura necessitam de arrefecimento; load-dominated materials do not
PEEK was cut with cutting fluid as the cooling medium to improve heat dissipation and lubrication at the wire
interface, limiting local softening, deformation and burrs. PMI foam was cut dry so that no liquid entered the
cells and no cleaning or drying step was needed afterwards. Choosing the wrong one is a process error in both
directions: dry-cutting PEEK risks a softened kerf, and wet-cutting PMI foam risks dimensional drift from
absorbed liquid.
Rule 2 – The soft material can run two orders of magnitude faster in feed
The PEEK feed rate was 3 mm/min; the PMI foam feed rate was 100 mm/min. That gap is not a machine difference,
it is the consequence of what limits the process. PEEK removal is limited by how much heat can be carried away,
so feed must stay low. PMI foam removal is limited by how much load the cell skeleton can take, and because the
foam is low density that ceiling is reached much later. Both tests used similar wire speed – 24 m/s for PEEK and
25 m/s for PMI foam – which confirms that feed rate, not wire speed, is the discriminating parameter.
Rule 3 – Compare each material against its own tolerance, not against the other
PMI foam produced TTV of 0.013-0.050 mm against PEEK’s 0.072-0.098 milímetro, but the slices were 0.8 mm e 6.5 milímetro
thick respectively and the tolerance requirement differs with the application. What both tests do show is a
stable process: PEEK held +/-0.037 mm thickness tolerance and PMI foam +/-0.043 milímetro, with Ra below 1 um in both
cases and edge chipping under 7.1 um in both cases.
Which Starting Point to Use
| If the material is… | Start from | First lever |
|---|---|---|
| A dense thermoplastic that softens with heat (PEEK, and similar engineering plastics) | ESO-GM style gantry machine, 0.35 mm fully coated wire, 24 M, 3 mm/min, 150 N, Fluido de corte | Velocidade de alimentação – keep heat generation low |
| A low-density cellular foam (PMI and similar structural foams) | ESH600-4T horizontal machine, 0.60 mm fully coated wire, 25 M, 100 mm/min, 145 N, dry | Velocidade de alimentação – keep load off the cell skeleton |
| Hard and brittle (silício, carboneto de silício, cerâmica, vidro óptico) | See the material-specific guides for the cluster | Wire specification and kerf control |
Common Mistakes When Switching Between the Two
- Carrying the feed rate across. A feed that is conservative for PMI foam is far too
aggressive for PEEK, and a feed that is right for PEEK leaves the PMI cut polishing rather than cutting. - Assuming coolant helps everywhere. On PMI foam, coolant is a dimensional risk rather than a
safety margin. - Judging the foam result by the plastic result. Um 0.8 mm foam slice and a 6.5 mm plastic
slice cannot be compared on raw TTV numbers. - Chasing wire speed. In both tests the wire speed sat in the same 24-25 m/s band, which is
the clearest sign that it is not the lever for quality on either material. - Ignoring the entry edge. Both materials need the wire bow to settle before feed engages; uma
60 s wire-bow tensioning time was used in both tests.
Full Test Data
The complete measurement sets – nine-point thickness readings, tolerance tables, Ra profiles and chipping
measurements – are published in the two source reports:
PEEK precision slicing with diamond wire loop and PMI foam precision slicing with
Loop de fio de diamante. The measurement method itself is described in the
guia de medição TTV de nove pontos.
Perguntas Frequentes
É mais difícil cortar PEEK ou espuma PMI com um fio de diamante??
Eles são duros de maneiras diferentes. PEEK é denso, tough thermoplastic: o risco é o aquecimento durante o corte, o que amolece o material no sulco e provoca desvios dimensionais e rebarbas. A espuma PMI é um sólido celular de baixa densidade: o risco é a carga de corte, o que comprime e rasga o esqueleto celular. Portanto, o PEEK precisa de refrigeração e avanço conservador, enquanto a espuma PMI necessita de controlo da carga e corte a seco.
Porque é que o PEEK é cortado com líquido e a espuma PMI a seco??
O PEEK é um termoplástico que amolece quando a zona de corte aquece, por isso usa-se fluido de corte para remover calor e lubricar a interface fio-material. A espuma PMI é porosa e absorve líquidos, por isso o refrigerante entraria nas células e teria depois de ser removido através de limpeza e secagem – daí usar-se corte a seco.
How different are the feed rates between the two materials?
Substantially. PEEK was sliced at a 3 velocidade de avanço de mm/min, while PMI foam ran at 100 mm/min. The dense thermoplastic needs slow feed to keep heat generation low; a espuma de baixa densidade tolera uma alimentação muito maior porque a remoção é limitada pela carga, não pelo calor. A velocidade do fio foi semelhante em ambos os testes, 24 m/s for PEEK and 25 m/s for PMI foam.
Qual material obteve melhores resultados dimensionais?
A espuma PMI apresentou a menor variação em termos absolutos – TTV 0.013-0.050 milímetro (média 0.036 milímetro) em comparação com o PEEK 0.072-0.098 milímetro (média 0.085 milímetro) – mas os dois não são diretamente comparáveis. As fatias de PEEK tinham 6.5 mm de espessura e as fatias de PMI 0.8 milímetro, e uma fatia mais fina é medida contra uma espessura nominal muito menor. Compare cada material com a sua própria tolerância de aplicação.
Pode um conjunto de parâmetros ser utilizado para ambos os materiais?
Não. Os conjuntos validados diferem no diâmetro do fio, taxa de avanço, tensão e método de arrefecimento. O PEEK utilizou um 0.35 x 1880 fio totalmente revestido a mm em 150 N tensão com fluido de corte; espuma PMI usada a 0.60 x 3460 fio totalmente revestido a mm em 145 N tensão com corte a seco. Comece cada material a partir da sua própria janela validada em referência de parâmetros de corte de espuma PMI.
Conteúdo técnico revisto pela equipa de engenharia da Ensoll – um fabricante de laços de fio de diamante com 10+ anos de experiência em produção.