Ductile Iron Precision Slicing with Diamond Wire Loop: 10 Données de test en mm
Sample testing for a European client (Company R) · Ring diamond wire cutting process
Aperçu
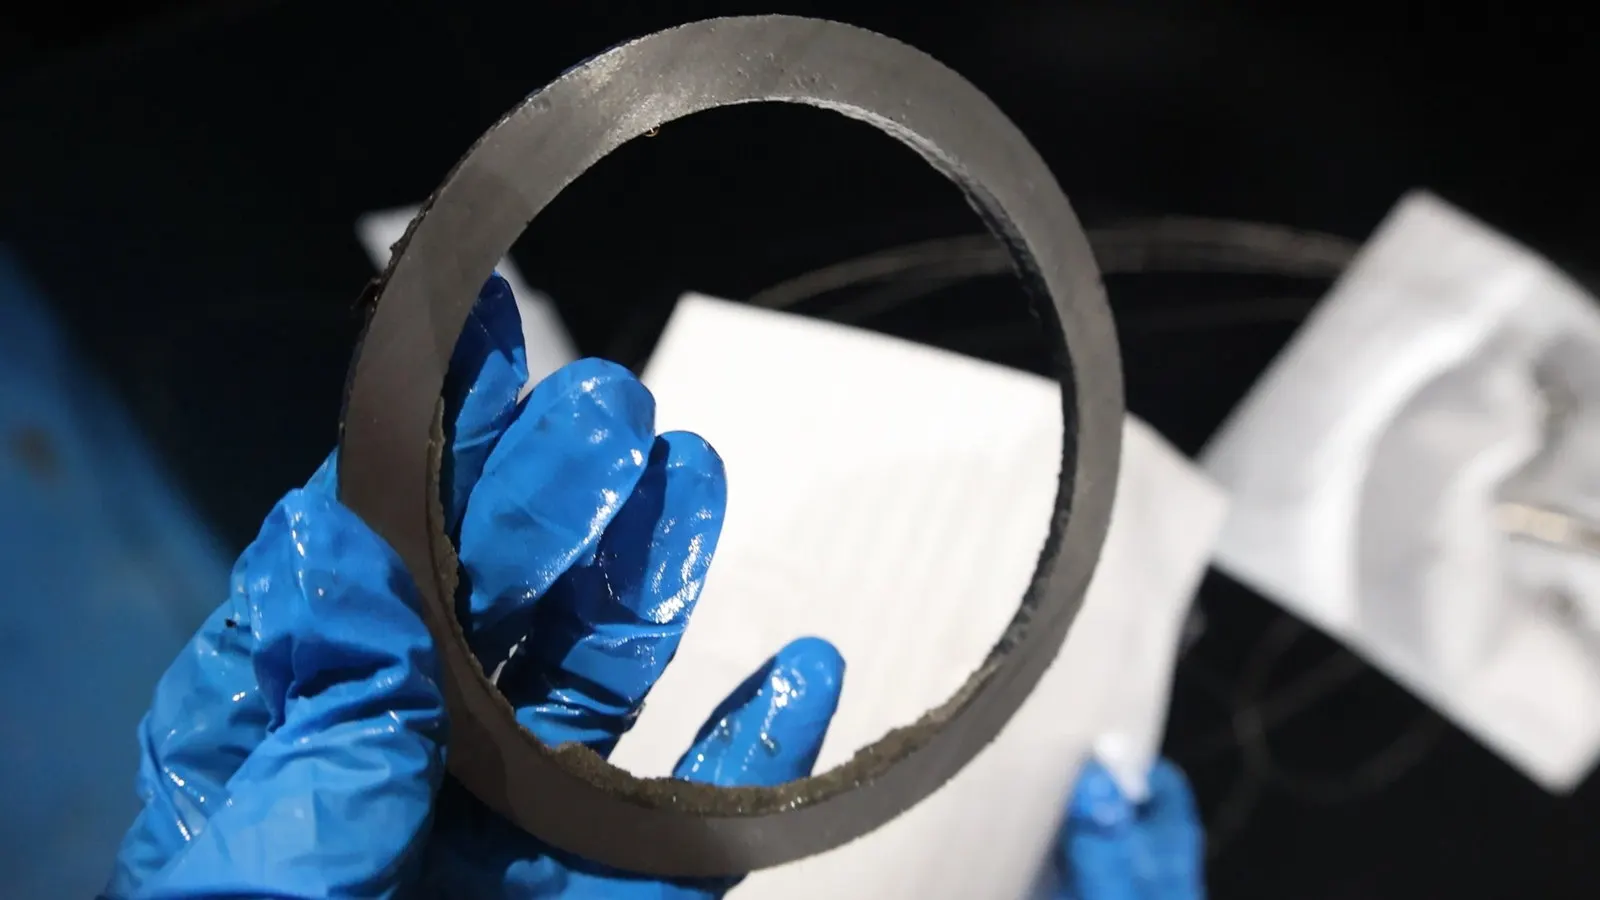
This report documents precision slicing of ductile iron using a ring diamond wire cutting system. The evaluation covers equipment and wire selection, cutting methodology, paramètres du processus, and the resulting thickness uniformity, la précision dimensionnelle, surface finish and edge integrity of the sliced parts. Test results indicate that a large-format ring diamond wire machine, oil-based cooling and lubrication, and appropriately matched process parameters deliver stable, high-precision slicing of ductile iron at production-representative section sizes.
1. Test Specimen
| Paramètre | Valeur |
|---|---|
| Matériau | Ductile iron (nodular cast iron) |
| Dureté | approx. 6–7 Mohs |
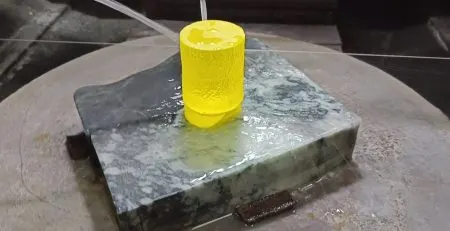
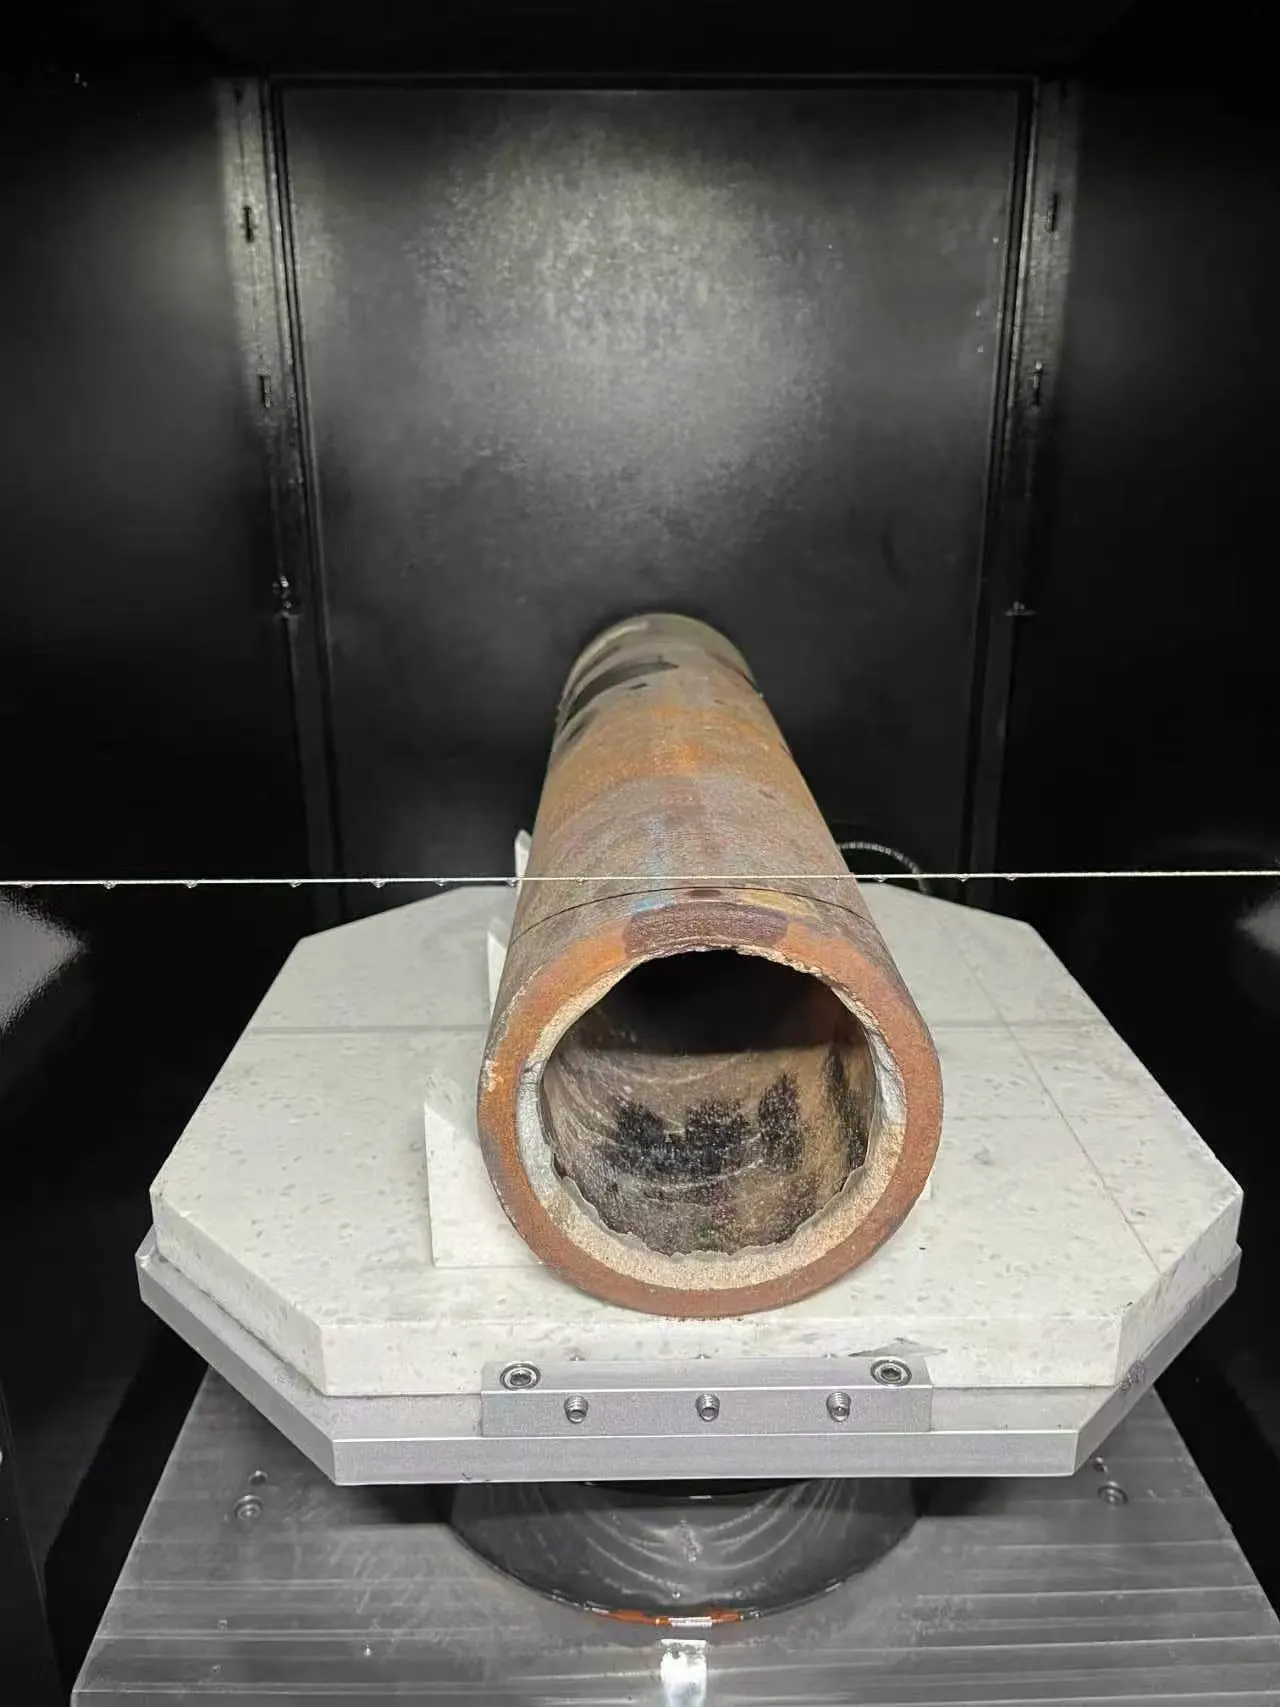
| Dimensions de la pièce | 500.0 mm (L) × Ø120.0 mm |
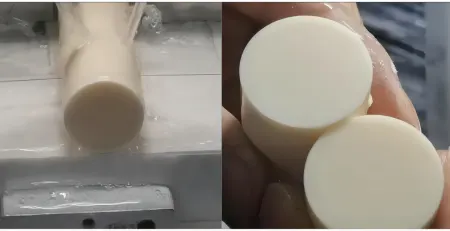
| Target slice dimensions | 10.0 mm (L) × Ø120.0 mm |
Ductile iron combines relatively high strength with a degree of toughness. Its structure consists of a metal matrix with spheroidal graphite nodules, and the difference in machinability between the matrix and the graphite phase can produce local variation in cutting behaviour along the kerf.
2. Sélection de l'équipement et du fil
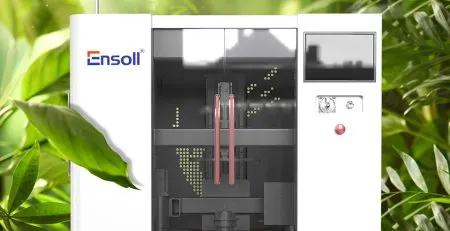
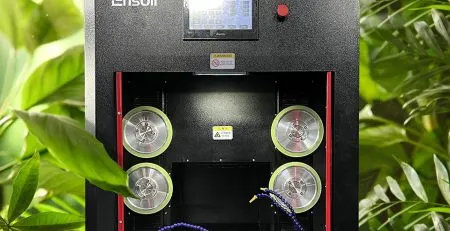
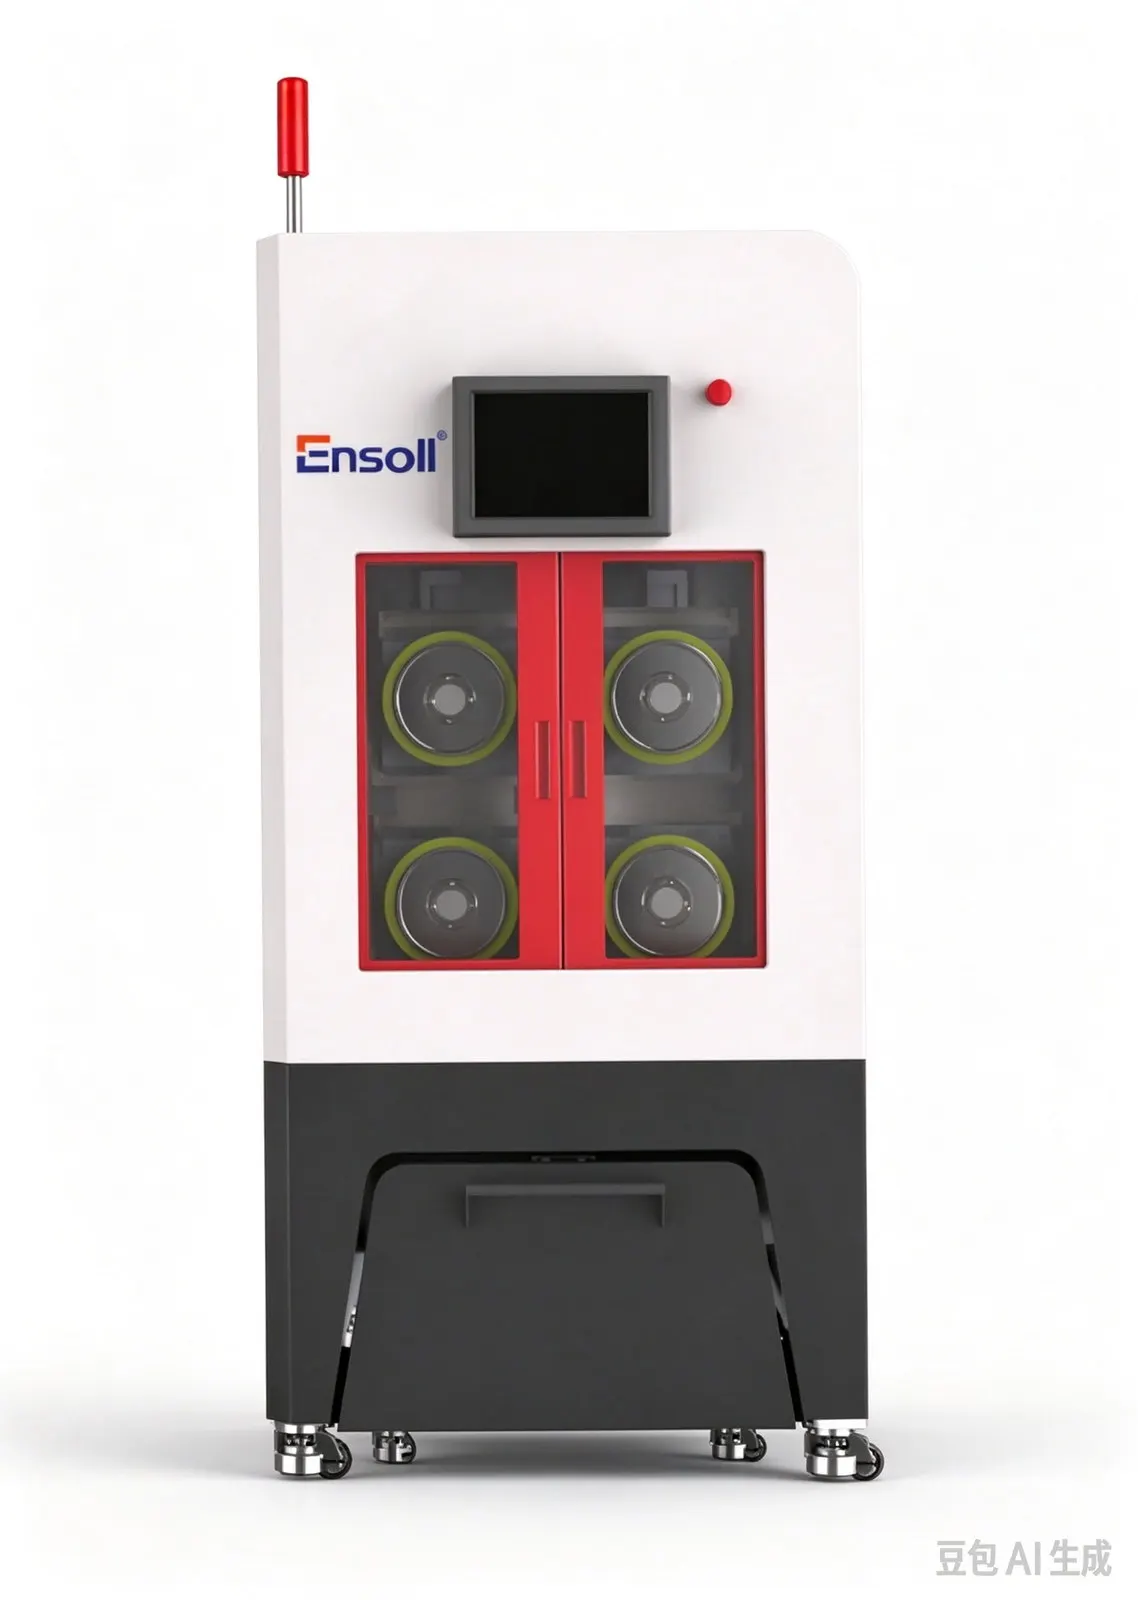
Équipement: ESG400-4T. In view of the characteristics of ductile iron and the requirement to slice at a 10 mm d'épaisseur, Ensoll selected the ESG400-4T ring diamond wire cutting system with a matched cutting feed. The machine maintains a stable wire trajectory and slice dimensional accuracy.
Liquide de refroidissement: coupe à l'huile. L'huile de coupe est utilisée comme milieu de refroidissement et de lubrification. It continuously lubricates and cools the contact zone between the diamond wire and the ductile iron and carries away part of the heat and cutting debris generated during cutting, reducing the effect of friction-heat accumulation and debris build-up on the machining condition. Controlled oil supply helps maintain a stable cutting zone.
Fil: totalement plaqué. un fil diamant totalement plaqué a été choisi, with the diamond abrasive grains bonded to the wire core by electroplating. The plated bond improves grain adhesion and distribution uniformity, so the wire maintains a consistent grinding capability and material removal behaviour during cutting. This reduces grain pull-out and wire wear, which matters for a metal workpiece of this section size.
3. Méthode de découpe et avantages de l'équipement
Configuration de découpe par portique. La structure du portique offre une grande rigidité globale et une stabilité de fonctionnement, which reduces the effect of machine vibration and structural deformation on the wire trajectory and keeps the cut stable. This limits the influence of changes in cutting load on slice position and dimensional accuracy in the ductile iron. La machine est équipée d'un système d'extraction de brouillard qui élimine rapidement le brouillard généré pendant la coupe.
Contrôle intelligent de la tension. Le système ajuste la tension du fil diamant en temps réel en fonction des conditions de coupe et prend en charge à la fois les modes à tension constante et à tension variable, maintenir le fonctionnement stable du fil. Well-matched tension control reduces fluctuation in the wire trajectory and limits localised uneven loading and the risk of wire breakage caused by tension variation, reducing the occurrence of slice defects.
Mémoire de rupture de fil. Si le fil diamanté se casse ou si la machine s'arrête de manière anormale, le système enregistre automatiquement la position actuelle d'usinage et l'état de fonctionnement associé. Après le remplacement du fil, la coupe reprend à partir de la position enregistrée, reducing dimensional deviation and material loss from re-positioning and repeat machining. This improves the continuity of ductile iron slicing.
Large workpiece capacity and high-speed cutting. The ESG400-4T provides a large effective working envelope, accommodating ductile iron workpieces of substantial section size. The ring diamond wire runs in continuous circulation, and wire speed can reach three to four times that of conventional wire-cut machines, which raises material removal efficiency while keeping the cut stable.
4. Paramètres du processus et méthode de refroidissement
| Paramètre | Valeur |
|---|---|
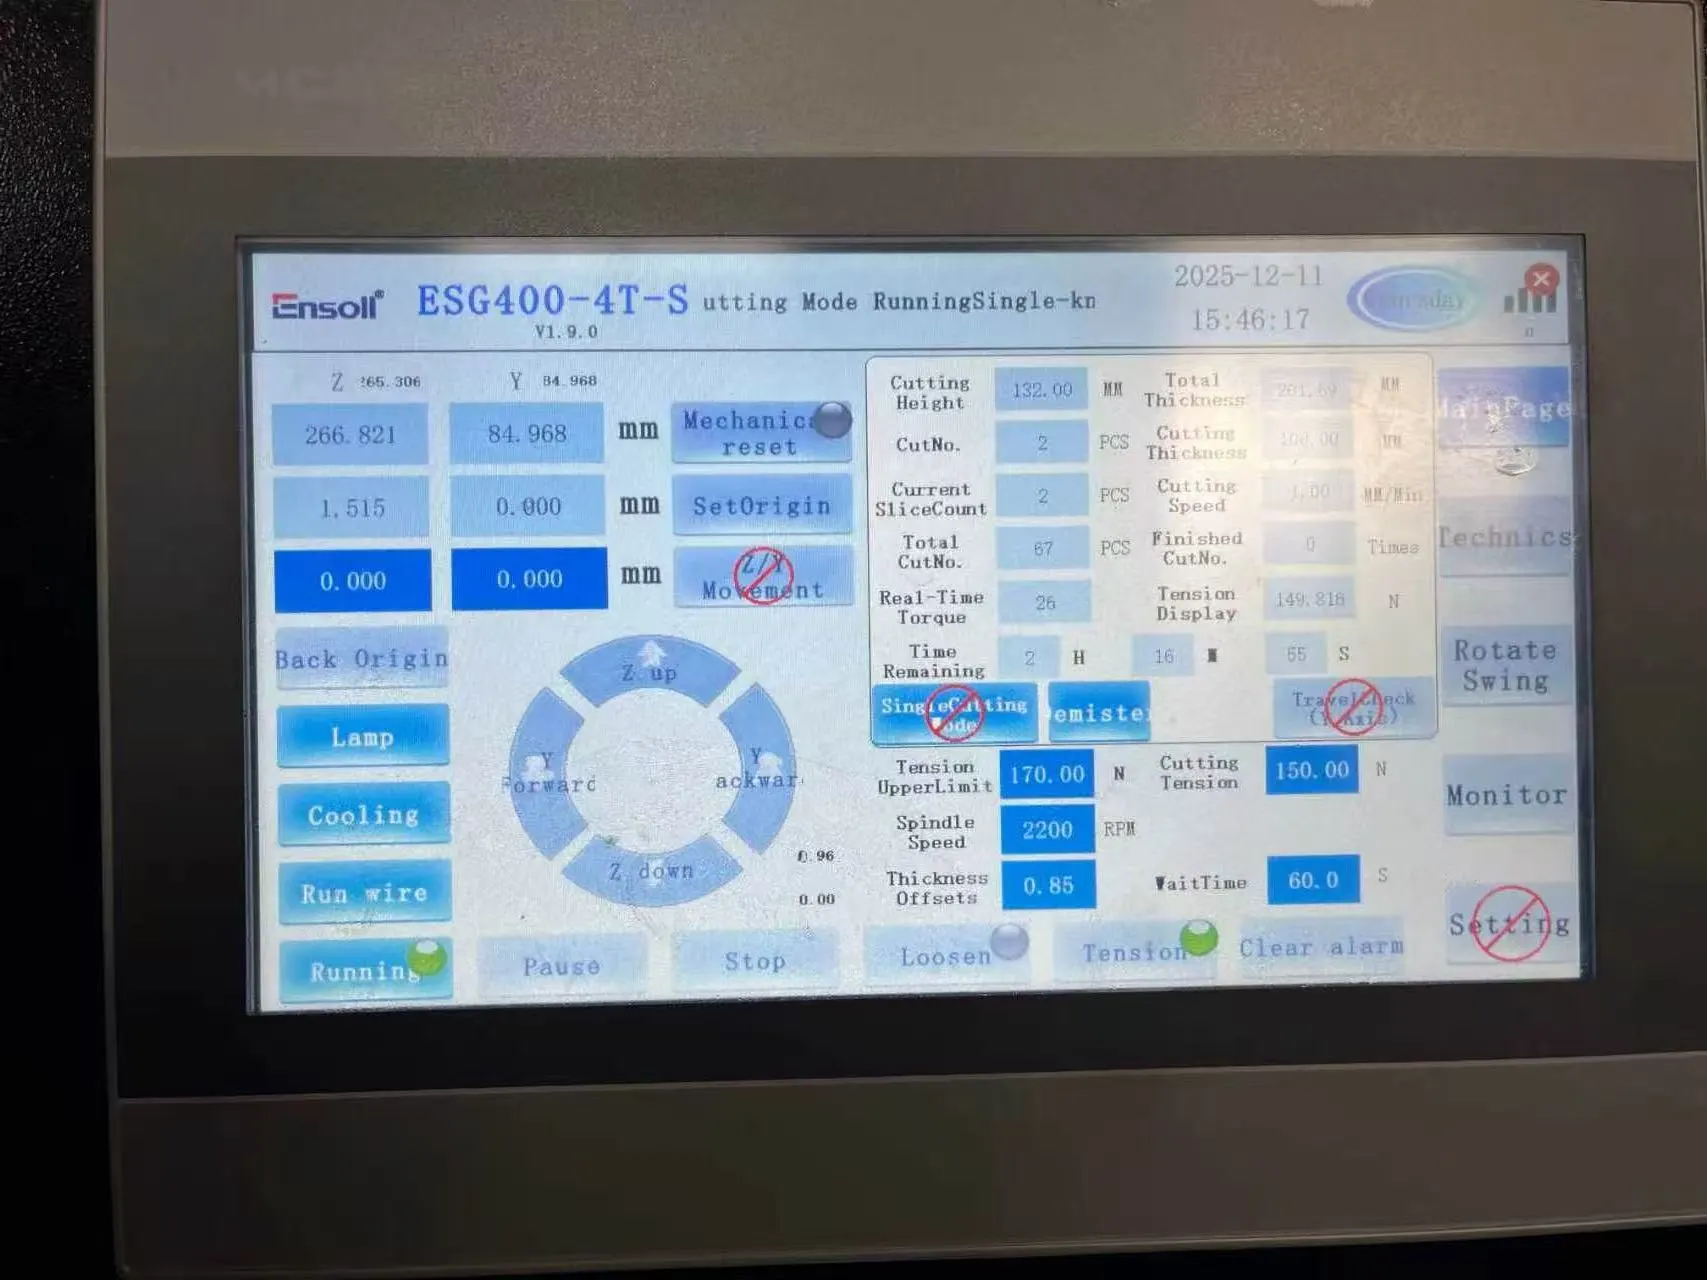
| Diamètre du fil (mm) | 0.80 × 2600 |
| Vitesse de déplacement du fil (mm/min) | 1.5 |
| Largeur de coupe (mm) | 120 |
| Tension du fil (N) | 150 |
| Vitesse du fil (m/s) | 32 |
| Temps de flexion du fil (s) | 60 |
5. Performance de coupe et résultats
5.1 Données de test TTV (Unité: mm)
Variation totale de l’épaisseur (TTV) a été mesuré à l'aide d'une grille à neuf points, Méthode de mesure d'épaisseur à double sonde sur une plate-forme à mandrin sous vide. The measurement was applied to ductile iron slices produced by ring diamond wire cutting. Avant la mesure, l'instrument a été thermiquement stabilisé et calibré par rapport à un bloc d'épaisseur standard. L'épaisseur nominale de la coupe était 10.000 mm.
| Échantillon | Lectures d'épaisseur en neuf points | Tmax | Tmin | TTV |
|---|---|---|---|---|
| S01 | 9.994, 9.997, 10.000 9.996, 10.001, 10.004 9.998, 10.005, 10.008 |
10.008 | 9.994 | 0.014 |
| S02 | 9.990, 9.994, 9.998 9.995, 10.000, 10.003 9.997, 10.004, 10.007 |
10.007 | 9.990 | 0.017 |
| S03 | 9.986, 9.991, 9.995 9.993, 9.998, 10.002 9.996, 10.003, 10.009 |
10.009 | 9.986 | 0.023 |
| S04 | 9.995, 9.998, 10.001 9.997, 10.002, 10.005 9.999, 10.006, 10.010 |
10.010 | 9.995 | 0.015 |
| S05 | 9.992, 9.996, 9.999 9.994, 10.000, 10.004 9.998, 10.005, 10.009 |
10.009 | 9.992 | 0.017 |
| S06 | 9.988, 9.993, 9.997 9.994, 9.999, 10.003 9.996, 10.004, 10.008 |
10.008 | 9.988 | 0.020 |
Évaluation. Nine-point grid measurement was applied to six ductile iron slices. Les valeurs de TTV étaient 0.014, 0.017, 0.023, 0.015, 0.017 et 0.020 mm, allant de 0,014 à 0,023 mm sur le lot, avec une TTV moyenne d'environ 0.018 mm on a 10.000 épaisseur nominale en mm. The results confirm good thickness uniformity when slicing a metal workpiece of this section size.
5.2 Données de tolérance d'épaisseur (Unité: mm)
La tolérance d'épaisseur a été dérivée à partir des données d'épaisseur à neuf points, en utilisant 10.000 mm comme épaisseur nominale. La déviation d'épaisseur positive et négative a été calculée à chaque position de mesure et les résultats des six échantillons ont été agrégés. La déviation positive maximale, la déviation négative maximale et la plage globale de déviation ont été déterminées pour évaluer la régularité d'épaisseur.
| Échantillon | Épaisseur moyenne | Déviation d'épaisseur |
|---|---|---|
| S01 | 10.000 | 0.000 |
| S02 | 9.999 | −0,001 |
| S03 | 9.997 | −0,003 |
| S04 | 10.001 | +0.001 |
| S05 | 10.000 | 0.000 |
| S06 | 9.998 | −0,002 |
| Écart positif maximal | — | +0.010 mm |
| Écart négatif maximal | — | −0,014 mm |
| Bande de tolérance d'épaisseur | — | ±0,012 mm |
Évaluation. Pour une épaisseur nominale de 10.000 mm, the six slices showed mean thicknesses of 9.997–10.001 mm, avec la moyenne du lot proche de la valeur nominale. Sur tous les points de mesure, la déviation d'épaisseur variait de −0,014 mm à +0.010 mm, avec une déviation absolue maximale de 0.014 mm.
5.3 Données de rugosité de surface Ra (Unité: μm)
Rugosité de surface (Ra) was measured by stylus profilometry on the ductile iron slices after ring diamond wire cutting. Des positions de mesure représentatives ont été prises au centre et sur les deux côtés le long de la face de coupe, Les données de profil de surface ont été acquises avec un profilomètre à stylet, et le paramètre de rugosité Ra a été enregistré à chaque position.
| Échantillon | Centre | Milieu-gauche | Milieu-droit | Ra moyen |
|---|---|---|---|---|
| S01 | 1.12 | 1.18 | 1.15 | 1.15 |
| S02 | 1.05 | 1.11 | 1.08 | 1.08 |
| S03 | 1.28 | 1.35 | 1.31 | 1.31 |
| S04 | 0.98 | 1.04 | 1.01 | 1.01 |
| S05 | 1.16 | 1.22 | 1.19 | 1.19 |
| S06 | 1.09 | 1.15 | 1.12 | 1.12 |
Évaluation. La moyenne Ra sur les six échantillons variait de 1.01 À 1.31 μm, avec toutes les lectures individuelles comprises entre 0.98 et 1.35 μm. The spread across measurement positions on each slice is modest, indicating a consistent surface finish along the cut face on a metal workpiece of this size.
5.4 Edge Condition Data (Unité: μm)
Edge defects were quantified by optical imaging on a toolmaker’s microscope. Les bords des échantillons ont été nettoyés avant la mesure et le grossissement ainsi que l'échelle de mesure de l'instrument ont été étalonnés. Le bord de la tranche a ensuite été examiné au microscope, identifiable edge defects were located and measured at four points per sample, et la valeur maximale a été retenue.
| Échantillon | Point 1 | Point 2 | Point 3 | Point 4 | Max. edge defect |
|---|---|---|---|---|---|
| S01 | 5.2 | 6.1 | 5.7 | 6.5 | 6.5 |
| S02 | 4.8 | 5.5 | 6.0 | 5.2 | 6.0 |
| S03 | 7.1 | 8.3 | 9.2 | 8.0 | 9.2 |
| S04 | 4.3 | 5.0 | 5.6 | 4.8 | 5.6 |
| S05 | 6.0 | 6.8 | 7.4 | 6.5 | 7.4 |
| S06 | 5.4 | 6.2 | 6.8 | 5.9 | 6.8 |
Évaluation. Toolmaker’s microscope inspection of the six ductile iron slices gave maximum edge defect values of 6.5, 6.0, 9.2, 5.6, 7.4 et 6.8 μm, avec un maximum global de 9.2 μm. S04 showed the best edge integrity and S03 the largest defect at 9.2 μm.
6. Conclusion
The good results obtained in this high-precision slicing trial of ductile iron stemmed mainly from the combined effect of a purpose-built cutting machine, la méthode de refroidissement et de lubrification, et des paramètres de processus correctement adaptés. Ductile iron has relatively high strength and a degree of toughness, and its structure consists of a metal matrix with spheroidal graphite. During ring diamond wire cutting, the difference between the matrix and the graphite phase can cause local variation in cutting behaviour, which places particular demands on machine rigidity and parameter matching.
Équipement. An ESG400-4T ring diamond wire cutting system was used. The machine provides a large effective working envelope for larger workpieces and a high-rigidity structure that reduces the effect of vibration and structural deformation on the wire trajectory. The ring diamond wire runs in continuous circulation at speeds well above conventional wire-cut machines, which raises removal efficiency without sacrificing cut stability.
Refroidissement et lubrification. Cutting oil was used as the cooling and lubricating medium. It continuously lubricates and cools the wire–workpiece contact zone, reduces friction at the cutting interface, and carries away part of the cutting heat and debris, improving conditions in the cutting zone. For a material with the strength and toughness of ductile iron, effective lubrication is essential to consistent surface finish.
Les paramètres du processus. Vitesse du fil, feed rate and other key parameters were matched to the properties of ductile iron and to the 10 mm slice requirement. Coordinating wire speed with workpiece feed keeps material removal steady and avoids localised increases in cutting load from excessive feed, or unstable cutting from mismatched parameters.
Dans l'ensemble. Pris ensemble avec la précision dimensionnelle des tranches, Rugosité (Ra) and edge quality, the combination of the ESG400-4T ring diamond wire machine, oil-based cooling and lubrication, and appropriately matched cutting parameters achieves a well-matched process for ductile iron. The results support ring diamond wire cutting as a practical route for precision slicing of ductile iron at this section size.