Fatiamento de Precisão de Material Magnético com Fio de Diamante: 2 Dados de Teste em mm
Sample testing for a European client (Company P) · Ring diamond wire cutting process
Visão geral
This report documents precision slicing of magnetic material using a ring diamond wire cutting system. The evaluation covers equipment and wire selection, cutting methodology, parâmetros do processo, and the resulting thickness uniformity, precisão dimensional, surface quality and edge integrity of the sliced parts. Test results indicate that a gantry-type ring diamond wire machine, oil-based cooling and lubrication, and appropriately matched process parameters deliver stable, high-precision slicing of magnetic material.
1. Test Specimen
| Parâmetro | Valor |
|---|---|
| Material | Magnetic material |
| Dureza | approx. 6–7 Mohs |
| Dimensões da peça de trabalho | 60 mm × 26.0 mm × 3.0 milímetro |
| Target slice dimensions | 2.0 mm × 26.0 mm × 3.0 milímetro |
2. Seleção de Equipamento e Fios
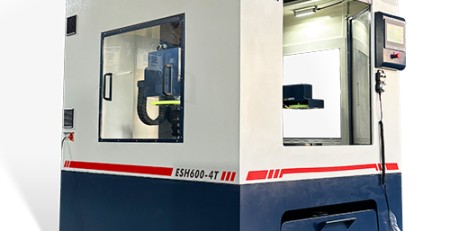
Equipamento: ESO-GM. In view of the hard-brittle characteristics of magnetic material and the requirement to slice at a 2 espessura em mm, Ensoll selected the ESO-GM gantry-type ring diamond wire cutting system with a top-down vertical feed. The gantry configuration maintains a stable wire trajectory and slice dimensional accuracy.
Fluido de arrefecimento: corte a óleo. O óleo de corte é utilizado como meio de arrefecimento e lubrificação. It improves lubrication and heat dissipation in the contact zone between the diamond wire and the magnetic material, reduces friction resistance and localised heat accumulation during cutting, and limits fluctuation in cutting load and its effect on the material. Isto ajuda a suprimir lascagem, micro-cracking and surface damage.
Fio: totalmente banhado. Foi selecionado um fio de diamante totalmente banhado. A construção com revestimento melhora a resistência de ligação entre os grãos de diamante abrasivo e o núcleo do fio e proporciona uma distribuição de grãos mais uniforme. Isto mantém uma taxa de remoção de material contínua e estável, reduz a extracção de grãos e o desgaste do fio, e contribui para menor lascamento, micro-cracking and surface damage when slicing magnetic material.

3. Método de Corte e Vantagens do Equipamento
Configuração de corte em pórtico. A estrutura em pórtico proporciona elevada rigidez geral e estabilidade de funcionamento. The top-down vertical feed helps keep the diamond wire trajectory stable and reduces the influence of changes in cutting force on kerf position and dimensional accuracy in the magnetic material. The machine is equipped with a mist-extraction system that promptly removes mist generated during cutting.
Controlo inteligente de tensão. O sistema ajusta a tensão do fio de diamante em tempo real, de acordo com as condições de corte, e suporta tanto modos de tensão constante como de tensão variável, mantendo o fio a funcionar de forma estável. Stable wire tension reduces fluctuation in the cutting trajectory and limits localised uneven loading and the risk of wire breakage caused by tension variation, which in turn reduces defects in the magnetic material.
Memória de quebra do fio. Se o fio de diamante se partir ou a máquina parar de forma anormal, O sistema regista automaticamente a posição de usinagem atual e o estado de funcionamento associado. Após a substituição do fio, cutting resumes from the recorded position, reducing dimensional deviation and material loss caused by re-positioning and repeat machining. This improves the continuity of magnetic material slicing and lowers the risk of repeated cutting.
Estrutura de ferro fundido de uma peça de alta rigidez. The one-piece cast iron frame provides high structural stiffness and vibration resistance, reducing the effect of machine vibration and structural deformation on the wire trajectory during machining. For a hard-brittle material such as magnetic material, the high-rigidity frame helps damp vibration and fluctuation in cutting force during the cut and keeps the diamond wire running stably.
4. Parâmetros de processo e método de arrefecimento
| Parâmetro | Valor |
|---|---|
| Diâmetro do fio (milímetro) | 0.35 × 1880 |
| Velocidade de travessia do fio (mm/min) | 2 |
| Largura de corte (milímetro) | 60 |
| Tensão do fio (N) | 140 |
| Velocidade do fio (M) | 26 |
| Tempo de curvatura do fio (s) | 60 |

5. Desempenho e resultados de corte

5.1 Dados de teste TTV (Unidade: milímetro)
Variação total da espessura (TTV) foi medido usando uma grelha de nove pontos, método de medição de espessura de duas sondas numa etapa de mandril a vácuo. The measurement was applied to magnetic material slices produced by ring diamond wire cutting. Before measurement the instrument was thermally stabilised and calibrated against a standard thickness block. A espessura nominal da fatia foi 2.000 milímetro.
| Amostra | Leituras de espessura de nove pontos | Tmáx | Tmín | TTV |
|---|---|---|---|---|
| S01 | 1.992, 1.996, 1.998 1.995, 2.000, 2.003 1.997, 2.004, 2.006 |
2.006 | 1.992 | 0.014 |
| S02 | 1.988, 1.993, 1.997 1.995, 2.001, 2.004 1.999, 2.006, 2.008 |
2.008 | 1.988 | 0.020 |
| S03 | 1.985, 1.990, 1.994 1.992, 1.998, 2.002 1.996, 2.004, 2.009 |
2.009 | 1.985 | 0.024 |
| S04 | 1.994, 1.997, 2.000 1.996, 2.001, 2.004 1.999, 2.005, 2.007 |
2.007 | 1.994 | 0.013 |
| S05 | 1.989, 1.994, 1.997 1.993, 1.999, 2.003 1.996, 2.005, 2.010 |
2.010 | 1.989 | 0.021 |
Avaliação. Nine-point grid measurement was applied to five magnetic material slices. TTV values were 0.014, 0.020, 0.024, 0.013 e 0.021 milímetro, spanning 0.013–0.024 mm across the batch, with a mean TTV of approximately 0.018 mm on a 2.000 mm de espessura nominal. The results confirm good thickness uniformity in magnetic material slicing.
5.2 Dados de Tolerância à Espessura (Unidade: milímetro)
Thickness tolerance was derived from the nine-point thickness data, using 2.000 mm conforme calculada a espessura nominal. The positive and negative thickness deviation were calculated at each measurement position and the results from all five samples were aggregated. O desvio máximo positivo, maximum negative deviation and overall deviation range were then determined to evaluate thickness consistency.
| Amostra | Espessura média | Desvio da espessura |
|---|---|---|
| S01 | 1.999 | −0.001 |
| S02 | 1.999 | −0.001 |
| S03 | 1.997 | −0.003 |
| S04 | 2.000 | 0.000 |
| S05 | 1.998 | −0.002 |
| Máxima deformação positiva | — | +0.010 milímetro |
| Máxima deformação negativa | — | −0.015 mm |
| Banda de tolerância de espessura | — | ±0.0125 mm |
Avaliação. Em relação a uma espessura nominal de 2.000 milímetro, the five slices showed mean thicknesses of 1.997–2.000 mm, with small average deviations across the batch. Over all measurement points the thickness deviation ranged from −0.015 mm to +0.010 milímetro, with a maximum absolute deviation of 0.015 milímetro.
5.3 Dados de Rugosidade de Superfície Ra (Unidade: μm)
Rugosidade da Superfície (Ra) was measured by stylus profilometry on the magnetic material slices after ring diamond wire cutting. Foram tomadas posições representativas no centro e em ambos os lados ao longo da face final do corte, os dados do perfil da superfície foram obtidos com um profilómetro de stylus, e o parâmetro de rugosidade Ra foi registado em cada posição.
| Amostra | Centre | Mid-left | Mid-right | Ra média |
|---|---|---|---|---|
| S01 | 0.52 | 0.56 | 0.49 | 0.52 |
| S02 | 0.48 | 0.53 | 0.50 | 0.50 |
| S03 | 0.61 | 0.66 | 0.58 | 0.62 |
| S04 | 0.46 | 0.51 | 0.48 | 0.48 |
| S05 | 0.55 | 0.59 | 0.53 | 0.56 |
Avaliação. Mean Ra across the five samples ranged from 0.48 Para 0.62 μm, com todas as medições individuais entre 0.46 e 0.66 μm. The narrow spread across the three measurement positions on each slice indicates a uniform surface finish along the cut face.
5.4 Dados de lascamento de borda (Unidade: μm)
A lascagem das arestas foi quantificada por imagem ótica no microscópio de um fabricante de ferramentas. Specimen edges were cleaned before measurement and the magnification and measurement scale of the instrument were calibrated. The slice edge was then inspected under the microscope, identifiable chipping defects were located and measured at four points per sample, and the maximum value was retained.
| Amostra | Point 1 | Point 2 | Point 3 | Point 4 | Max. lascar |
|---|---|---|---|---|---|
| S01 | 4.2 | 5.1 | 4.8 | 5.6 | 5.6 |
| S02 | 3.8 | 4.6 | 5.2 | 4.4 | 5.2 |
| S03 | 5.6 | 6.8 | 7.5 | 6.2 | 7.5 |
| S04 | 3.5 | 4.1 | 4.6 | 3.9 | 4.6 |
| S05 | 4.9 | 5.7 | 6.3 | 5.2 | 6.3 |
Avaliação. Toolmaker’s microscope inspection of the five magnetic material slices gave maximum chipping values of 5.6, 5.2, 7.5, 4.6 e 6.3 μm, with an overall maximum of 7.5 μm. S04 showed the best edge integrity and S03 the largest chipping at 7.5 μm.

6. Conclusão
The good results obtained in this high-precision slicing trial of magnetic material stemmed mainly from the combined effect of a purpose-built cutting machine, o método de arrefecimento e lubrificação, e parâmetros de processo corretamente ajustados. Magnetic material is relatively hard with a degree of brittleness. During ring diamond wire cutting the abrasive grains act continuously on the material surface, and material removal is affected by cutting load, wire running condition and the machining parameters.
Equipamento. An ESO-GM gantry-type ring diamond wire cutting system was used. The gantry structure provides high overall rigidity and running stability and gives reliable mechanical support for workpiece clamping and continuous wire travel. Stable motion and feed control keep the diamond wire on the programmed path throughout the cut.
Arrefecimento e lubrificação. Foi utilizado óleo de corte como meio de refrigeração e lubrificação. During cutting the diamond wire remains in continuous contact with the workpiece and the abrasive grains grind the material continuously, gerando calor por fricção na zona de contacto. Cutting oil improves lubrication at the cutting interface, carries away part of the cutting heat, and reduces friction between the wire and the workpiece, which helps limit thermal effects and edge damage.
Parâmetros do processo. Velocidade do fio, feed rate and other key parameters were matched to the hardness, brittleness and target slice thickness of the magnetic material. Os parâmetros foram definidos para manter um movimento estável do fio e remoção contínua de material, avoiding feed rates high enough to raise cutting load, or a mismatch between wire speed and feed rate that would degrade slice quality.
Geral. Taken together with slice dimensional accuracy, tolerância de espessura, rugosidade superficial (Ra) and cut-edge quality, the combination of the ESO-GM gantry cutting machine, oil-based cooling and lubrication, and appropriately matched process parameters allows ring diamond wire cutting to meet the precision slicing requirements for this magnetic material.