Cómo medir TTV en rebanadas finas: El método de nueve puntos
Abstracto: Total thickness variation (TTV) is the single number most often quoted for a
precision slicing process, and the easiest one to measure badly. This guide documents the nine-point grid
dual-probe method used in Ensoll’s slicing tests for
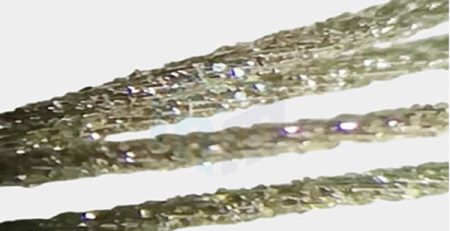
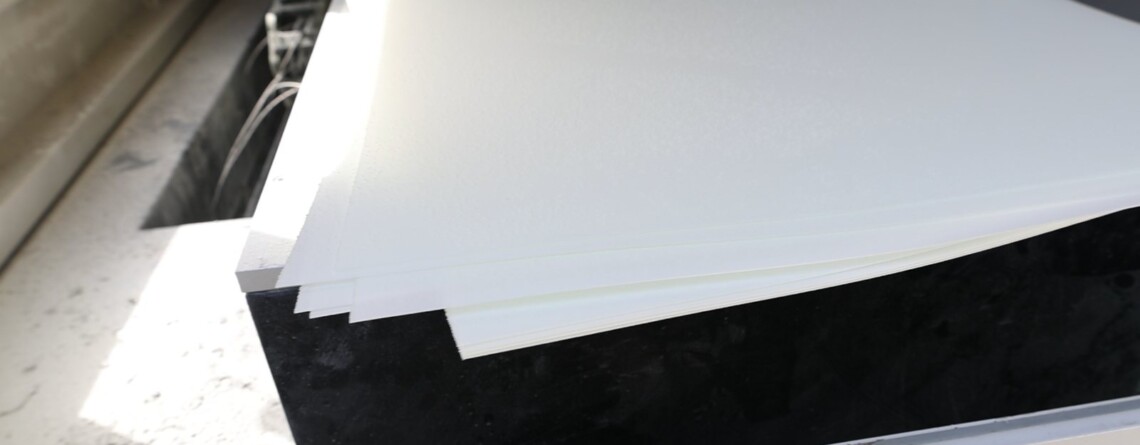
PEEK y PMI foam cut with a
bucle de alambre de diamante: how the sample is prepared, how it is held, where the nine points sit,
how TTV is calculated from them, and which errors produce a plausible but wrong number.
Puntos clave
- TTV = Tmax – Tmin across a defined set of measurement points on one part; it is a within-part spread, not a flatness measurement.
- The standard pattern is a nine-point 3×3 grid – the smallest layout that samples centre, edges and diagonals, and fast enough to run on every sample in a batch.
- The sample must be cleaned, thermally stabilised and held on a vacuum chuck; a loose thin slice measures its own warpage as thickness.
- Always report TTV together with the nominal thickness: 0.036 mm on a 0.8 mm PMI foam slice and 0.085 mm on a 6.5 mm PEEK slice are not comparable raw numbers.
- Batch-level TTV trends are process signals; single-sample outliers are usually sample-handling problems.
What TTV Is – and What It Is Not
Total thickness variation is the spread of thickness across a single part. Measure the thickness at each
point of a defined grid, take the largest reading and the smallest reading, and subtract: the difference is the
TTV of that part. It says nothing about where the thick and thin areas are, and nothing about how the part
deviates from a plane – which is why it is normally reported alongside the flatness-family parameters rather
que en lugar de ellos.
| Parámetro | Lo que describe | Referencia |
|---|---|---|
| TTV (variación total de espesor) | Diferencia entre el punto más grueso y el más delgado en una pieza | La propia cuadrícula de medición de la pieza |
| Desviación de espesor | Qué tan lejos está el espesor promedio del nominal | El nominal (objetivo) el espesor |
| Planitud | Desviación de una superficie respecto a un plano de referencia | Un plano ideal |
| Curvatura / deformación | Curvatura de la pieza en su conjunto | Un plano ideal, medida en toda la pieza |
| Conicidad | Cambio sistemático de espesor de un borde al otro | Los dos bordes opuestos |
El TTV se indica en la misma unidad que el espesor que se está midiendo. En trabajos de corte de precisión eso suele ser
micrómetros (µm) o milímetros (milímetros), y el espesor nominal siempre debe indicarse junto con él – un TTV de
0.036 mm significa algo muy diferente en un 0.8 mm de corte que en un 6.5 mm de corte.
El TTV es una disciplina de medición más que de mecanizado, but it only earns its keep when the process
around it is under control. The wire selection, cooling strategy and kerf questions that sit upstream of the
number are covered in the Preguntas frecuentes sobre tecnología de corte con lazo de alambre de diamante, and the range of
workpiece materials the method is applied to is summarised in the guide to
materiales adecuados para el corte con lazo de alambre de diamante.
Equipment Needed
- A thickness measuring instrument with two opposed probes, so the reading is the true part thickness rather
than a distance to a reference surface. - A vacuum chuck stage that holds the sample flat by negative pressure.
- A standard thickness block for calibration.
- A thermal stabilisation period – the instrument, the sample and the room should be at the same temperature
before measurement, to remove zero drift and systematic error. - A dust-free preparation area, so that particles on the sample surface do not enter the readings.
The Nine-Point Procedure
- Thermally stabilise and calibrate. Warm the instrument up at constant temperature and
calibrate it with the standard thickness block, to reduce zero drift and systematic error. - Clean the sample. Remove dust and loose debris from both faces. On a sliced foam or
composite, debris at the surface is a thickness error, not a cleanliness issue. - Mount on the vacuum chuck. Centre the sample and hold it by negative pressure. This keeps
the sample in a stable measuring state and limits the effect of position shift, local warping and deformation
on the readings. - Define the grid. Mark nine positions in a 3×3 pattern – three rows of three, spanning the
centre and the edge regions of the part. Se debe usar la misma cuadrícula para cada muestra del lote. - Recolectar lecturas en secuencia. Medir las nueve posiciones en el mismo orden en cada
muestra, para que cualquier desviación del instrumento se distribuya de manera idéntica en lugar de afectar a una sola muestra. - Tomar Tmax y Tmin y restar. TTV = Tmax – Tmin para esa muestra. El resultado describe
esa parte; La consistencia del lote se juzga comparando TTV entre las muestras.
Ejemplo trabajando
Del test de corte de espuma PMI, la muestra S01 dio nueve lecturas de 0.785, 0.790, 0.799 / 0.800, 0.802, 0.812
/ 0.819, 0.832, 0.835 milímetros. Tmax es 0.835 mm y Tmin es 0.785 milímetros, así que:
TTV = 0.835 – 0.785 = 0.050 milímetros
La misma muestra medida para tolerancia dimensional promedió 0.808 mm frente a un 0.800 mm de grosor nominal,
una desviación de +0.008 milímetros. Esos dos números responden a diferentes preguntas: la desviación indica que la rebanada está cerca del
grosor objetivo, mientras que el TTV indica cuánto varía a lo largo de su propia área. Un proceso puede mantener el grosor
well and still have poor TTV.
Reference TTV Values from Diamond Wire Cutting
| Material | Slice produced | TTV | Thickness tolerance | Ra | Máximo astillado |
|---|---|---|---|---|---|
| PMI foam | 400 x 400 x 0.8 milímetros | 0.013-0.050 milímetros, mean 0.036 milímetros | +/-0.043 milímetros | 0.68-0.82 µm | 7.1 µm |
| PEEK | 6.5 x 60 x 60 milímetros | 0.072-0.098 milímetros, mean 0.085 milímetros | +/-0.037 milímetros | 0.76-0.95 µm | 6.7 µm |
Three Ways to Get a Wrong Number
Measuring a sample that is not held flat
A thin slice laid loose on a surface measures its own warpage as well as its thickness. The vacuum chuck
exists to remove that variable; skipping it typically inflates TTV on thin parts rather than reducing it.
Comparing TTV across nominal thicknesses
A raw TTV value is only meaningful against the nominal thickness and the application tolerance. The PMI
foam figure of 0.036 mm average sounds tighter than the PEEK figure of 0.085 mm average, but the slices were
0.8 mm and 6.5 mm thick respectively. Report the nominal thickness with every TTV value or the comparison is
misleading.
Reading TTV as a flatness measurement
TTV no te dice si la pieza está arqueada o deformada, y un TTV bajo no garantiza una pieza plana.
Donde la planicidad importa, mídela por separado, en la misma muestra, con el plano de referencia adecuado
método.
Uso del TTV en el Control de Procesos
Debido a que el método de nueve puntos es rápido y repetible, su valor real es comparativo: úsalo en cada muestra
en un lote y el patrón de resultados indica si el proceso es estable. Una sola muestra con un TTV alto
indica esa muestra; un lote que tiende a subir indica el proceso – más a menudo la condición del alambre, tensión
estabilidad o soporte del accesorio. En la prueba de espuma PMI las cuatro muestras dieron TTV de 0.050, 0.037, 0.044 y
0.013 milímetros, con el valor más bajo en la última muestra, indicando consistencia en el grosor de la rebanada con cierta
variación de muestra a muestra en lugar de una tendencia sistemática.
Preguntas Frecuentes
What does TTV mean in precision cutting?
TTV stands for total thickness variation. It is the difference between the thickest and the thinnest reading across a defined set of measurement points on one part. On a sliced wafer, plate or foam sheet it is the headline indicator of how uniform the cut was, and it is expressed in the same unit as the thickness – micrometres or millimetres.
How is TTV different from flatness, bow and warp?
TTV describes the spread of thickness values on one part. Planitud, bow and warp describe how the part deviates from a reference plane – a part can be uniformly thin and still be bowed. A slicing process can therefore show good TTV and poor flatness at the same time, which is why both are reported separately.
Why use nine points rather than more or fewer?
A nine-point 3×3 la cuadrícula es el patrón más pequeño que muestrea el centro, los bordes y las direcciones diagonales, para detectar un gradiente de grosor a través del corte en lugar de solo una dispersión aleatoria. también es lo suficientemente rápido para aplicar en cada muestra en un lote, lo que hace resultados comparables entre muestras y materiales.
¿Por qué debe sostenerse la muestra sobre un mandril de vacío??
Una franja fina es flexible. Si simplemente se coloca sobre una superficie, su propio peso y cualquier deformación local cambian la lectura. mantenerla con presión negativa sobre un mandril de vacío lo mantiene en un estado de medición repetible y limita el efecto del desplazamiento de posición, deformación y deformación local en las lecturas de grosor.
¿Qué valores TTV ha logrado el corte de alambre de diamante??
Sobre 0.8 mm en rebanadas de espuma PMI de mm, TTV varió desde 0.013 El papel del interruptor magnético del refrigerador. 0.050 mm con un promedio de 0.036 milímetros. Sobre 6.5 mm de cortes PEEK, TTV varió desde 0.072 El papel del interruptor magnético del refrigerador. 0.098 mm con un promedio de 0.085 milímetros. Porque las piezas difieren en grosor nominal y material, comparar cada una con su tolerancia de aplicación.
Contenido técnico revisado por el equipo de ingeniería de Ensoll – un fabricante de lazos de alambre de diamante con 10+ años de experiencia en producción.