PEEK対PMIフォーム: ダイヤモンドワイヤー切断比較
要約: PEEK and PMI foam sit at opposite ends of the material spectrum that a
ダイヤモンドワイヤーループ has to handle – one is a dense, tough thermoplastic, the other a
low-density cellular structural foam. This comparison sets Ensoll’s two published slicing tests side by side:
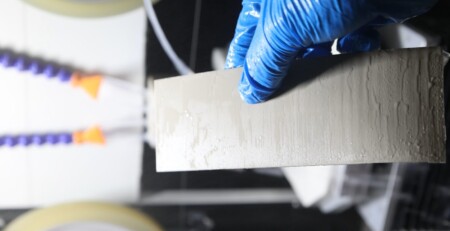
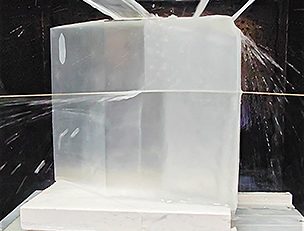
a 200 mm x 60 mm x 60 mm PEEK block cut into 6.5 mm slices with cutting fluid, and four 400 mm x 400 mm PMI
foam slices cut to 0.8 mm dry. It compares the failure modes, the parameter sets
(a diamond wire saw machine in both cases) and the measured quality results, and gives the
rule for deciding which starting point to use.
重要なポイント
- PEEK is limited by cutting heat (it is a thermoplastic that softens at the kerf); PMI foam is limited by cutting load (its cell skeleton compresses and tears).
- PEEK was cut wet at a 3 mm/min feed; PMI foam was cut dry at 100 ミリメートル/分 – a two-order-of-magnitude difference in feed rate for essentially the same wire speed.
- PEEK: TTV 0.072-0.098 ミリメートル (mean 0.085 ミリメートル), tolerance +/-0.037 ミリメートル, Ra 0.76-0.95 um, chipping max 6.7 um, on 6.5 mm slices.
- PMI foam: TTV 0.013-0.050 ミリメートル (mean 0.036 ミリメートル), tolerance +/-0.043 ミリメートル, Ra 0.68-0.82 um, chipping max 7.1 um, on 0.8 mm slices.
- The two parameter sets are not interchangeable – wire diameter, tension, feed rate and cooling method all differ.
Two Materials, Two Different Failure Modes
The reason PEEK and PMI foam need different process settings is not hardness alone – it is what happens when
the process window is exceeded.
PEEK is a high-performance thermoplastic with high toughness, wear resistance and heat resistance. Under
diamond wire cutting its removal mechanism differs from hard and brittle materials: because the material has
plasticity and toughness, the continuous action of the abrasive grains generates cutting heat. If that heat
cannot dissipate, the machining zone softens locally and cutting resistance rises, producing dimensional
deviation, edge burrs and degraded surface quality. The controlling variable is therefore
temperature.
PMI foam is a high-performance structural foam with low density, a uniform cellular structure and good
specific strength and stiffness. Its porous interior gives a removal behaviour quite unlike a dense material:
the abrasive grains act on the foam skeleton, and if the cutting load is too high or the parameters are poorly
matched, the cells are compressed and torn and the cut face becomes uneven, which feeds directly into slice
thickness and surface quality. The controlling variable is therefore load.
Material and Workpiece Comparison
| Item | PEEK | PMI foam |
|---|---|---|
| Material class | High-performance thermoplastic | High-performance structural foam |
| Hardness | Approximately MH 6.5 | Approximately MH 2 |
| Workpiece size | 200 mm x 60 mm x 60 ミリメートル | 400 mm x 400 mm x 50 ミリメートル |
| Slice produced | 6.5 mm x 60 mm x 60 ミリメートル | 400 mm x 400 mm x 0.8 ミリメートル |
| Density | Dense, solid | 低密度, cellular |
| Governing failure mode | Cutting heat – local softening, burrs | Cutting load – cell compression and tearing |
| 冷却 | Cutting fluid (continuous) | Dry cutting |
Parameter Comparison
| Parameter | PEEK | PMI foam |
|---|---|---|
| Machine | ESO-GM gantry-type | ESH600-4T horizontal |
| Wire diameter x loop length (ミリメートル) | 0.35 x 1880 | 0.60 x 3460 |
| Wire type | Fully coated | Fully coated |
| Feed rate (ミリメートル/分) | 3 | 100 |
| Cutting width (ミリメートル) | 2 | 400 |
| Wire tension (N) | 150 | 145 |
| Wire speed (MS) | 24 | 25 |
| Wire-bow tensioning time (s) | 60 | 60 |
| Cutting load (N·m) | 17 | 17 |
Result Comparison
| Measure | PEEK (6.5 mm slices) | PMI foam (0.8 mm slices) |
|---|---|---|
| 全厚さ変動 (TTV) | 0.072-0.098 ミリメートル, mean 0.085 ミリメートル | 0.013-0.050 ミリメートル, mean 0.036 ミリメートル |
| Thickness tolerance | +/-0.037 mm against 6.500 mm nominal | +/-0.043 mm against 0.800 mm nominal |
| Average surface roughness Ra | 0.76-0.95 um (means 0.80-0.91 um) | 0.68-0.82 um |
| Maximum edge chipping | 6.7 um (range 4.2-6.7 um) | 7.1 um (range 5.5-7.1 um) |
| Sample count | 3 slices | 4 slices |
Reading the Differences: Three Rules
Rule 1 – Temperature-dominated materials get cooling; load-dominated materials do not
PEEK was cut with cutting fluid as the cooling medium to improve heat dissipation and lubrication at the wire
interface, limiting local softening, deformation and burrs. PMI foam was cut dry so that no liquid entered the
cells and no cleaning or drying step was needed afterwards. Choosing the wrong one is a process error in both
directions: dry-cutting PEEK risks a softened kerf, and wet-cutting PMI foam risks dimensional drift from
absorbed liquid.
Rule 2 – The soft material can run two orders of magnitude faster in feed
The PEEK feed rate was 3 ミリメートル/分; the PMI foam feed rate was 100 ミリメートル/分. That gap is not a machine difference,
it is the consequence of what limits the process. PEEK removal is limited by how much heat can be carried away,
so feed must stay low. PMI foam removal is limited by how much load the cell skeleton can take, and because the
foam is low density that ceiling is reached much later. Both tests used similar wire speed – 24 m/s for PEEK and
25 m/s for PMI foam – which confirms that feed rate, not wire speed, is the discriminating parameter.
Rule 3 – Compare each material against its own tolerance, not against the other
PMI foam produced TTV of 0.013-0.050 mm against PEEK’s 0.072-0.098 ミリメートル, but the slices were 0.8 mm and 6.5 ミリメートル
thick respectively and the tolerance requirement differs with the application. What both tests do show is a
stable process: PEEK held +/-0.037 mm thickness tolerance and PMI foam +/-0.043 ミリメートル, with Ra below 1 um in both
cases and edge chipping under 7.1 um in both cases.
Which Starting Point to Use
| If the material is… | Start from | First lever |
|---|---|---|
| A dense thermoplastic that softens with heat (PEEK, and similar engineering plastics) | ESO-GM style gantry machine, 0.35 mm fully coated wire, 24 MS, 3 ミリメートル/分, 150 N, cutting fluid | Feed rate – keep heat generation low |
| A low-density cellular foam (PMI and similar structural foams) | ESH600-4T horizontal machine, 0.60 mm fully coated wire, 25 MS, 100 ミリメートル/分, 145 N, 乾いた | Feed rate – keep load off the cell skeleton |
| Hard and brittle (珪素, 炭化ケイ素, 陶芸, 光学ガラス) | See the material-specific guides for the cluster | Wire specification and kerf control |
Common Mistakes When Switching Between the Two
- Carrying the feed rate across. A feed that is conservative for PMI foam is far too
aggressive for PEEK, and a feed that is right for PEEK leaves the PMI cut polishing rather than cutting. - Assuming coolant helps everywhere. On PMI foam, coolant is a dimensional risk rather than a
safety margin. - Judging the foam result by the plastic result. NS 0.8 mm foam slice and a 6.5 mm plastic
slice cannot be compared on raw TTV numbers. - Chasing wire speed. In both tests the wire speed sat in the same 24-25 m/s band, which is
the clearest sign that it is not the lever for quality on either material. - Ignoring the entry edge. Both materials need the wire bow to settle before feed engages; a
60 s wire-bow tensioning time was used in both tests.
Full Test Data
The complete measurement sets – nine-point thickness readings, tolerance tables, Ra profiles and chipping
measurements – are published in the two source reports:
PEEK precision slicing with diamond wire loop and PMI foam precision slicing with
ダイヤモンドワイヤーループ. The measurement method itself is described in the
nine-point TTV measurement guide.
よくある質問
Is PEEK or PMI foam harder to cut with a diamond wire loop?
They are hard in different ways. PEEK is a dense, tough thermoplastic: the risk is cutting heat, which softens the material at the kerf and produces dimensional deviation and burrs. PMI foam is a low-density cellular solid: the risk is cutting load, which compresses and tears the cell skeleton. PEEK therefore needs cooling and conservative feed, while PMI foam needs load control and dry cutting.
Why is PEEK cut wet and PMI foam cut dry?
PEEK is a thermoplastic that softens when the cutting zone heats up, so cutting fluid is used to remove heat and lubricate the wire-material interface. PMI foam is porous and absorbs liquids, so coolant would enter the cells and would then have to be removed by cleaning and drying – so dry cutting is used instead.
How different are the feed rates between the two materials?
Substantially. PEEK was sliced at a 3 mm/min feed rate, while PMI foam ran at 100 ミリメートル/分. The dense thermoplastic needs slow feed to keep heat generation low; the low-density foam tolerates a much higher feed because removal is limited by load, not by heat. Wire speed was similar in both tests, 24 m/s for PEEK and 25 m/s for PMI foam.
Which material achieved better dimensional results?
PMI foam showed the smaller variation in absolute terms – TTV 0.013-0.050 ミリメートル (average 0.036 ミリメートル) against PEEK’s 0.072-0.098 ミリメートル (average 0.085 ミリメートル) – but the two are not directly comparable. The PEEK slices were 6.5 mm thick and the PMI slices 0.8 ミリメートル, and a thinner slice is measured against a much smaller nominal thickness. Compare each material against its own application tolerance.
Can one parameter set be used for both materials?
いいえ. The validated sets differ in wire diameter, feed rate, tension and cooling method. PEEK used a 0.35 x 1880 mm fully coated wire at 150 N tension with cutting fluid; PMI foam used a 0.60 x 3460 mm fully coated wire at 145 N tension with dry cutting. Start each material from its own validated window in the PMI foam cutting parameter reference.
Technical content reviewed by the Ensoll engineering team – a diamond wire loop manufacturer with 10+ years of production experience.