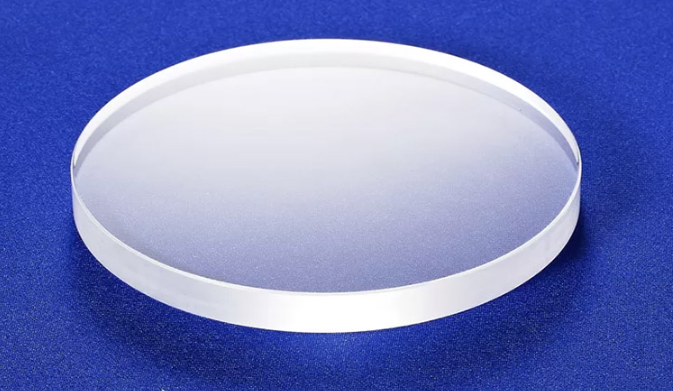
In the precision-driven world of optical manufacturing, the quality of crystal cutting directly impacts the performance of end products. From laser systems to advanced imaging devices, optical crystals like sapphire, lithium niobate, and calcium fluoride form the foundation of modern photonic technologies. Traditional cutting methods often compromise material integrity, leading to reduced optical performance and increased production costs.
Laço de fio diamantadocutting has emerged as the gold standard for optical crystal processing, offering manufacturers unprecedented control over the cutting process. This advanced technology combines the precision of diamond abrasives with the flexibility of wire-based cutting to deliver exceptional results. Unlike conventional sawing methods, diamond wire loops produce cleaner edges, minimize material waste, and preserve the intrinsic properties of optical crystals.
The transition to diamond wire technology represents more than just an equipment upgrade – it’s a fundamental shift in how optical components are manufactured. By understanding and implementing best practices in diamond wire cutting, manufacturers can achieve superior product quality while optimizing production efficiency.
Crystal behaves like its glass counterpart under the wire, so the guidance oncorte óptico de vidroapplies here too.
Section 1: Fundamental Advantages of Diamond Wire Cutting
1.1 Unmatched Material Preservation
The slender profile of diamond wire loops creates significantly narrower kerf widths compared to traditional blades. This characteristic proves particularly valuable when working with expensive optical-grade crystals, where every micron of conserved material translates to cost savings. A typical diamond wire produces kerfs measuring just 100-200 micrómetros, allowing for more efficient material utilization and increased yield from each crystal boule.
1.2 Superior Surface Integrity
Optical applications demand flawless surfaces free from micro-fractures and subsurface damage. Diamond wire cutting excels in this regard by:
– Distributing cutting forces evenly across the wire length
– Minimizing localized stress concentrations
– Producing surface roughness values often below 1μm Ra
– Eliminating the need for aggressive post-processing
1.3 Thermal Management Benefits
The continuous motion of diamond wire loops prevents heat buildup in any single area of the workpiece. This thermal stability is crucial for maintaining the optical properties of temperature-sensitive crystals. Unlike pulsed cutting methods that create thermal cycling, diamond wire maintains a consistent temperature profile throughout the process, preventing alterations to crystal structure and refractive properties.
Section 2: Technology and Methodology
2.1 Composição do Fio de Diamante
Modern diamond wires for optical crystal cutting feature sophisticated designs optimized for specific materials:
– Core Wire: High-tensile steel or tungsten for durability
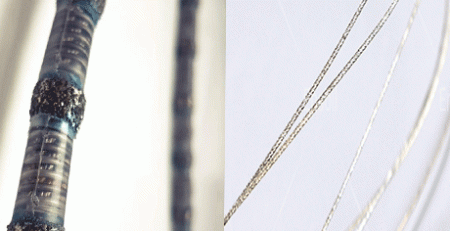
– Granulado de Diamante: Precisely sized synthetic diamonds (10-50μm)
– Bonding Matrix: Nickel-based or resin coatings for particle retention
– Surface Treatments: Special coatings to enhance performance
2.2 Cutting System Architecture
Advanced diamond wire cutting systems incorporate multiple precision components:
– Wire Guidance System: Precision rollers and tensioners
– Motion Control: Multi-axis positioning with sub-micron accuracy
– Coolant Delivery: High-pressure, filtered fluid systems
– Process Monitoring: Real-time sensors for quality assurance
2.3 Operational Workflow
A standardized cutting procedure ensures consistent results:
Material preparation and fixturing
Wire threading and tensioning
Parameter input and system calibration
Automated cutting cycle initiation
Post-cut inspection and quality verification
Section 3: Application-Specific Solutions
3.1 Sapphire Optics Production
Sapphire’s exceptional hardness (Mohs 9) makes it particularly suited for diamond wire cutting:
– Recommended wire diameter: 0.15-0.20milímetro
– Optimal diamond size: 15-25μm
– Cutting speed range: 0.5-1.5mm/min
– Preferred coolant: Deionized water with anti-corrosion additives
3.2 Lithium Niobate Component Manufacturing
The ferroelectric properties of LiNbO₃ require specialized approaches:
– Lower tension settings to prevent domain disruption
– Alcohol-based coolants to prevent hydration
– Slower cutting speeds for stress minimization
– Post-cut annealing recommendations
3.3 Calcium Fluoride Window Fabrication
CaF₂’s softness and brittleness demand careful handling:
– Smaller diamond particles (10-15μm) for clean cuts
– Reduced feed rates to prevent edge chipping
– Temperature-controlled environments
– Specialized wire coatings to prevent chemical interaction
Section 4: Process Optimization Strategies
4.1 Parameter Optimization
Key variables requiring precise adjustment:
– Tensão do Fio: Typically 20-40N depending on material
– Velocidade de corte: Material-specific velocity profiles
– Coolant Flow Rate: 5-15 liters/minute based on cut geometry
– Taxa de Avanço: Optimized for material properties and thickness
4.2 Quality Control Measures
Implementing comprehensive quality assurance:
– Pre-cut material inspection (crystallographic orientation verification)
– Surface Irregularities: Identification and correction
– Dimensional Variability: Process adjustment strategies
– Reduced Wire Life: Maintenance and parameter optimization
Section 5: Implementation and ROI Considerations
5.1 System Selection Criteria
Evaluating diamond wire cutting equipment:
– Production volume requirements
– Material diversity needs
– Facility space constraints
– Automation integration capabilities
– Service and support availability
5.2 Análise Custo-Benefício
Understanding the financial implications:
– Capital investment vs. operational savings
– Material yield improvements
– Labor efficiency gains
– Quality enhancement benefits
– Maintenance cost considerations
5.3 Transition Planning
Steps for successful implementation:
– Pilot testing and process development
– Operator training programs
– Production workflow integration
– Quality standard establishment
– Performance benchmarking
Conclusão: The Future of Optical Crystal Processing
Laço de fio diamantadocutting technology represents a transformative advancement for optical crystal manufacturing. As the demand for high-performance optical components grows across industries, manufacturers who adopt this technology position themselves at the forefront of precision manufacturing.
The benefits extend beyond immediate quality improvements – diamond wire cutting enables new possibilities in optical design by allowing more complex geometries and thinner components than previously achievable. As the technology continues to evolve with smarter controls and advanced wire formulations, its role in optical manufacturing will only expand.
For companies seeking to enhance their optical crystal processing capabilities, investing in high-qualityLoop de fio de diamantecutting systems offers a clear path to improved product quality, reduced manufacturing costs, and greater production flexibility. The transition requires careful planning and process optimization, but the long-term advantages make it an essential strategic move for forward-thinking manufacturers.
Principais Conclusões
Os tijolos normalmente classificam 5-8 na escala de dureza de Mohs, portanto, ferramentas de corte e moagem precisam de abrasivos mais duros e mais.... leia mais
No mundo do processamento de pedras preciosas e materiais duros, a precisão não é apenas um luxo – é uma necessidade absoluta. Durante séculos,... leia mais
Principais Conclusões
Cobalto de samário (SmCo) magnets combine high magnetic strength with thermal stability up to 350 degC e resistência à corrosão natural... leia mais
Introduction
Hard and brittle materials are essential in industries like electronics, óptica, aeroespaço, e dispositivos médicos. Contudo, cortando-os frequentemente... leia mais
Conclusões Chave
O vidro ótico é projetado para objetivas, prismas e filtros com índice de refração precisamente controlado, dispersão e baixos níveis de impureza.... leia mais
Principais Conclusões
PV Os fabricantes de PV precisam de mais pastilhas por lingote a um custo cada vez menor — exatamente o que a serra em laço de arame de diamante proporciona.
Estreito... leia mais
Conclusões Chave
Corte de materiais duros e frágeis sofre de baixa eficiência, baixo rendimento material, má qualidade de superfície, alto custo da ferramenta e poluição; espesso... leia mais
As serras de cabo de metal são ferramentas versáteis amplamente utilizadas para cortar vários tipos de metais. Eles são comumente empregados em indústrias... leia mais
Abstrair: Esta ficha de referência lista a janela de processo validada no teste de corte de espuma estrutural PMI da Ensoll
(polimetacrilimida) em uma máquina horizontal ESH600-4T
leia mais