Ferrite (セラミック) 磁石は酸化鉄にストロンチウムまたはバリウム炭酸塩を混ぜて焼結したものです: 安価, 耐食性があり、安定している 250 degC, but hard and brittle — so cutting method directly decides yield.
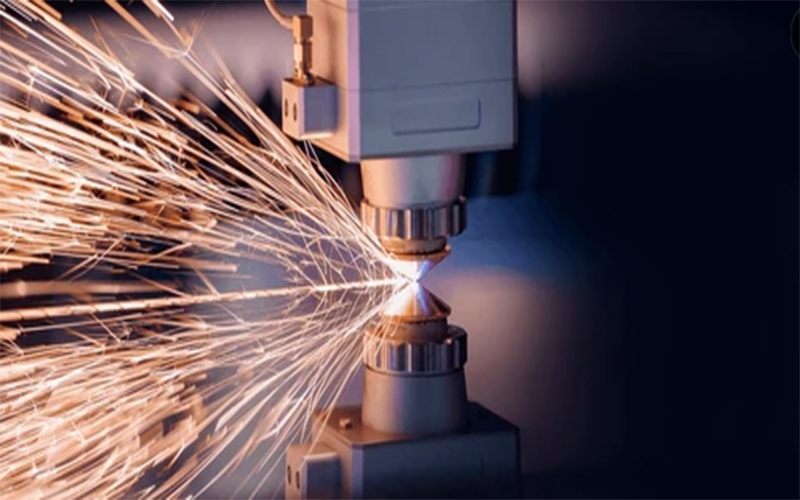
Grinding leaves 50-100 micrometer micro-cracks and runs slowly; laser adds a heat-affected zone that alters magnetic properties; waterjet leaves Ra >3 micrometer edges needing polishing.
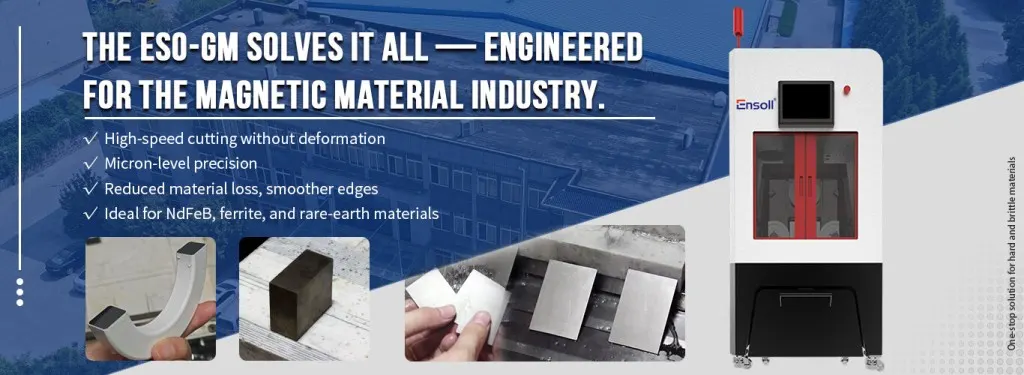
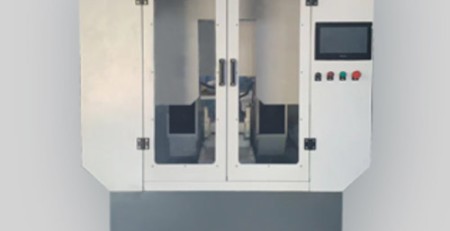
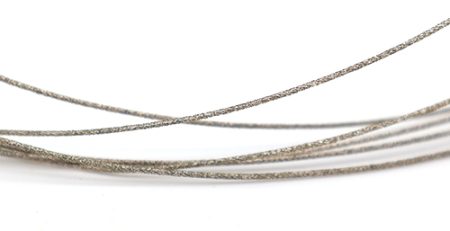
Diamond wire saw cutting is the best fit: a 0.1-0.3 mm diamond-coated wire gives chip-free edges (Ra <0.5 micrometers), no heat damage, ±0.02 mm tolerances and kerf under 0.2 ミリメートル.
About 80% of Japanese ferrite manufacturers already use diamond wire saws, cutting production cost by roughly 30% versus grinding in high-volume runs.
1. What Are Ferrite Magnets?
Ferrite magnets, also known as ceramic magnets, are a type of permanent magnet composed primarily of iron oxide (Fe₂O₃) combined with strontium or barium carbonate. They are sintered under high temperatures to form a hard, brittle ceramic material with moderate magnetic strength (0.2–0.4 Tesla).
Key Properties
– Cost-Effective: Cheaper than rare-earth magnets (NdFeB/SmCo)
– High Resistivity: Low electrical conductivity reduces eddy current losses
– Temperature Stability: Maintain performance up to 250°C
– Corrosion Resistance: Do not require coating like NdFeB
アプリケーション
– 電子工学: Speakers, sensors, and microwave devices
– 自動車: ABS sensors, electric motor components
– Industrial: Magnetic separators, holding systems
Due to their brittleness, ferrite magnets require specialized cutting methods to avoid chipping and cracking.
2.How Are Ferrite Magnets Processed?
Ferrite magnets are manufactured through sintering, producing blocks or discs that must be cut into precise shapes. Common machining methods include:
– Sensor Components: Precision slots for Hall-effect devices
– Custom Shapes: Trapezoidal/arc cuts for motors
結論
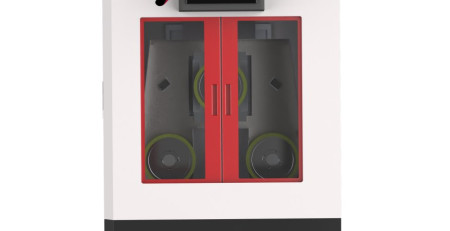
Ferrite magnets demand precision cutting to maintain performance. While grinding and laser methods have limitations, diamond wire saw cutting machines deliver the best balance of accuracy, surface quality, and cost efficiency.
For manufacturers seeking zero-defect ferrite components, upgrading to diamond wire technology reduces waste by 20% and boosts productivity by 3×.
Need a cutting solution? [お 問い合わせ] for a free sample test with your ferrite material! Compared withhow to cut neodymium magnets, ferrite allows a higher feed rate, but chipping at the exit edge is still the defect to watch.
よくある質問
What is the best way to cut ferrite magnets?
ダイヤモンドワイヤーソー切断. The thin diamond-coated wire (0.1-0.3 ミリメートル) grinds through the brittle ceramic with very low force, producing chip-free edges at Ra below 0.5 micrometers and tolerances around ±0.02 mm — without the micro-cracks of grinding or the heat damage of laser cutting.
Why do ferrite magnets chip during cutting?
Ferrite is a sintered ceramic with very low tensile strength. Rigid blades and grinding wheels concentrate mechanical stress at the cut edge, and the material fractures as the tool exits. Low-force abrasive micro-grinding with a diamond wire largely eliminates this failure mode.
Can you laser cut ferrite magnets?
Only thin sheets (under about 3 ミリメートル) and only for straight cuts. The laser’s heat-affected zone alters the magnetic properties near the cut, so for production parts a cold process like diamond wire saw cutting is preferred.
Does cutting affect ferrite’s magnetic performance?
Yes if the process adds heat or stress. Laser and hot grinding can alter properties near the cut; diamond wire saw cutting is a cold, coolant-controlled process, so the ferrite keeps its rated performance with no heat-affected zone.
Original Ensoll precision-slicing test for magnetic materials using an ESO-GM endless diamond wire saw, with measured TTV, thickness drift, 表面... 続きを読む
要約: This application report covers a high-precision straight-slicing test on optical glass
supplied by a European customer. The workpiece was a... 続きを読む