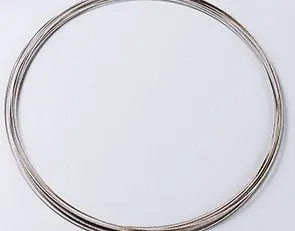
다이아몬드 와이어 루프를 이용한 연성 철 정밀 절단: 10 mm 테스트 데이터
유럽 고객을 위한 샘플 테스트 (Company R) · Ring diamond wire cutting process
개요
This report documents precision slicing of ductile iron using a ring diamond wire cutting system. 평가는 장비 및 와이어 선택을 포함한다, 절단 방법론, 공정 매개변수, 그 결과 두께 균일성, 치수 정확도, surface finish and edge integrity of the sliced parts. Test results indicate that a large-format ring diamond wire machine, 유성 냉각 및 윤활, and appropriately matched process parameters deliver stable, high-precision slicing of ductile iron at production-representative section sizes.
1. 시험 시료
| 매개변수 | 값 |
|---|---|
| 재료 | Ductile iron (nodular cast iron) |
| 경도 | 대략. 6–7 Mohs |
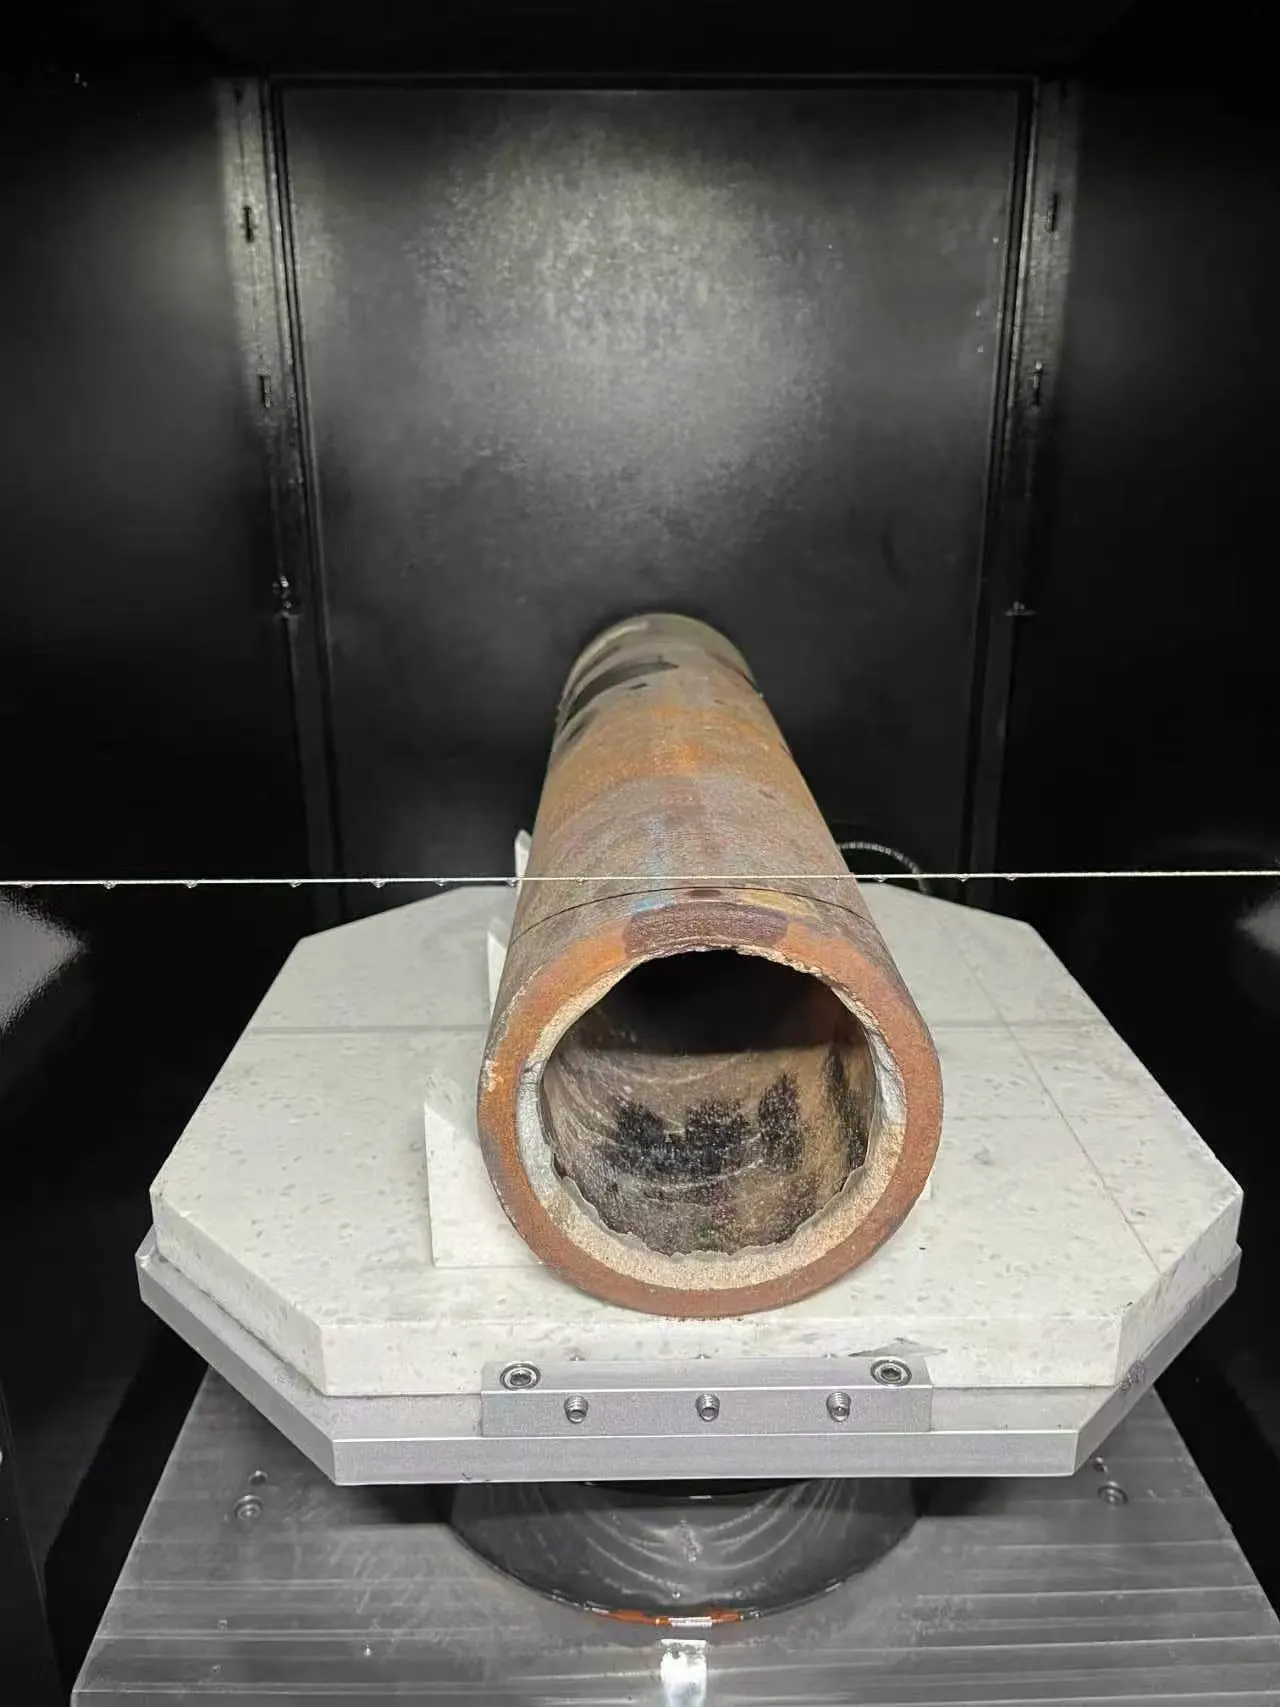
| 작업물 치수 | 500.0 밀리미터 (L) × Ø120.0 mm |
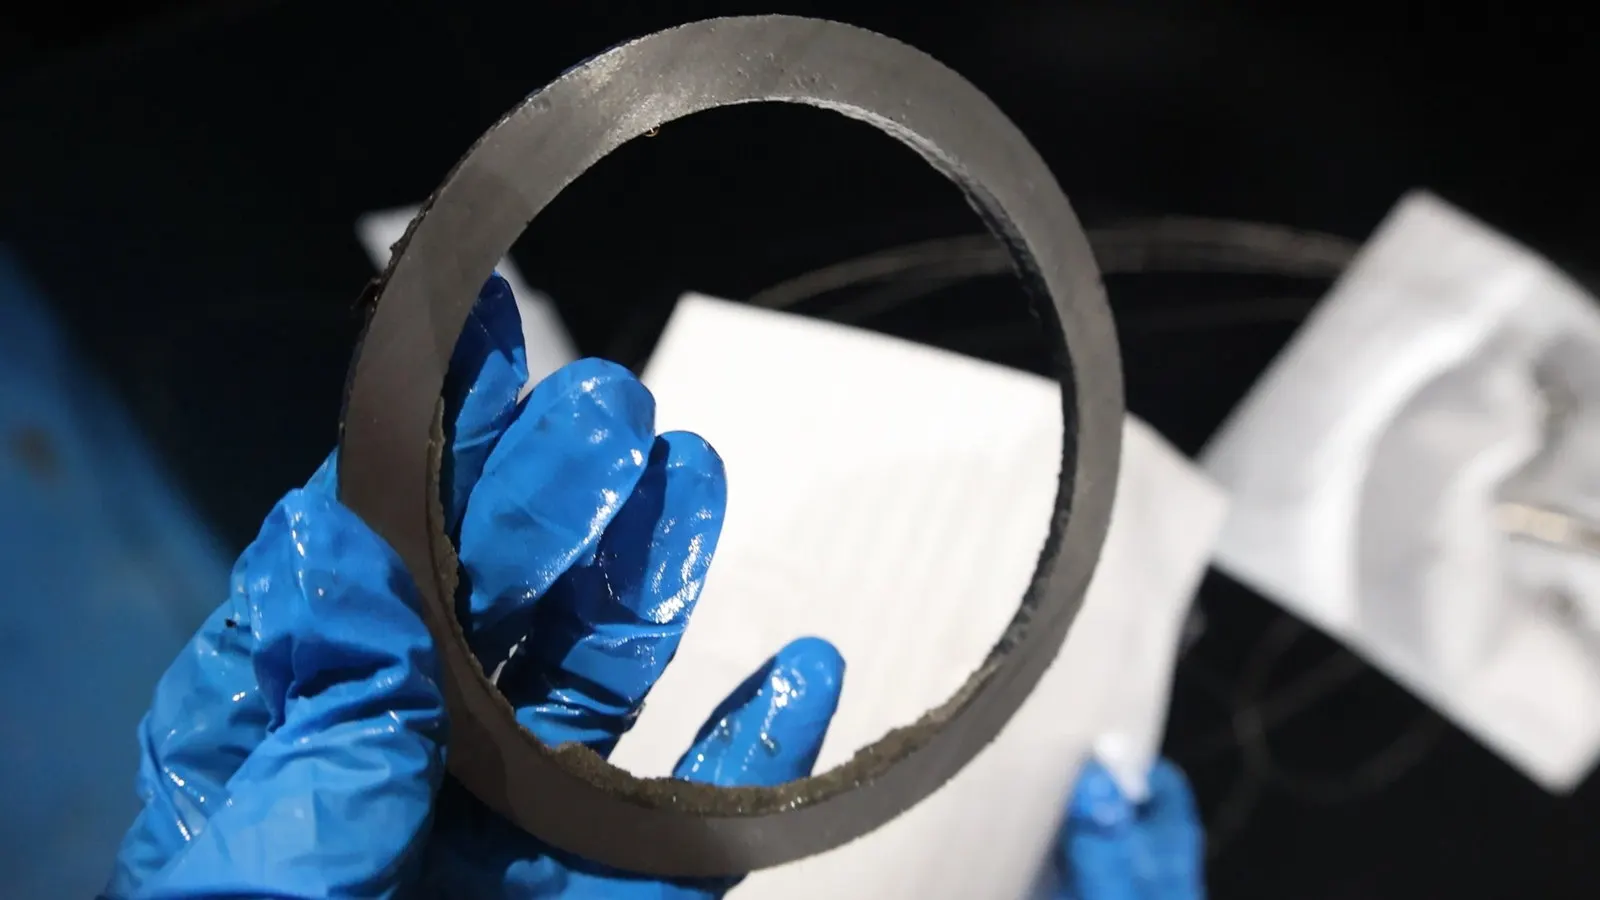
| Target slice dimensions | 10.0 밀리미터 (L) × Ø120.0 mm |
Ductile iron combines relatively high strength with a degree of toughness. Its structure consists of a metal matrix with spheroidal graphite nodules, and the difference in machinability between the matrix and the graphite phase can produce local variation in cutting behaviour along the kerf.
2. 장비 및 와이어 선택
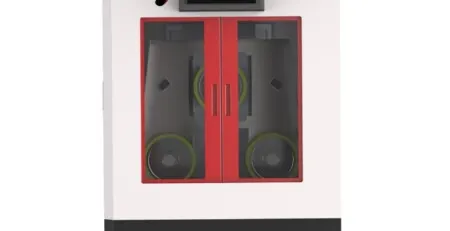
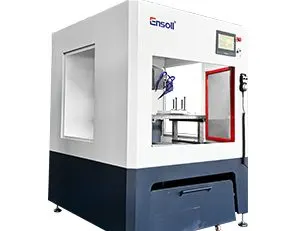
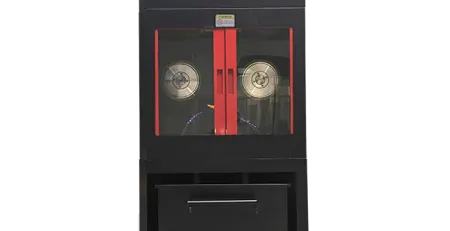
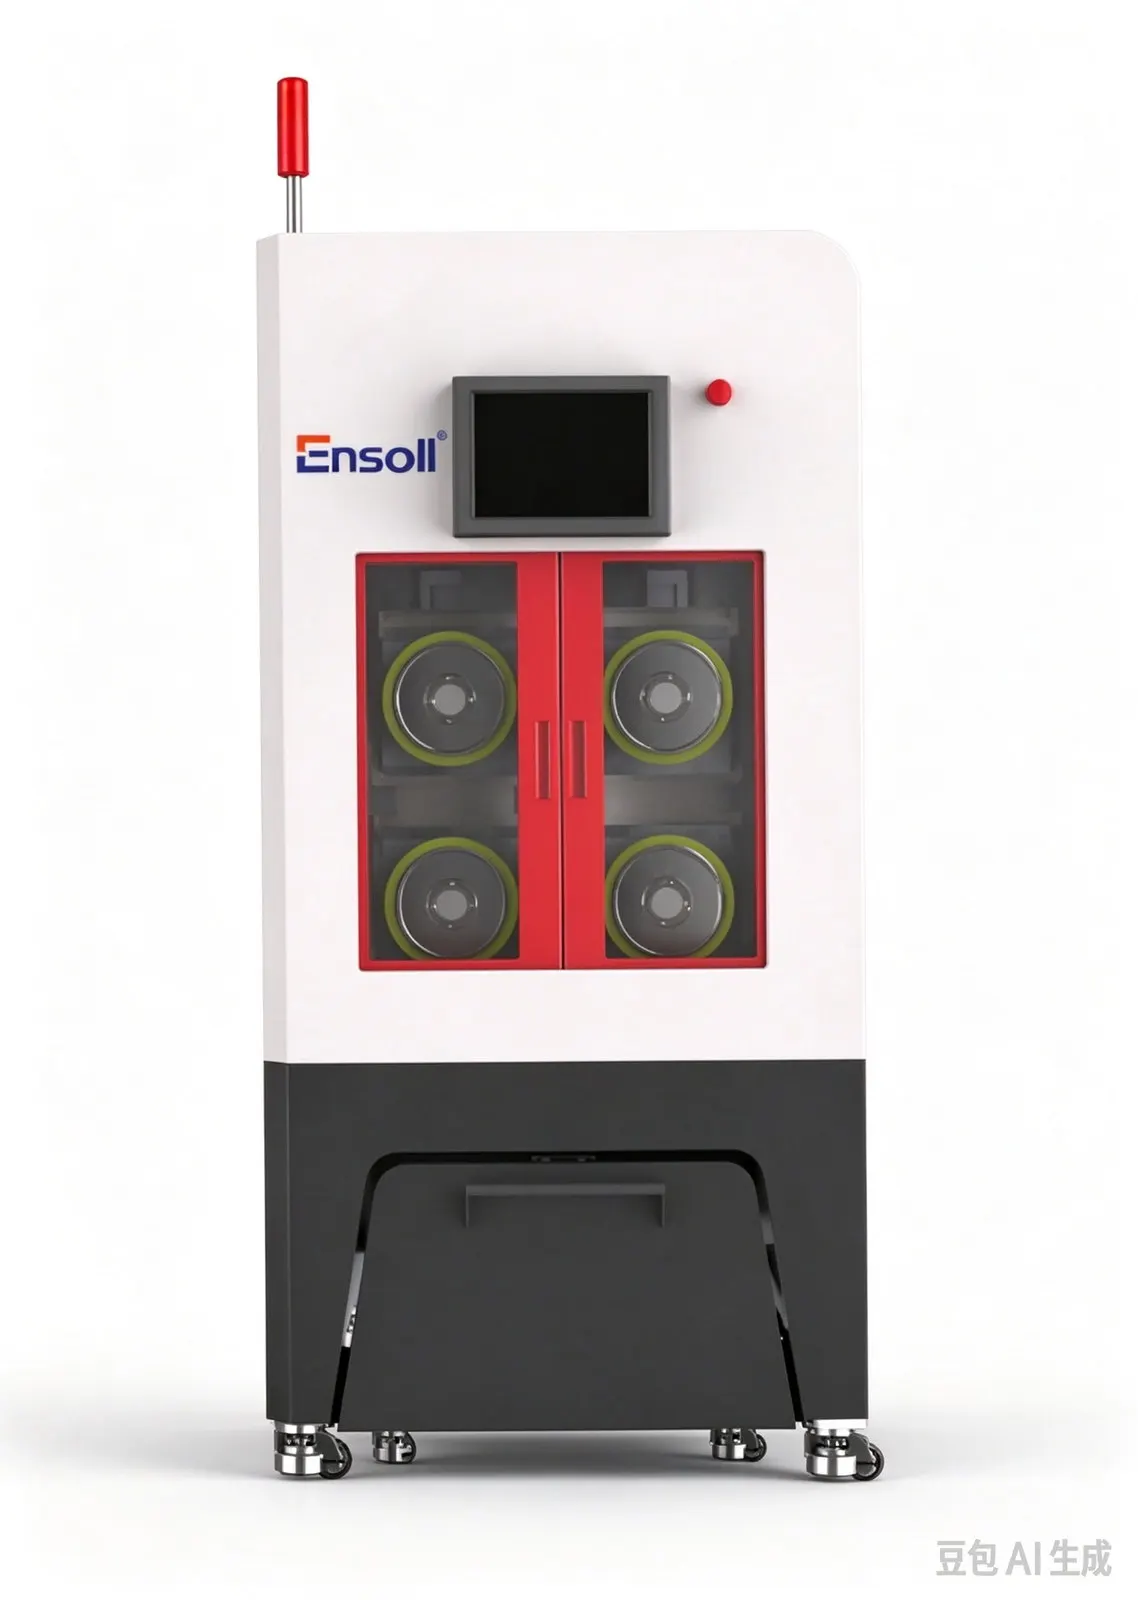
장비: ESG400-4T 시리즈. In view of the characteristics of ductile iron and the requirement to slice at a 10 mm thickness, Ensoll selected the ESG400-4T ring diamond wire cutting system with a matched cutting feed. The machine maintains a stable wire trajectory and slice dimensional accuracy.
냉각수: 유성 절단. 절삭유는 냉각 및 윤활 매체로 사용된다. It continuously lubricates and cools the contact zone between the diamond wire and the ductile iron and carries away part of the heat and cutting debris generated during cutting, reducing the effect of friction-heat accumulation and debris build-up on the machining condition. Controlled oil supply helps maintain a stable cutting zone.
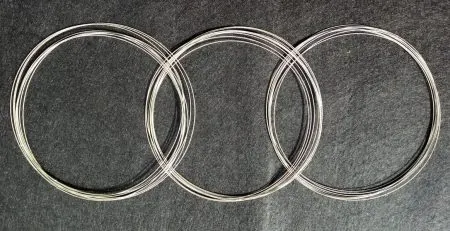
와이어: 완전히 도금됨. 완전히 도금된 다이아몬드 와이어가 선택되었습니다., with the diamond abrasive grains bonded to the wire core by electroplating. The plated bond improves grain adhesion and distribution uniformity, so the wire maintains a consistent grinding capability and material removal behaviour during cutting. This reduces grain pull-out and wire wear, which matters for a metal workpiece of this section size.
3. 절단 방식 및 장비 장점
갠트리 절단 구성. 갠트리 구조는 높은 전체 강성과 주행 안정성을 제공합니다, which reduces the effect of machine vibration and structural deformation on the wire trajectory and keeps the cut stable. This limits the influence of changes in cutting load on slice position and dimensional accuracy in the ductile iron. 이 기계는 절단 중 발생하는 미스트를 신속하게 제거하는 미스트 추출 시스템이 장착되어 있습니다..
지능형 장력 제어. 이 시스템은 절단 조건에 따라 다이아몬드 와이어 장력을 실시간으로 조절하며, 일정 장력 모드와 가변 장력 모드를 모두 지원합니다., 와이어를 안정적으로 작동시키기. Well-matched tension control reduces fluctuation in the wire trajectory and limits localised uneven loading and the risk of wire breakage caused by tension variation, reducing the occurrence of slice defects.
와이어 파단 메모리. 다이아몬드 와이어가 파손되거나 기계가 비정상적으로 정지하면, 시스템은 현재 가공 위치와 관련 작동 상태를 자동으로 기록합니다.. 와이어를 교체한 후, 절단은 기록된 위치에서 재개됩니다., reducing dimensional deviation and material loss from re-positioning and repeat machining. This improves the continuity of ductile iron slicing.
Large workpiece capacity and high-speed cutting. The ESG400-4T provides a large effective working envelope, accommodating ductile iron workpieces of substantial section size. The ring diamond wire runs in continuous circulation, and wire speed can reach three to four times that of conventional wire-cut machines, which raises material removal efficiency while keeping the cut stable.
4. 공정 매개변수 및 냉각 방법
| 매개변수 | 값 |
|---|---|
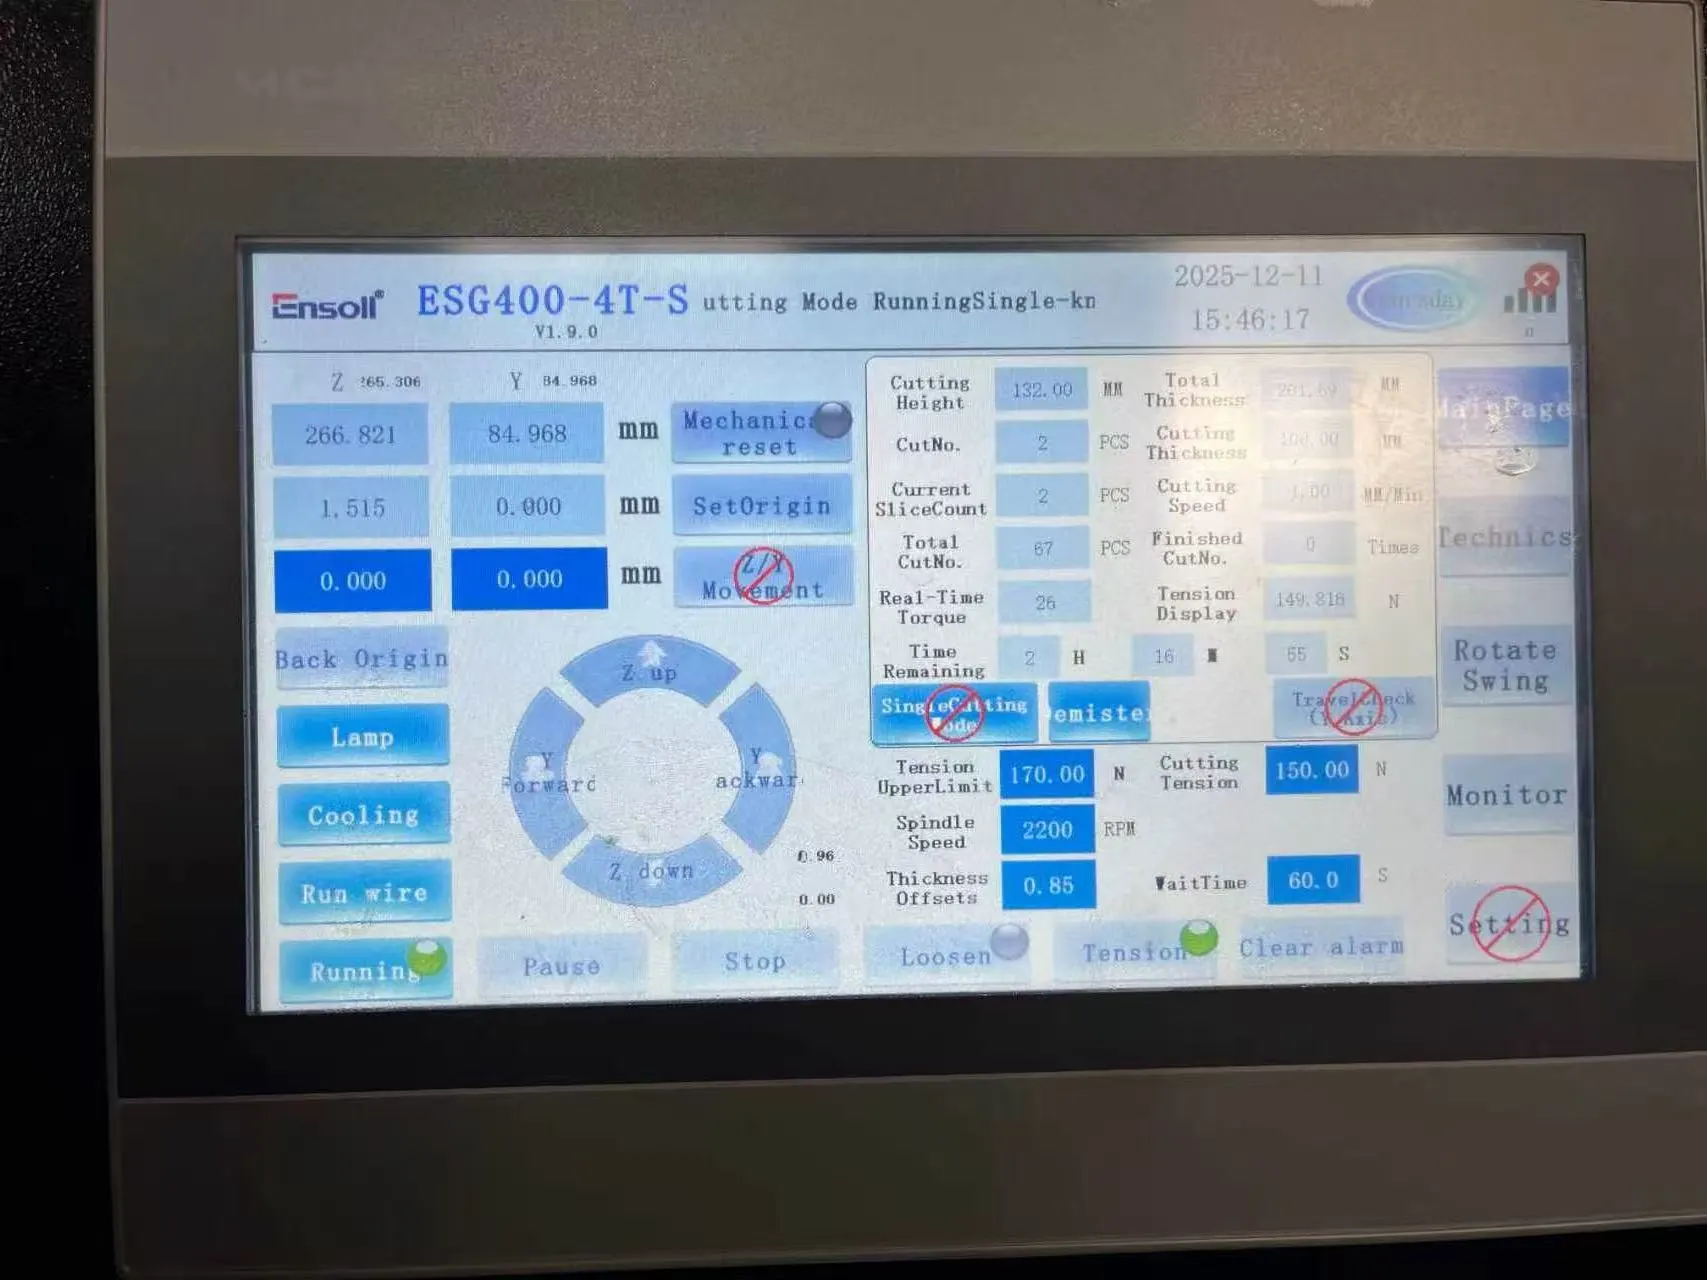
| 와이어 직경 (밀리미터) | 0.80 × 2600 |
| 와이어 이동 속도 (mm / 분) | 1.5 |
| 절단 폭 (밀리미터) | 120 |
| 와이어 장력 (N) | 150 |
| 와이어 속도 (엠/초) | 32 |
| 와이어 보우 시간 (초) | 60 |
5. 절단 성능 및 결과
5.1 TTV 시험 데이터 (단위: 밀리미터)
총 두께 변동 (TTV) 9점 격자를 사용하여 측정됨, 진공 척 스테이지에서 이중 탐침 두께 측정 방법. The measurement was applied to ductile iron slices produced by ring diamond wire cutting. 측정 전에 기기는 열 안정화와 표준 두께 블록을 통한 보정을 거쳤습니다. 명목상 절단 두께는 10.000 밀리미터.
| 시료 | 9점 두께 측정 | T최대 | T최소 | TTV |
|---|---|---|---|---|
| S01 | 9.994, 9.997, 10.000 9.996, 10.001, 10.004 9.998, 10.005, 10.008 |
10.008 | 9.994 | 0.014 |
| S02 | 9.990, 9.994, 9.998 9.995, 10.000, 10.003 9.997, 10.004, 10.007 |
10.007 | 9.990 | 0.017 |
| S03 | 9.986, 9.991, 9.995 9.993, 9.998, 10.002 9.996, 10.003, 10.009 |
10.009 | 9.986 | 0.023 |
| S04 | 9.995, 9.998, 10.001 9.997, 10.002, 10.005 9.999, 10.006, 10.010 |
10.010 | 9.995 | 0.015 |
| S05 | 9.992, 9.996, 9.999 9.994, 10.000, 10.004 9.998, 10.005, 10.009 |
10.009 | 9.992 | 0.017 |
| S06 | 9.988, 9.993, 9.997 9.994, 9.999, 10.003 9.996, 10.004, 10.008 |
10.008 | 9.988 | 0.020 |
평가. Nine-point grid measurement was applied to six ductile iron slices. TTV 값은 0.014, 0.017, 0.023, 0.015, 0.017 그리고 0.020 밀리미터, 배치 전체에서 0.014–0.023 mm 범위였으며, 평균 TTV는 약 0.018 mm 위에 10.000 mm 명목 두께. The results confirm good thickness uniformity when slicing a metal workpiece of this section size.
5.2 두께 허용치 데이터 (단위: 밀리미터)
두께 허용오차는 9점 두께 데이터를 사용하여 도출되었습니다, 사용하여 10.000 mm를 명목 두께로 하여. 각 측정 위치에서 양의 두께 편차와 음의 두께 편차를 계산했으며, 여섯 샘플의 결과를 모두 집계하였다. 최대 양의 편차, 두께 일관성을 평가하기 위해 최대 음의 편차와 전체 편차 범위를 결정하였다.
| 시료 | 평균 두께 | 두께 편차 |
|---|---|---|
| S01 | 10.000 | 0.000 |
| S02 | 9.999 | −0.001 |
| S03 | 9.997 | −0.003 |
| S04 | 10.001 | +0.001 |
| S05 | 10.000 | 0.000 |
| S06 | 9.998 | −0.002 |
| 최대 양의 편차 | — | +0.010 밀리미터 |
| 최대 음의 편차 | — | −0.014 mm |
| 두께 허용 범위 | — | ±0.012 mm |
평가. 명목 두께에 대하여 10.000 밀리미터, the six slices showed mean thicknesses of 9.997–10.001 mm, 배치 평균은 명목값에 근접하였다. 모든 측정 지점에서 두께 편차는 −0.014 mm에서 측정되었으며 +0.010 밀리미터, 최대 절대 편차는 0.014 밀리미터.
5.3 표면 거칠기 Ra 데이터 (단위: μm의)
표면 거칠기 (Ra) was measured by stylus profilometry on the ductile iron slices after ring diamond wire cutting. 대표적인 측정 위치는 중앙과 절단 끝 면을 따라 양쪽에 취해졌으며, 표면 프로파일 데이터는 스타일러스 프로파일로미터로 수집되었으며, 각 위치에서 거칠기 매개변수 Ra가 기록되었으며.
| 시료 | 중앙 | 중간 왼쪽 | 중간 오른쪽 | 평균 Ra |
|---|---|---|---|---|
| S01 | 1.12 | 1.18 | 1.15 | 1.15 |
| S02 | 1.05 | 1.11 | 1.08 | 1.08 |
| S03 | 1.28 | 1.35 | 1.31 | 1.31 |
| S04 | 0.98 | 1.04 | 1.01 | 1.01 |
| S05 | 1.16 | 1.22 | 1.19 | 1.19 |
| S06 | 1.09 | 1.15 | 1.12 | 1.12 |
평가. 여섯 샘플의 평균 Ra는 1.01 받는 사람 1.31 μm의, 그 사이의 모든 개별 측정값과 함께 0.98 그리고 1.35 μm의. The spread across measurement positions on each slice is modest, indicating a consistent surface finish along the cut face on a metal workpiece of this size.
5.4 Edge Condition Data (단위: μm의)
Edge defects were quantified by optical imaging on a toolmaker’s microscope. 시료 가장자리는 측정 전에 세척되고 기기의 배율과 측정 척도가 보정되었다. 슬라이스 가장자리는 현미경으로 검사되었다, identifiable edge defects were located and measured at four points per sample, 최대 값이 유지됨.
| 시료 | 포인트 1 | 포인트 2 | 포인트 3 | 포인트 4 | 최대. edge defect |
|---|---|---|---|---|---|
| S01 | 5.2 | 6.1 | 5.7 | 6.5 | 6.5 |
| S02 | 4.8 | 5.5 | 6.0 | 5.2 | 6.0 |
| S03 | 7.1 | 8.3 | 9.2 | 8.0 | 9.2 |
| S04 | 4.3 | 5.0 | 5.6 | 4.8 | 5.6 |
| S05 | 6.0 | 6.8 | 7.4 | 6.5 | 7.4 |
| S06 | 5.4 | 6.2 | 6.8 | 5.9 | 6.8 |
평가. Toolmaker’s microscope inspection of the six ductile iron slices gave maximum edge defect values of 6.5, 6.0, 9.2, 5.6, 7.4 그리고 6.8 μm의, 전체 최대치 9.2 μm의. S04 showed the best edge integrity and S03 the largest defect at 9.2 μm의.
6. 결론
The good results obtained in this high-precision slicing trial of ductile iron stemmed mainly from the combined effect of a purpose-built cutting machine, 냉각 및 윤활 방법, 그리고 공정 매개변수의 정확한 일치. Ductile iron has relatively high strength and a degree of toughness, and its structure consists of a metal matrix with spheroidal graphite. During ring diamond wire cutting, the difference between the matrix and the graphite phase can cause local variation in cutting behaviour, which places particular demands on machine rigidity and parameter matching.
장비. An ESG400-4T ring diamond wire cutting system was used. The machine provides a large effective working envelope for larger workpieces and a high-rigidity structure that reduces the effect of vibration and structural deformation on the wire trajectory. The ring diamond wire runs in continuous circulation at speeds well above conventional wire-cut machines, which raises removal efficiency without sacrificing cut stability.
냉각 및 윤활. 절삭유가 냉각 및 윤활 매체로 사용되었다. It continuously lubricates and cools the wire–workpiece contact zone, reduces friction at the cutting interface, and carries away part of the cutting heat and debris, improving conditions in the cutting zone. For a material with the strength and toughness of ductile iron, effective lubrication is essential to consistent surface finish.
공정 매개변수. 와이어 속도, feed rate and other key parameters were matched to the properties of ductile iron and to the 10 mm slice requirement. Coordinating wire speed with workpiece feed keeps material removal steady and avoids localised increases in cutting load from excessive feed, or unstable cutting from mismatched parameters.
전체. Taken together with slice dimensional accuracy, 표면 거칠기 (Ra) and edge quality, the combination of the ESG400-4T ring diamond wire machine, 유성 냉각 및 윤활, and appropriately matched cutting parameters achieves a well-matched process for ductile iron. The results support ring diamond wire cutting as a practical route for precision slicing of ductile iron at this section size.