Контурная резка магнитных материалов с помощью бесконечной проволочной пилы
Ensoll протестировала образец магнитного материала европейского клиента с помощью специально настроенной бесконечной проволочной пилы с алмазным покрытием. The goal was to cut an irregular contour while keeping edge chipping, шероховатость поверхности, and contour deviation under control. The process used an endless diamond wire saw machine paired with a полностью покрытая алмазная проволочная петля.
- A diamond wire loop process cut an irregular contour in an 80 x 50 x 50 mm magnetic-material sample, holding feature deviations within -0.110 / +0.073 миллиметр.
- The matched setup was a 0.5 mm fully coated diamond wire loop at 29 М / сек, 120 N tension, vertical clamping and cutting-oil cooling.
- Surface roughness stayed in a narrow Ra 0.53-0.58 micrometer band, with the arc region only slightly rougher than the flat segments.
- Maximum edge chipping was just 2.8 микрометры, making the process a practical reference for clean irregular cuts before secondary finishing.
Contour work on rare-earth blocks follows the same principles as как резать неодимовые магниты, with lower feed rates on tight radii.
Test Result at a Glance
- Материал: magnetic material supplied by a European customer
- Размер заготовки: 80 x 50 x 50 миллиметр
- Cutting target: irregular contour machining
- Cooling medium: cutting oil
- Проволочная петля: 0.5 mm fully coated loop, 2305 mm length
- Linear wire speed: 29 М / сек
- Напряжение проволоки: 120 N
- Wire bowing time: 200 s
1. Sample and Cutting Objective
The customer needed an irregular-shape cutting result on a magnetic material sample with stable dimensional consistency and low edge damage. Магнитные материалы can be brittle, locally sensitive to stress concentration, and prone to contour-related chipping. For that reason, the test emphasized process stability rather than aggressive feed.
Ensoll used an endless diamond wire process because it offers continuous one-direction cutting, narrow kerf loss, and gentler load control than many conventional cutting methods. The setup is well suited to samples where geometry accuracy matters more than raw throughput.
2. Equipment and Process Setup
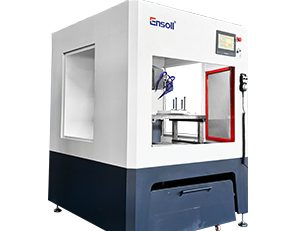
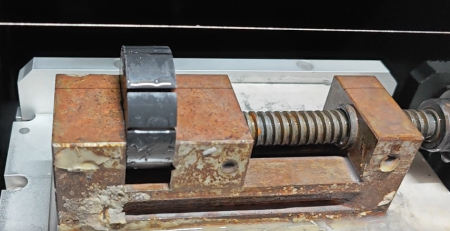
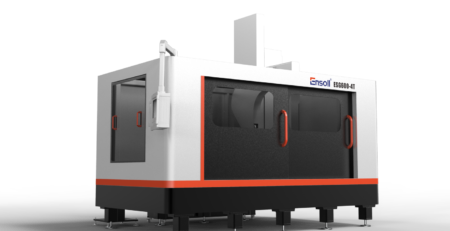
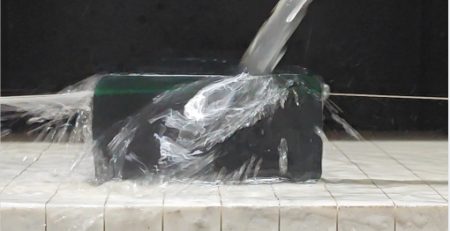
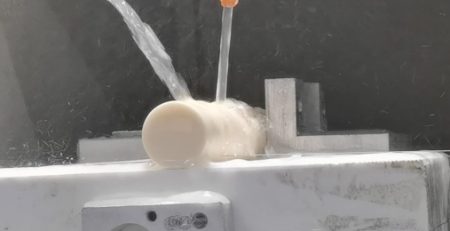
The machine platform was a customized vertical endless diamond wire cutting system. The sample was clamped vertically to help stabilize force distribution across the cut path, and cutting oil was applied to support cooling, смазкой, and chip evacuation.
| Параметр | Значение |
|---|---|
| Станок | Customized vertical endless diamond wire saw |
| Wire specification | 0.5 mm fully coated wire loop, 2305 mm length |
| Скорость проволоки | 29 М / сек |
| Напряжение проволоки | 120 N |
| Wire bowing time | 200 s |
| Ширина реза | 50 миллиметр |
| Cooling and lubrication | Резательное масло |
The cutting interface was monitored in real time so the operator could confirm the motion state and parameter values during the cut.
3. Результаты резки
The contour was checked at several feature positions. For this test, the outer arc width, bottom width, H1 height, and H2 height were recorded. The data showed that the sample remained stable overall, with the H2 direction showing the largest variation and therefore the clearest opportunity for further tuning if a tighter drawing tolerance is required.
| Функция | TTV (миллиметр) |
|---|---|
| Outer arc width | 0.020 |
| Bottom width | 0.010 |
| H1 height | 0.010 |
| H2 height | 0.040 |
| Функция | Design Dimension | Average Measured Dimension | Отклонение |
|---|---|---|---|
| Outer arc width | 12.500 | 12.390 | -0.110 |
| Bottom width | 7.500 | 7.403 | -0.097 |
| H1 height | 12.500 | 12.393 | -0.107 |
| H2 height | 13.750 | 13.823 | +0.073 |
| Max positive deviation | +0.073 | ||
| Max negative deviation | -0.110 | ||
| Total deviation span | 0.183 | ||
The measured feature deviations were small enough to confirm that the contour was formed consistently. В то же время, the unequal deviation directions tell us that this kind of irregular shape should be tuned by feature zone rather than by one blanket parameter for the whole cut.
4. Результаты шероховатости поверхности
Surface roughness was measured at representative positions across the sample. The flat regions were slightly smoother than the curved transition area, which is a common pattern in irregular cutting.
| Measurement Area | Ra-1 | Ra-2 | Ra-3 | Среднее значение Ra (микрометры) |
|---|---|---|---|---|
| Center region | 0.52 | 0.54 | 0.53 | 0.53 |
| Left region | 0.56 | 0.57 | 0.55 | 0.56 |
| Right region | 0.55 | 0.58 | 0.56 | 0.56 |
| Arc region | 0.57 | 0.59 | 0.58 | 0.58 |
Результат: the sample stayed in a narrow roughness band across the measured areas. The arc zone was slightly rougher than the straight segments, so it should be watched closely if the next sample needs a lower Ra in the curved section.
5. Результаты сколов кромок
Edge chipping was measured along the contour after cutting. The bevel edges showed the largest defects, while the arc region stayed more stable.
| Test Point | Положение 1 | Положение 2 | Положение 3 | Положение 4 | Max Chipping (микрометры) |
|---|---|---|---|---|---|
| Top arc | 1.2 | 1.4 | 1.3 | 1.8 | 1.8 |
| Left bevel edge | 1.5 | 1.7 | 1.6 | 2.8 | 2.8 |
| Right bevel edge | 1.4 | 1.6 | 1.5 | 1.5 | 1.6 |
| Bottom region | 1.8 | 2.0 | 1.9 | 1.6 | 2.0 |
Результат: the maximum chipping stayed low across the contour, and the largest defect was still only 2.8 микрометры. That makes the process a practical reference for customers who need a clean irregular cut on magnetic materials before secondary finishing.
6. Инженерное заключение
This sample test shows that an endless diamond wire process can cut an irregular magnetic-material contour with stable force distribution, низкая шероховатость, and limited edge damage. The result depended on a matching set of process choices: vertical cutting, cutting oil, 120 N tension, 29 m/s wire speed, and careful path control.
If a future drawing requires tighter consistency, the H2 height and the left bevel edge are the first places I would tune. For the current sample, however, the overall contour quality is strong enough to serve as a practical process reference.
Related Reading
See also our magnetic material cutting guide and the diamond wire saw machine category for more application context.
Разрешение на цитирование: Если вы считаете эту статью полезной, Ensoll разрешает цитировать или ссылаться на нее, при условии, что вы включите ссылку на эту страницу как на исходный источник.
Часто задаваемые вопросы
How do you cut irregular shapes in brittle magnetic materials?
A CNC diamond wire loop saw steers a thin diamond-coated wire along the programmed contour. Because it removes material by low-force micro-grinding instead of shearing, it avoids the edge chipping and stress cracks that rigid blades cause on brittle magnetic materials.
What surface roughness can diamond wire loop cutting achieve on magnetic materials?
In this sample test the average Ra stayed between 0.53 и 0.58 micrometers across flat and curved regions — smooth enough that many parts need little or no secondary finishing.
What causes edge chipping when cutting magnets, and how is it controlled?
Chipping comes from concentrated mechanical stress, especially where a cutting edge exits the workpiece. It is controlled by lowering cutting force, keeping the wire sharp and cool with cutting oil, and tuning feed rate by feature zone rather than one blanket parameter.
Which parameters matter most for contour accuracy?
Напряжение проволоки, wire speed and feed control matter most. This test used 120 N tension and 29 m/s wire speed; measured TTV per feature stayed between 0.010 и 0.040 миллиметр, with the H2 height identified as the first place to tune for tighter tolerances.
Технический контент проверен инженерной командой Ensoll — производителя алмазных проволочных петель с 10+ многолетним производственным опытом.