Точное нарезывание магнитных материалов с алмазной проволочной петлей: 2 мм Тестовые данные
Пробное тестирование для европейского клиента (Company P) · Ring diamond wire cutting process
Обзор
This report documents precision slicing of magnetic material using a ring diamond wire cutting system. Оценка охватывает оборудование и выбор проволоки, методологию резки, параметры процесса, и полученную равномерность толщины, размерную точность, surface quality and edge integrity of the sliced parts. Test results indicate that a gantry-type ring diamond wire machine, масляная охлаждение и смазка, and appropriately matched process parameters deliver stable, high-precision slicing of magnetic material.
1. тестовый образец
| Параметр | Значение |
|---|---|
| Материал | Magnetic material |
| Твёрдость | приблизительно. 6–7 Мohs |
| Размеры заготовки | 60 мм × 26.0 мм × 3.0 миллиметр |
| Target slice dimensions | 2.0 мм × 26.0 мм × 3.0 миллиметр |
2. Выбор оборудования и проволоки
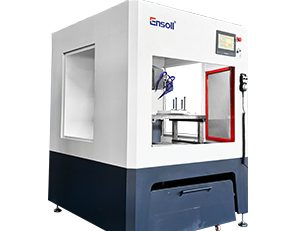
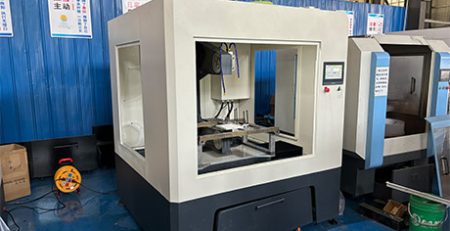
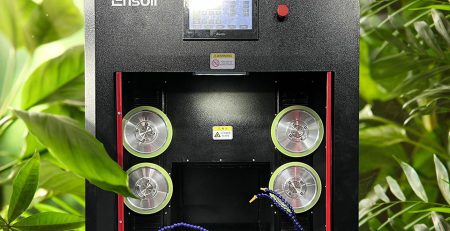
Оборудование: ESO-GM. In view of the hard-brittle characteristics of magnetic material and the requirement to slice at a 2 мм толщины, Ensoll selected the ESO-GM gantry-type ring diamond wire cutting system with a top-down vertical feed. The gantry configuration maintains a stable wire trajectory and slice dimensional accuracy.
Охлаждающая жидкость: резка с использованием масла. В качестве охлаждающей и смазывающей среды используется режущее масло. It improves lubrication and heat dissipation in the contact zone between the diamond wire and the magnetic material, reduces friction resistance and localised heat accumulation during cutting, and limits fluctuation in cutting load and its effect on the material. This helps suppress chipping, micro-cracking and surface damage.
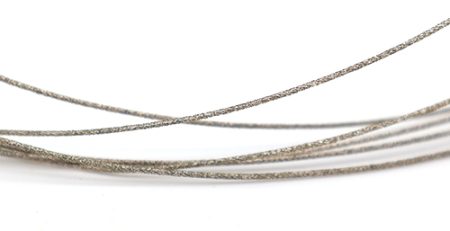
Проволока: fully plated. A fully plated diamond wire was selected. The plated construction improves the bonding strength between the diamond abrasive grains and the wire core and provides a more uniform grain distribution. This sustains a continuous and stable material removal rate, reduces grain pull-out and wire wear, and contributes to lower chipping, micro-cracking and surface damage when slicing magnetic material.

3. Метод резки и преимущества оборудования
Gantry cutting configuration. The gantry structure provides high overall rigidity and running stability. The top-down vertical feed helps keep the diamond wire trajectory stable and reduces the influence of changes in cutting force on kerf position and dimensional accuracy in the magnetic material. The machine is equipped with a mist-extraction system that promptly removes mist generated during cutting.
Интеллектуальное управление натяжением. The system adjusts diamond wire tension in real time according to cutting conditions and supports both constant-tension and variable-tension modes, обеспечение стабильной работы проволоки. Stable wire tension reduces fluctuation in the cutting trajectory and limits localised uneven loading and the risk of wire breakage caused by tension variation, which in turn reduces defects in the magnetic material.
Запоминание обрыва проволоки. Если алмазная проволока порвется или станок остановится аномально, the system automatically records the current machining position and associated operating state. После замены проволоки, cutting resumes from the recorded position, reducing dimensional deviation and material loss caused by re-positioning and repeat machining. This improves the continuity of magnetic material slicing and lowers the risk of repeated cutting.
High-rigidity one-piece cast iron frame. The one-piece cast iron frame provides high structural stiffness and vibration resistance, reducing the effect of machine vibration and structural deformation on the wire trajectory during machining. For a hard-brittle material such as magnetic material, the high-rigidity frame helps damp vibration and fluctuation in cutting force during the cut and keeps the diamond wire running stably.
4. Process Parameters and Cooling Method
| Параметр | Значение |
|---|---|
| Диаметр проволоки (миллиметр) | 0.35 × 1880 |
| Wire traverse speed (мм/мин) | 2 |
| Ширина реза (миллиметр) | 60 |
| Напряжение проволоки (N) | 140 |
| Скорость проволоки (М / сек) | 26 |
| Wire bow time (s) | 60 |

5. Cutting Performance and Results

5.1 Данные теста TTV (Единица: миллиметр)
Изменение общей толщины (TTV) измерялся с использованием сетки из девяти точек, dual-probe thickness gauging method on a vacuum-chuck stage. The measurement was applied to magnetic material slices produced by ring diamond wire cutting. Before measurement the instrument was thermally stabilised and calibrated against a standard thickness block. Номинальная толщина среза составляла 2.000 миллиметр.
| Образец | Nine-point thickness readings | Tmax | Tmin | TTV |
|---|---|---|---|---|
| S01 | 1.992, 1.996, 1.998 1.995, 2.000, 2.003 1.997, 2.004, 2.006 |
2.006 | 1.992 | 0.014 |
| S02 | 1.988, 1.993, 1.997 1.995, 2.001, 2.004 1.999, 2.006, 2.008 |
2.008 | 1.988 | 0.020 |
| S03 | 1.985, 1.990, 1.994 1.992, 1.998, 2.002 1.996, 2.004, 2.009 |
2.009 | 1.985 | 0.024 |
| S04 | 1.994, 1.997, 2.000 1.996, 2.001, 2.004 1.999, 2.005, 2.007 |
2.007 | 1.994 | 0.013 |
| S05 | 1.989, 1.994, 1.997 1.993, 1.999, 2.003 1.996, 2.005, 2.010 |
2.010 | 1.989 | 0.021 |
Assessment. Nine-point grid measurement was applied to five magnetic material slices. TTV values were 0.014, 0.020, 0.024, 0.013 и 0.021 миллиметр, spanning 0.013–0.024 mm across the batch, with a mean TTV of approximately 0.018 mm on a 2.000 номинальной толщиной мм. The results confirm good thickness uniformity in magnetic material slicing.
5.2 Данные по допуску толщины (Единица: миллиметр)
Thickness tolerance was derived from the nine-point thickness data, Использование 2.000 mm as the nominal thickness. The positive and negative thickness deviation were calculated at each measurement position and the results from all five samples were aggregated. The maximum positive deviation, maximum negative deviation and overall deviation range were then determined to evaluate thickness consistency.
| Образец | Mean thickness | Thickness deviation |
|---|---|---|
| S01 | 1.999 | −0.001 |
| S02 | 1.999 | −0.001 |
| S03 | 1.997 | −0.003 |
| S04 | 2.000 | 0.000 |
| S05 | 1.998 | −0.002 |
| Максимальное положительное отклонение | — | +0.010 миллиметр |
| Максимальное отрицательное отклонение | — | −0.015 mm |
| Диапазон допуска по толщине | — | ±0.0125 mm |
Assessment. Относительно номинальной толщины 2.000 миллиметр, the five slices showed mean thicknesses of 1.997–2.000 mm, with small average deviations across the batch. Over all measurement points the thickness deviation ranged from −0.015 mm to +0.010 миллиметр, with a maximum absolute deviation of 0.015 миллиметр.
5.3 Данные по шероховатости поверхности Ra (Единица: мкм)
Шероховатость поверхности (Ra) was measured by stylus profilometry on the magnetic material slices after ring diamond wire cutting. Представительные позиции измерений были выбраны в центре и по обеим сторонам вдоль торцевой поверхности реза, данные профиля поверхности были получены с помощью стилусного профилометра, и параметр шероховатости Ra фиксировался в каждой позиции.
| Образец | Centre | Mid-left | Mid-right | Среднее Ra |
|---|---|---|---|---|
| S01 | 0.52 | 0.56 | 0.49 | 0.52 |
| S02 | 0.48 | 0.53 | 0.50 | 0.50 |
| S03 | 0.61 | 0.66 | 0.58 | 0.62 |
| S04 | 0.46 | 0.51 | 0.48 | 0.48 |
| S05 | 0.55 | 0.59 | 0.53 | 0.56 |
Assessment. Mean Ra across the five samples ranged from 0.48 Кому 0.62 мкм, with all individual readings between 0.46 и 0.66 мкм. The narrow spread across the three measurement positions on each slice indicates a uniform surface finish along the cut face.
5.4 Данные о склеивании края (Единица: мкм)
Edge chipping was quantified by optical imaging on a toolmaker’s microscope. Specimen edges were cleaned before measurement and the magnification and measurement scale of the instrument were calibrated. The slice edge was then inspected under the microscope, identifiable chipping defects were located and measured at four points per sample, and the maximum value was retained.
| Образец | Point 1 | Point 2 | Point 3 | Point 4 | Макс. сколы |
|---|---|---|---|---|---|
| S01 | 4.2 | 5.1 | 4.8 | 5.6 | 5.6 |
| S02 | 3.8 | 4.6 | 5.2 | 4.4 | 5.2 |
| S03 | 5.6 | 6.8 | 7.5 | 6.2 | 7.5 |
| S04 | 3.5 | 4.1 | 4.6 | 3.9 | 4.6 |
| S05 | 4.9 | 5.7 | 6.3 | 5.2 | 6.3 |
Assessment. Toolmaker’s microscope inspection of the five magnetic material slices gave maximum chipping values of 5.6, 5.2, 7.5, 4.6 и 6.3 мкм, with an overall maximum of 7.5 мкм. S04 showed the best edge integrity and S03 the largest chipping at 7.5 мкм.

6. Заключение
The good results obtained in this high-precision slicing trial of magnetic material stemmed mainly from the combined effect of a purpose-built cutting machine, метод охлаждения и смазки, и правильно подобранные параметры процесса. Magnetic material is relatively hard with a degree of brittleness. During ring diamond wire cutting the abrasive grains act continuously on the material surface, and material removal is affected by cutting load, wire running condition and the machining parameters.
Оборудование. An ESO-GM gantry-type ring diamond wire cutting system was used. The gantry structure provides high overall rigidity and running stability and gives reliable mechanical support for workpiece clamping and continuous wire travel. Stable motion and feed control keep the diamond wire on the programmed path throughout the cut.
Охлаждение и смазывание. Cutting oil was used as the cooling and lubricating medium. During cutting the diamond wire remains in continuous contact with the workpiece and the abrasive grains grind the material continuously, generating friction heat in the contact zone. Cutting oil improves lubrication at the cutting interface, carries away part of the cutting heat, and reduces friction between the wire and the workpiece, which helps limit thermal effects and edge damage.
Process parameters. Скорость проволоки, feed rate and other key parameters were matched to the hardness, brittleness and target slice thickness of the magnetic material. Parameters were set to maintain stable wire travel and continuous material removal, avoiding feed rates high enough to raise cutting load, or a mismatch between wire speed and feed rate that would degrade slice quality.
Overall. Taken together with slice dimensional accuracy, thickness tolerance, шероховатость поверхности (Ra) and cut-edge quality, the combination of the ESO-GM gantry cutting machine, масляная охлаждение и смазка, and appropriately matched process parameters allows ring diamond wire cutting to meet the precision slicing requirements for this magnetic material.