金刚石线圈对球墨铸铁的精密切片: 10 毫米 测试数据
Sample testing for a European client (Company R) · Ring diamond wire cutting process
概述
This report documents precision slicing of ductile iron using a ring diamond wire cutting system. The evaluation covers equipment and wire selection, cutting methodology, 工艺参数, and the resulting thickness uniformity, 尺寸精度, surface finish and edge integrity of the sliced parts. Test results indicate that a large-format ring diamond wire machine, oil-based cooling and lubrication, and appropriately matched process parameters deliver stable, high-precision slicing of ductile iron at production-representative section sizes.
1. Test Specimen
| 参数 | 数值 |
|---|---|
| 材料 | Ductile iron (nodular cast iron) |
| 硬度 | approx. 6–7 Mohs |
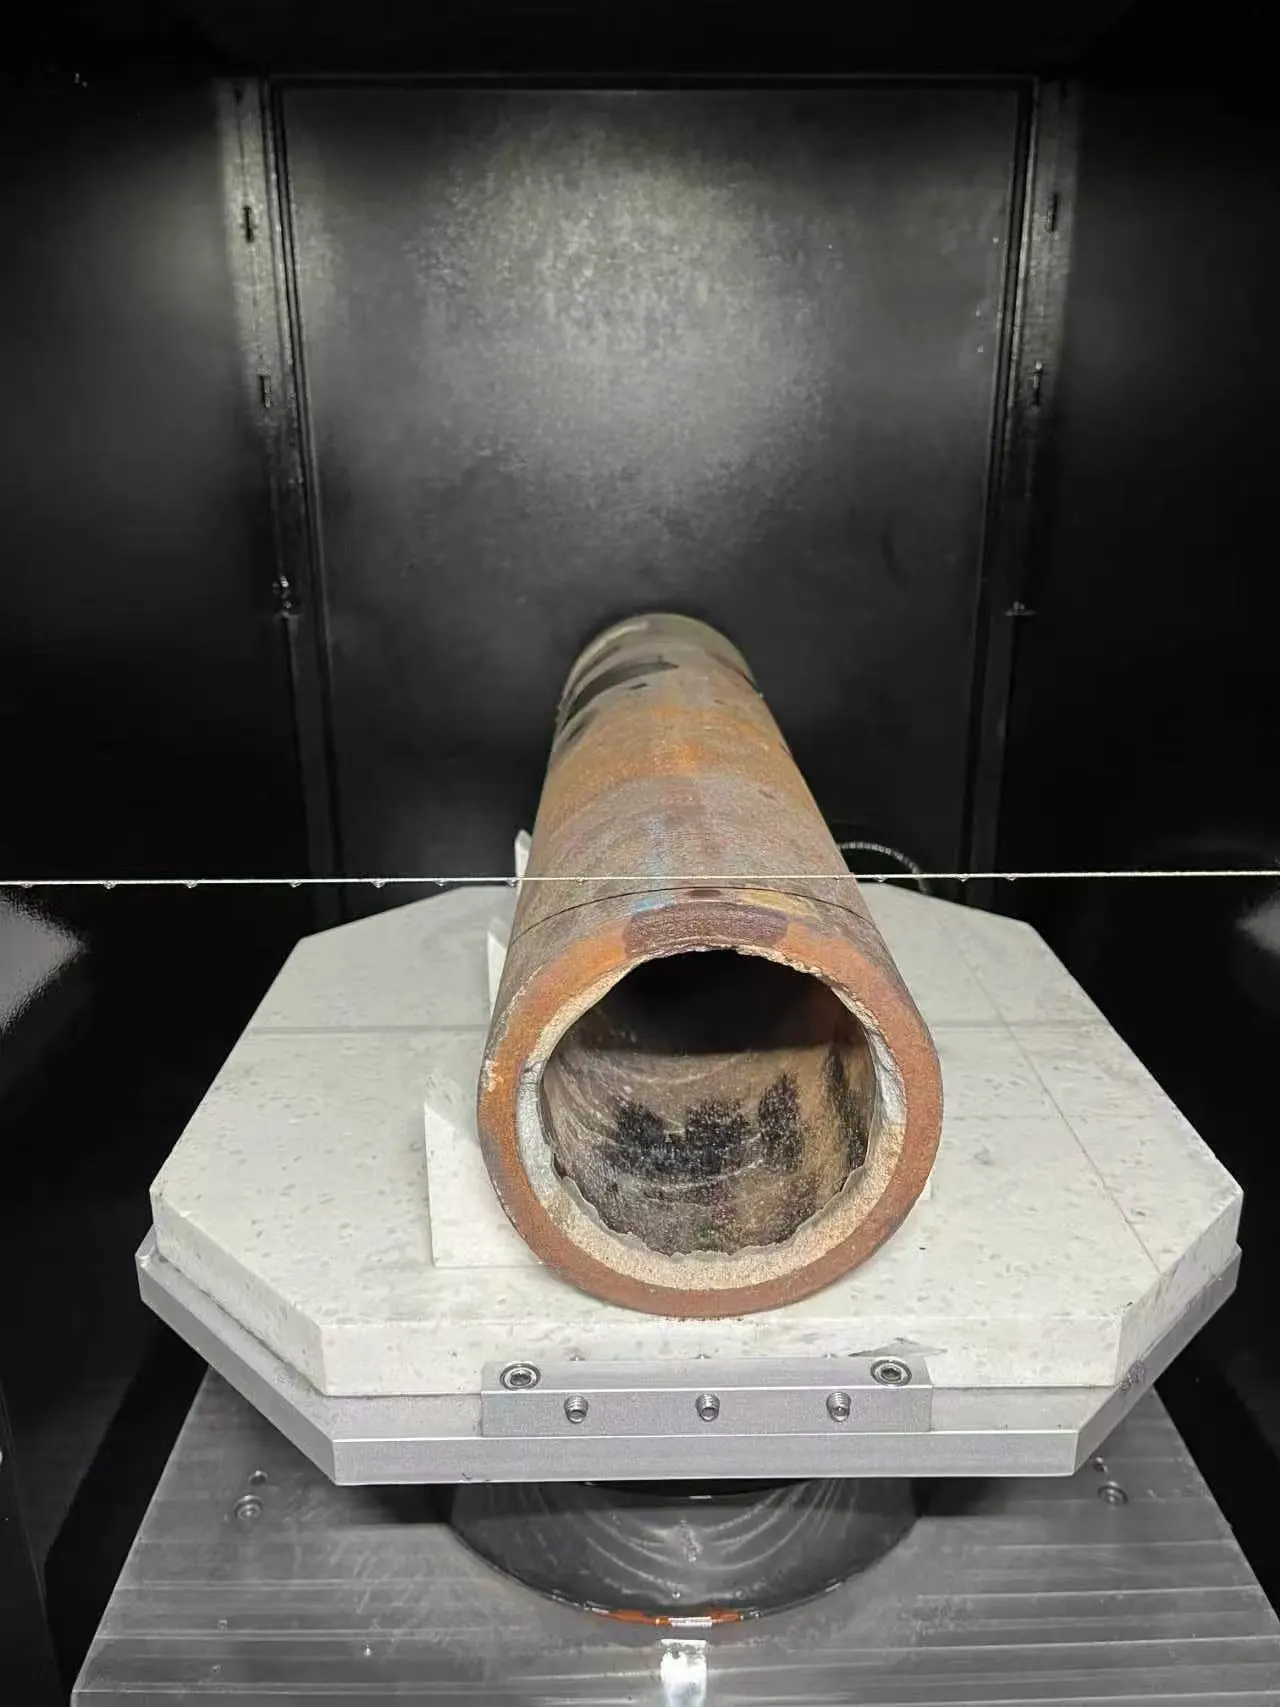
| 工件尺寸 | 500.0 毫米 (L) × Ø120.0 mm |
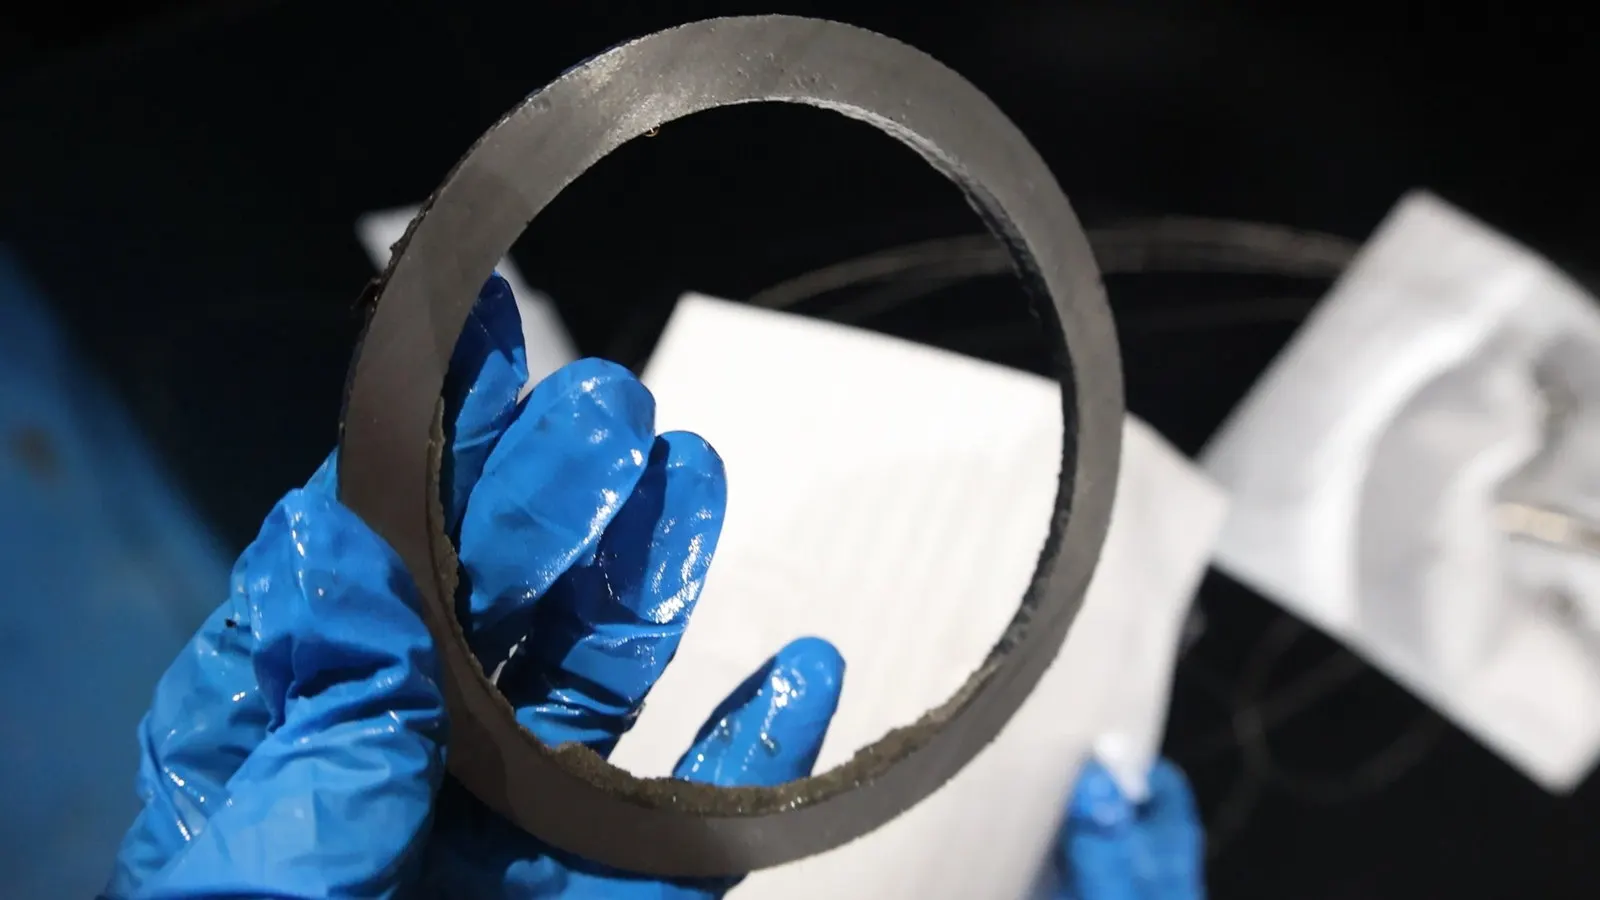
| Target slice dimensions | 10.0 毫米 (L) × Ø120.0 mm |
Ductile iron combines relatively high strength with a degree of toughness. Its structure consists of a metal matrix with spheroidal graphite nodules, and the difference in machinability between the matrix and the graphite phase can produce local variation in cutting behaviour along the kerf.
2. 设备与线材选择
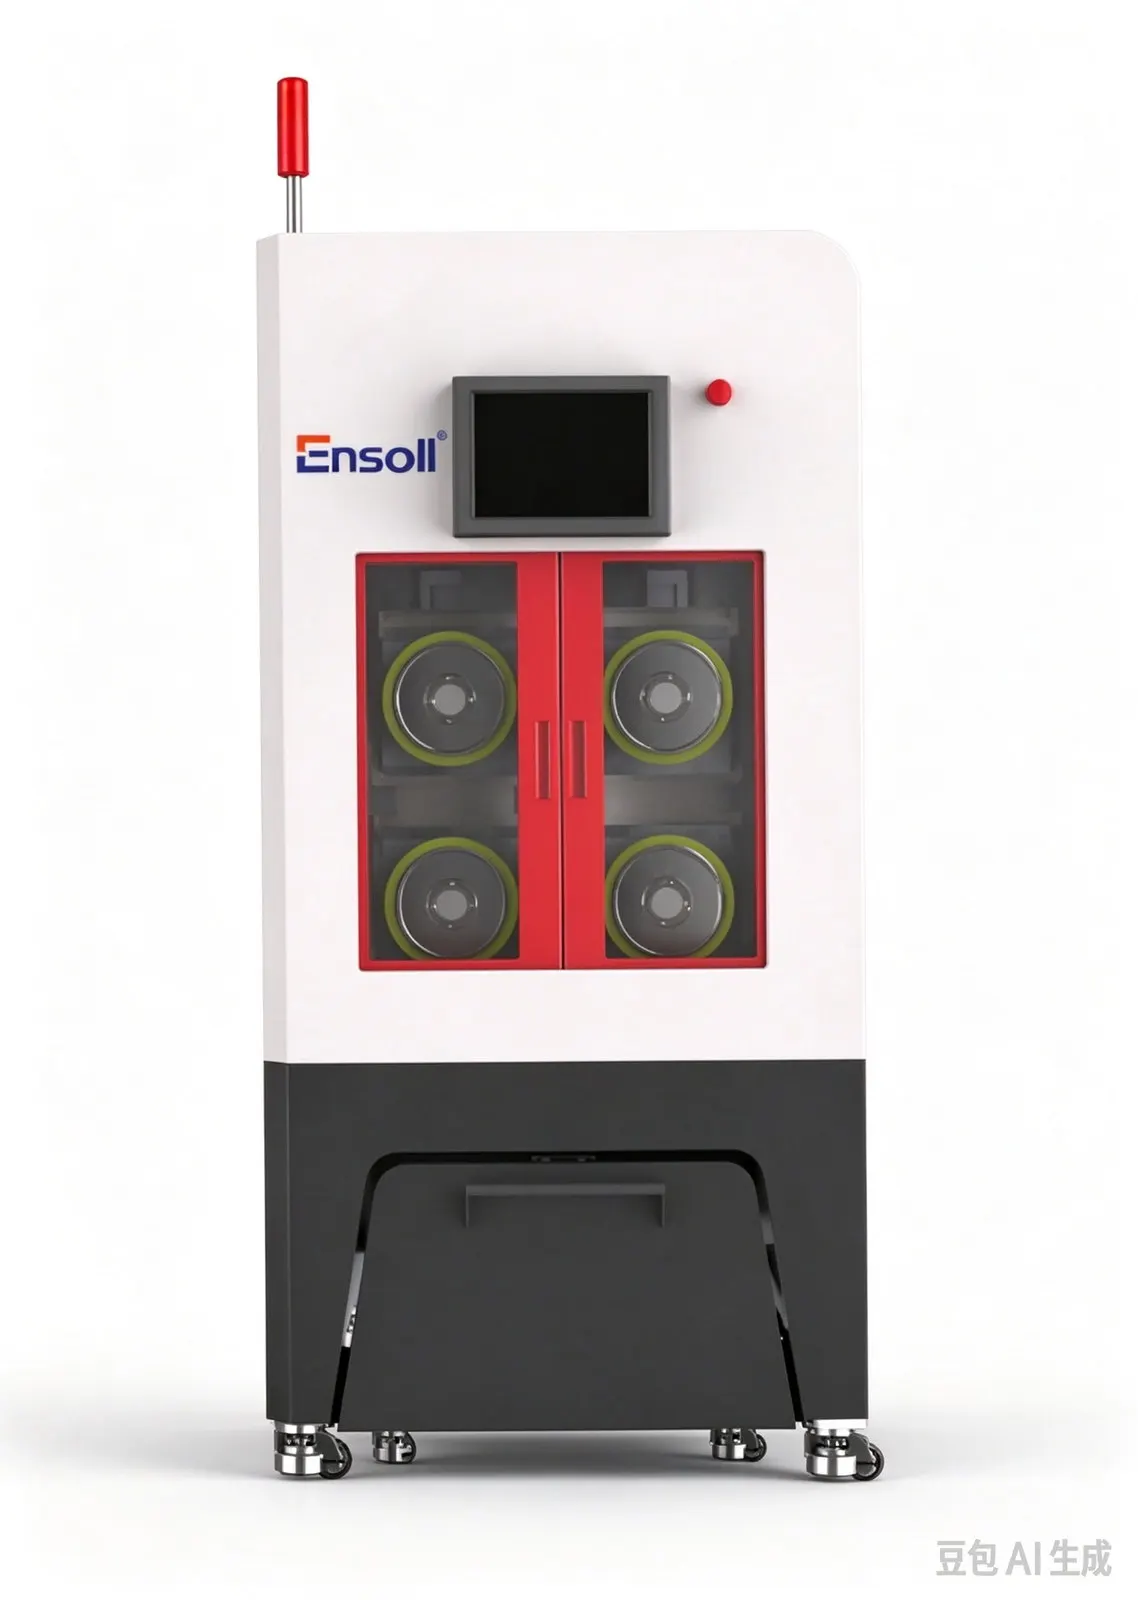
Equipment: ESG400-4T(英语:ESG400-4T). In view of the characteristics of ductile iron and the requirement to slice at a 10 mm thickness, Ensoll selected the ESG400-4T ring diamond wire cutting system with a matched cutting feed. The machine maintains a stable wire trajectory and slice dimensional accuracy.
冷却液: 油基切割. 切削油用作冷却和润滑介质. It continuously lubricates and cools the contact zone between the diamond wire and the ductile iron and carries away part of the heat and cutting debris generated during cutting, reducing the effect of friction-heat accumulation and debris build-up on the machining condition. Controlled oil supply helps maintain a stable cutting zone.
线材: 全镀层. 选择了全镀层金刚石线, with the diamond abrasive grains bonded to the wire core by electroplating. The plated bond improves grain adhesion and distribution uniformity, so the wire maintains a consistent grinding capability and material removal behaviour during cutting. This reduces grain pull-out and wire wear, which matters for a metal workpiece of this section size.
3. 切割方法与设备优势
龙门式切割结构. 龙门结构提供高整体刚性和运行稳定性, which reduces the effect of machine vibration and structural deformation on the wire trajectory and keeps the cut stable. This limits the influence of changes in cutting load on slice position and dimensional accuracy in the ductile iron. 该机配备有雾气抽排系统,可及时去除切割过程中产生的雾气.
智能张力控制. 系统根据切割条件实时调节金刚石线张力,并支持恒张力和变张力模式, 保持线材稳定运转. 良好匹配的张力控制可减少线轨迹的波动,限制局部不均匀受力及因张力变化引起的断线风险, reducing the occurrence of slice defects.
断线记忆. 如果金刚石线断裂或机器异常停止, 系统自动记录当前加工位置及相关操作状态. 更换线材后, 从记录的位置继续切割, reducing dimensional deviation and material loss from re-positioning and repeat machining. This improves the continuity of ductile iron slicing.
Large workpiece capacity and high-speed cutting. The ESG400-4T provides a large effective working envelope, accommodating ductile iron workpieces of substantial section size. The ring diamond wire runs in continuous circulation, and wire speed can reach three to four times that of conventional wire-cut machines, which raises material removal efficiency while keeping the cut stable.
4. 工艺参数与冷却方法
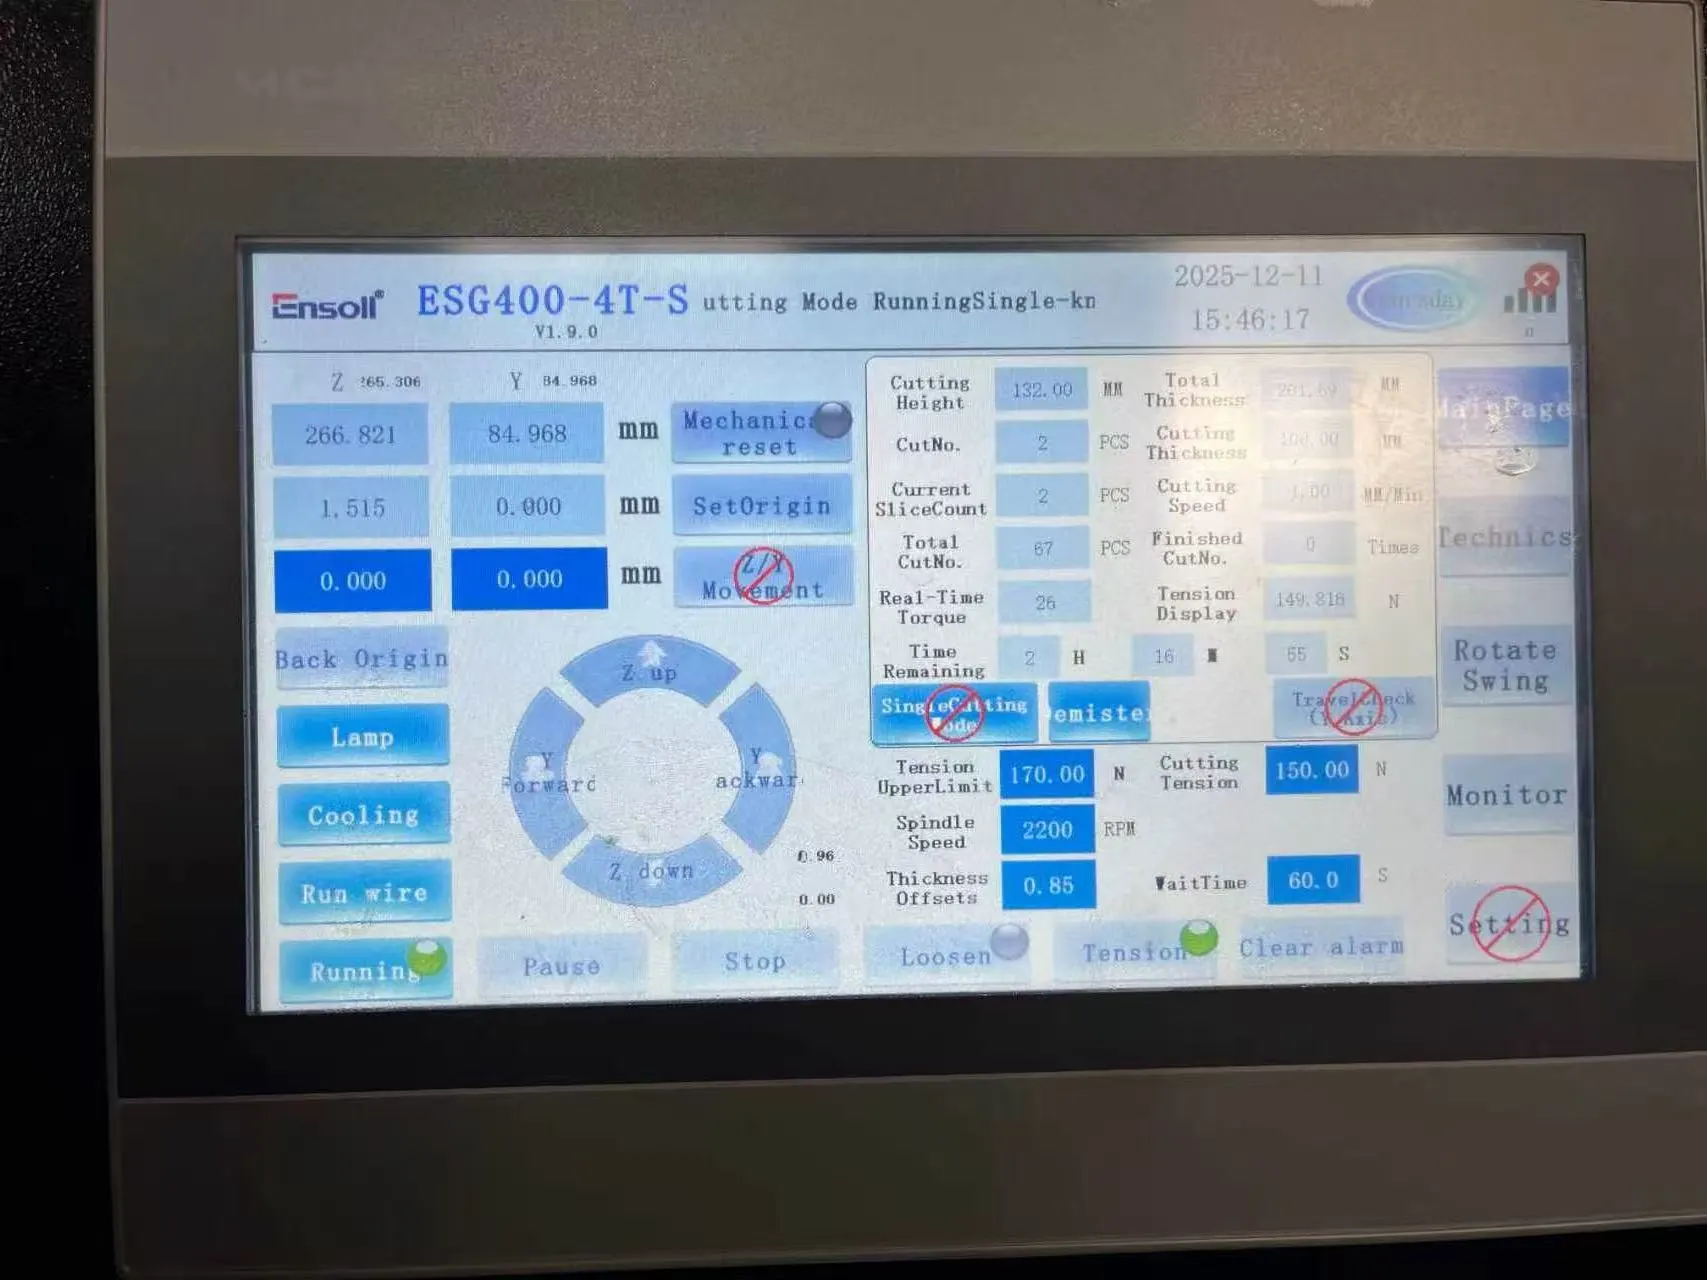
| 参数 | 数值 |
|---|---|
| 线径 (毫米) | 0.80 × 2600 |
| 线速 (毫米/分钟) | 1.5 |
| 切割宽度 (毫米) | 120 |
| 导丝张力 (N) | 150 |
| 导丝速度 (米/秒) | 32 |
| 线弓时间 (秒) | 60 |
5. 切割性能与结果
5.1 TTV测试数据 (单位: 毫米)
总厚度变化 (TTV) 通过九点网格测量, 在真空吸附台上使用双探头厚度测量方法. The measurement was applied to ductile iron slices produced by ring diamond wire cutting. 在测量之前,仪器经过热稳定并使用标准厚度块进行了校准. 标称片厚为 10.000 毫米.
| 样品 | Nine-point thickness readings | T最大值 | T最小值 | TTV |
|---|---|---|---|---|
| S01 | 9.994, 9.997, 10.000 9.996, 10.001, 10.004 9.998, 10.005, 10.008 |
10.008 | 9.994 | 0.014 |
| S02 | 9.990, 9.994, 9.998 9.995, 10.000, 10.003 9.997, 10.004, 10.007 |
10.007 | 9.990 | 0.017 |
| S03 | 9.986, 9.991, 9.995 9.993, 9.998, 10.002 9.996, 10.003, 10.009 |
10.009 | 9.986 | 0.023 |
| S04 | 9.995, 9.998, 10.001 9.997, 10.002, 10.005 9.999, 10.006, 10.010 |
10.010 | 9.995 | 0.015 |
| S05 | 9.992, 9.996, 9.999 9.994, 10.000, 10.004 9.998, 10.005, 10.009 |
10.009 | 9.992 | 0.017 |
| S06 | 9.988, 9.993, 9.997 9.994, 9.999, 10.003 9.996, 10.004, 10.008 |
10.008 | 9.988 | 0.020 |
评估. Nine-point grid measurement was applied to six ductile iron slices. TTV值为 0.014, 0.017, 0.023, 0.015, 0.017 和 0.020 毫米, 批次厚度范围为0.014–0.023毫米, 平均TTV约为 0.018 毫米,在 10.000 毫米标称厚度上. The results confirm good thickness uniformity when slicing a metal workpiece of this section size.
5.2 Thickness Tolerance Data (单位: 毫米)
厚度公差是根据九点厚度数据推导得出的, 使用 10.000 标称厚度为 mm. 在每个测量位置计算正负厚度偏差,并汇总六个样品的结果. 最大正偏差, 确定最大负偏差和总体偏差范围以评估厚度一致性.
| 样品 | 平均厚度 | 厚度偏差 |
|---|---|---|
| S01 | 10.000 | 0.000 |
| S02 | 9.999 | −0.001 |
| S03 | 9.997 | −0.003 |
| S04 | 10.001 | +0.001 |
| S05 | 10.000 | 0.000 |
| S06 | 9.998 | −0.002 |
| 最大正偏差 | — | +0.010 毫米 |
| 最大负偏差 | — | −0.014毫米 |
| 厚度公差带 | — | ±0.012毫米 |
评估. 以公称厚度为基准 10.000 毫米, the six slices showed mean thicknesses of 9.997–10.001 mm, with the batch average close to nominal. Over all measurement points the thickness deviation ranged from −0.014 mm to +0.010 毫米, 最大绝对偏差为 0.014 毫米.
5.3 表面粗糙度 Ra 数据 (单位: 微米)
表面粗糙度 (Ra) was measured by stylus profilometry on the ductile iron slices after ring diamond wire cutting. 代表性测量位置取在切割端面的中心及两侧, 使用针型轮廓仪获取表面轮廓数据, 并在每个位置记录粗糙度参数 Ra.
| 样品 | 中心 | 中左 | 中右 | 平均 Ra |
|---|---|---|---|---|
| S01 | 1.12 | 1.18 | 1.15 | 1.15 |
| S02 | 1.05 | 1.11 | 1.08 | 1.08 |
| S03 | 1.28 | 1.35 | 1.31 | 1.31 |
| S04 | 0.98 | 1.04 | 1.01 | 1.01 |
| S05 | 1.16 | 1.22 | 1.19 | 1.19 |
| S06 | 1.09 | 1.15 | 1.12 | 1.12 |
评估. Mean Ra across the six samples ranged from 1.01 自 1.31 微米, 所有单个读数均在 0.98 和 1.35 微米. The spread across measurement positions on each slice is modest, indicating a consistent surface finish along the cut face on a metal workpiece of this size.
5.4 Edge Condition Data (单位: 微米)
Edge defects were quantified by optical imaging on a toolmaker’s microscope. 测量前清洁样品边缘,并校准仪器的放大倍数和测量刻度. 然后在显微镜下检查切片边缘, identifiable edge defects were located and measured at four points per sample, 并保留最大值.
| 样品 | 点 1 | 点 2 | 点 3 | 点 4 | 麦克斯. edge defect |
|---|---|---|---|---|---|
| S01 | 5.2 | 6.1 | 5.7 | 6.5 | 6.5 |
| S02 | 4.8 | 5.5 | 6.0 | 5.2 | 6.0 |
| S03 | 7.1 | 8.3 | 9.2 | 8.0 | 9.2 |
| S04 | 4.3 | 5.0 | 5.6 | 4.8 | 5.6 |
| S05 | 6.0 | 6.8 | 7.4 | 6.5 | 7.4 |
| S06 | 5.4 | 6.2 | 6.8 | 5.9 | 6.8 |
评估. Toolmaker’s microscope inspection of the six ductile iron slices gave maximum edge defect values of 6.5, 6.0, 9.2, 5.6, 7.4 和 6.8 微米, 总体最大值为 9.2 微米. S04 showed the best edge integrity and S03 the largest defect at 9.2 微米.
6. 结论
The good results obtained in this high-precision slicing trial of ductile iron stemmed mainly from the combined effect of a purpose-built cutting machine, the cooling and lubrication method, and correctly matched process parameters. Ductile iron has relatively high strength and a degree of toughness, and its structure consists of a metal matrix with spheroidal graphite. During ring diamond wire cutting, the difference between the matrix and the graphite phase can cause local variation in cutting behaviour, which places particular demands on machine rigidity and parameter matching.
Equipment. An ESG400-4T ring diamond wire cutting system was used. The machine provides a large effective working envelope for larger workpieces and a high-rigidity structure that reduces the effect of vibration and structural deformation on the wire trajectory. The ring diamond wire runs in continuous circulation at speeds well above conventional wire-cut machines, which raises removal efficiency without sacrificing cut stability.
冷却与润滑. 切割油被用作冷却和润滑介质. It continuously lubricates and cools the wire–workpiece contact zone, reduces friction at the cutting interface, and carries away part of the cutting heat and debris, improving conditions in the cutting zone. For a material with the strength and toughness of ductile iron, effective lubrication is essential to consistent surface finish.
工艺参数. 导丝速度, feed rate and other key parameters were matched to the properties of ductile iron and to the 10 mm slice requirement. Coordinating wire speed with workpiece feed keeps material removal steady and avoids localised increases in cutting load from excessive feed, or unstable cutting from mismatched parameters.
总体. Taken together with slice dimensional accuracy, 表面粗糙度 (Ra) and edge quality, the combination of the ESG400-4T ring diamond wire machine, oil-based cooling and lubrication, and appropriately matched cutting parameters achieves a well-matched process for ductile iron. The results support ring diamond wire cutting as a practical route for precision slicing of ductile iron at this section size.