使用金刚石线环进行磁性材料精密切割: 2 毫米 测试数据
Sample testing for a European client (Company P) · Ring diamond wire cutting process
概述
This report documents precision slicing of magnetic material using a ring diamond wire cutting system. The evaluation covers equipment and wire selection, cutting methodology, 工艺参数, and the resulting thickness uniformity, 尺寸精度, surface quality and edge integrity of the sliced parts. Test results indicate that a gantry-type ring diamond wire machine, oil-based cooling and lubrication, and appropriately matched process parameters deliver stable, high-precision slicing of magnetic material.
1. Test Specimen
| 参数 | 数值 |
|---|---|
| 材料 | Magnetic material |
| 硬度 | approx. 6–7 Mohs |
| 工件尺寸 | 60 mm × 26.0 mm × 3.0 毫米 |
| Target slice dimensions | 2.0 mm × 26.0 mm × 3.0 毫米 |
2. 设备与线材选择
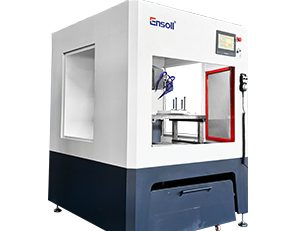
Equipment: ESO-GM. In view of the hard-brittle characteristics of magnetic material and the requirement to slice at a 2 mm thickness, Ensoll selected the ESO-GM gantry-type ring diamond wire cutting system with a top-down vertical feed. The gantry configuration maintains a stable wire trajectory and slice dimensional accuracy.
冷却液: oil-based cutting. 切削油用作冷却和润滑介质. It improves lubrication and heat dissipation in the contact zone between the diamond wire and the magnetic material, reduces friction resistance and localised heat accumulation during cutting, and limits fluctuation in cutting load and its effect on the material. This helps suppress chipping, micro-cracking and surface damage.
线材: fully plated. A fully plated diamond wire was selected. The plated construction improves the bonding strength between the diamond abrasive grains and the wire core and provides a more uniform grain distribution. This sustains a continuous and stable material removal rate, reduces grain pull-out and wire wear, and contributes to lower chipping, micro-cracking and surface damage when slicing magnetic material.

3. Cutting Method and Equipment Advantages
Gantry cutting configuration. The gantry structure provides high overall rigidity and running stability. The top-down vertical feed helps keep the diamond wire trajectory stable and reduces the influence of changes in cutting force on kerf position and dimensional accuracy in the magnetic material. The machine is equipped with a mist-extraction system that promptly removes mist generated during cutting.
智能张力控制. 系统根据切割条件实时调节金刚石线张力,并支持恒张力和变张力模式, 保持线材稳定运转. 稳定的线张力减少切割轨迹的波动,限制局部不均匀受力以及因张力变化导致的线断裂风险, 从而减少磁性材料的缺陷.
断线记忆. 如果金刚石线断裂或机器异常停止, 系统自动记录当前加工位置及相关操作状态. 更换线材后, 从记录的位置继续切割, 减少因重新定位和重复加工造成的尺寸偏差和材料损失. 这提高了磁性材料切割的连续性并降低重复切割的风险.
高刚性一体成型铸铁机架. The one-piece cast iron frame provides high structural stiffness and vibration resistance, reducing the effect of machine vibration and structural deformation on the wire trajectory during machining. For a hard-brittle material such as magnetic material, the high-rigidity frame helps damp vibration and fluctuation in cutting force during the cut and keeps the diamond wire running stably.
4. Process Parameters and Cooling Method
| 参数 | 数值 |
|---|---|
| 线径 (毫米) | 0.35 × 1880 |
| Wire traverse speed (毫米/分钟) | 2 |
| 切割宽度 (毫米) | 60 |
| 导丝张力 (N) | 140 |
| 导丝速度 (米/秒) | 26 |
| Wire bow time (秒) | 60 |

5. Cutting Performance and Results

5.1 TTV测试数据 (单位: 毫米)
总厚度变化 (TTV) was measured using a nine-point grid, dual-probe thickness gauging method on a vacuum-chuck stage. The measurement was applied to magnetic material slices produced by ring diamond wire cutting. Before measurement the instrument was thermally stabilised and calibrated against a standard thickness block. 标称片厚为 2.000 毫米.
| 样品 | Nine-point thickness readings | T最大值 | T最小值 | TTV |
|---|---|---|---|---|
| S01 | 1.992, 1.996, 1.998 1.995, 2.000, 2.003 1.997, 2.004, 2.006 |
2.006 | 1.992 | 0.014 |
| S02 | 1.988, 1.993, 1.997 1.995, 2.001, 2.004 1.999, 2.006, 2.008 |
2.008 | 1.988 | 0.020 |
| S03 | 1.985, 1.990, 1.994 1.992, 1.998, 2.002 1.996, 2.004, 2.009 |
2.009 | 1.985 | 0.024 |
| S04 | 1.994, 1.997, 2.000 1.996, 2.001, 2.004 1.999, 2.005, 2.007 |
2.007 | 1.994 | 0.013 |
| S05 | 1.989, 1.994, 1.997 1.993, 1.999, 2.003 1.996, 2.005, 2.010 |
2.010 | 1.989 | 0.021 |
Assessment. Nine-point grid measurement was applied to five magnetic material slices. TTV values were 0.014, 0.020, 0.024, 0.013 和 0.021 毫米, spanning 0.013–0.024 mm across the batch, with a mean TTV of approximately 0.018 mm on a 2.000 mm nominal thickness. The results confirm good thickness uniformity in magnetic material slicing.
5.2 Thickness Tolerance Data (单位: 毫米)
Thickness tolerance was derived from the nine-point thickness data, using 2.000 标称厚度为 mm. The positive and negative thickness deviation were calculated at each measurement position and the results from all five samples were aggregated. 最大正偏差, maximum negative deviation and overall deviation range were then determined to evaluate thickness consistency.
| 样品 | Mean thickness | 厚度偏差 |
|---|---|---|
| S01 | 1.999 | −0.001 |
| S02 | 1.999 | −0.001 |
| S03 | 1.997 | −0.003 |
| S04 | 2.000 | 0.000 |
| S05 | 1.998 | −0.002 |
| 最大正偏差 | — | +0.010 毫米 |
| 最大负偏差 | — | −0.015 毫米 |
| 厚度公差带 | — | ±0.0125 毫米 |
Assessment. 以公称厚度为基准 2.000 毫米, 五片样品的平均厚度为 1.997–2.000 毫米, 整个批次的平均偏差很小. 在所有测量点上厚度偏差范围为 −0.015 毫米 到 +0.010 毫米, 最大绝对偏差为 0.015 毫米.
5.3 表面粗糙度 Ra 数据 (单位: 微米)
表面粗糙度 (Ra) 通过在环形金刚线切割后的磁性材料片上使用针型轮廓仪测量. 代表性测量位置取在切割端面的中心及两侧, 使用针型轮廓仪获取表面轮廓数据, 并在每个位置记录粗糙度参数 Ra.
| 样品 | 中心 | 中左 | 中右 | 平均 Ra |
|---|---|---|---|---|
| S01 | 0.52 | 0.56 | 0.49 | 0.52 |
| S02 | 0.48 | 0.53 | 0.50 | 0.50 |
| S03 | 0.61 | 0.66 | 0.58 | 0.62 |
| S04 | 0.46 | 0.51 | 0.48 | 0.48 |
| S05 | 0.55 | 0.59 | 0.53 | 0.56 |
Assessment. 五个样品的平均 Ra 范围为 0.48 自 0.62 微米, 所有单个读数均在 0.46 和 0.66 微米. The narrow spread across the three measurement positions on each slice indicates a uniform surface finish along the cut face.
5.4 边缘崩缺数据 (单位: 微米)
Edge chipping was quantified by optical imaging on a toolmaker’s microscope. Specimen edges were cleaned before measurement and the magnification and measurement scale of the instrument were calibrated. The slice edge was then inspected under the microscope, identifiable chipping defects were located and measured at four points per sample, and the maximum value was retained.
| 样品 | Point 1 | Point 2 | Point 3 | Point 4 | 麦克斯. chipping |
|---|---|---|---|---|---|
| S01 | 4.2 | 5.1 | 4.8 | 5.6 | 5.6 |
| S02 | 3.8 | 4.6 | 5.2 | 4.4 | 5.2 |
| S03 | 5.6 | 6.8 | 7.5 | 6.2 | 7.5 |
| S04 | 3.5 | 4.1 | 4.6 | 3.9 | 4.6 |
| S05 | 4.9 | 5.7 | 6.3 | 5.2 | 6.3 |
Assessment. Toolmaker’s microscope inspection of the five magnetic material slices gave maximum chipping values of 5.6, 5.2, 7.5, 4.6 和 6.3 微米, with an overall maximum of 7.5 微米. S04 showed the best edge integrity and S03 the largest chipping at 7.5 微米.

6. 结论
The good results obtained in this high-precision slicing trial of magnetic material stemmed mainly from the combined effect of a purpose-built cutting machine, the cooling and lubrication method, and correctly matched process parameters. Magnetic material is relatively hard with a degree of brittleness. During ring diamond wire cutting the abrasive grains act continuously on the material surface, and material removal is affected by cutting load, wire running condition and the machining parameters.
Equipment. An ESO-GM gantry-type ring diamond wire cutting system was used. The gantry structure provides high overall rigidity and running stability and gives reliable mechanical support for workpiece clamping and continuous wire travel. Stable motion and feed control keep the diamond wire on the programmed path throughout the cut.
冷却与润滑. Cutting oil was used as the cooling and lubricating medium. During cutting the diamond wire remains in continuous contact with the workpiece and the abrasive grains grind the material continuously, generating friction heat in the contact zone. Cutting oil improves lubrication at the cutting interface, carries away part of the cutting heat, and reduces friction between the wire and the workpiece, which helps limit thermal effects and edge damage.
Process parameters. 导丝速度, feed rate and other key parameters were matched to the hardness, brittleness and target slice thickness of the magnetic material. Parameters were set to maintain stable wire travel and continuous material removal, avoiding feed rates high enough to raise cutting load, or a mismatch between wire speed and feed rate that would degrade slice quality.
总体. Taken together with slice dimensional accuracy, thickness tolerance, 表面粗糙度 (Ra) and cut-edge quality, the combination of the ESO-GM gantry cutting machine, oil-based cooling and lubrication, and appropriately matched process parameters allows ring diamond wire cutting to meet the precision slicing requirements for this magnetic material.