광학 유리 절단: 다이아몬드 와이어 톱 vs 레이저
광학 유리 가공은 항공우주, 광자학 등 산업의 요구를 충족하기 위해 서브 마이크로 정밀도를 필요로 합니다, 광자학, 그리고 소비자 전자공학. 와 함께 끝없는 다이아몬드 와이어 톱 and laser cutting emerging as dominant technologies, manufacturers face a critical choice. This guide analyzes both methods across 7 key parameters to help you make data-driven decisions.
- Diamond wire saw cutting removes material by diamond grit abrasion (wire 0.1-0.3 밀리미터, 5-30 엠/초) and holds +/-0.02-0.03 mm tolerance; laser cutting vaporizes material and typically holds +/-0.05 밀리미터.
- Cut quality favors the wire: under 10 micrometers edge chipping and Ra 0.2-0.5 마이크로미터, versus a 20-50 micrometer heat-affected zone and Ra 0.5-2 micrometers for laser.
- Efficiency favors the laser: 40-60 wafers/hour with 5-10 minute setup versus 20-30 wafers/hour and 15-30 minutes for the wire saw — but laser kerf is narrower at 0.05-0.1 mm versus 0.15-0.3 밀리미터.
- Cost profile: wire saw $50K-150K investment with $0.10/meter consumables and low maintenance; laser $100K-300K with $20/hour gas assist and higher optics maintenance.
- 경험 규칙: wire saw for glass thicker than 3 밀리미터, optical-grade edges below Ra 0.5 micrometers and heat-sensitive coatings; laser for thin-glass prototyping and complex contours.
1. Endless Diamond Wire Saw Cutting
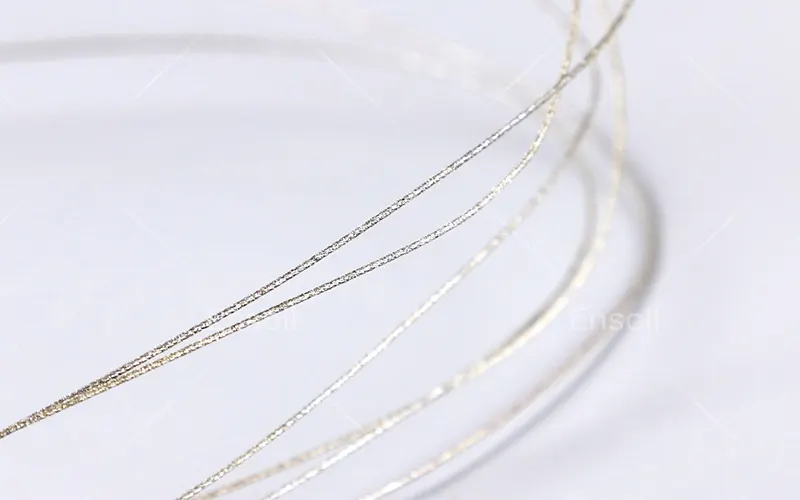
A closed-loop system using a diamond-coated wire (typically 0.1-0.3mm diameter) running at 5-30 엠/초. The abrasive action provides:
– Material Removal Mechanism: Micro-chipping through diamond grit abrasion
– Typical Tolerance: ±0.03mm for standard cuts, ±0.02mm with advanced controls
– Best Suited For: Thick 광학 유리 (>1밀리미터), curved cuts, and brittle materials like SCHOTT B270 .
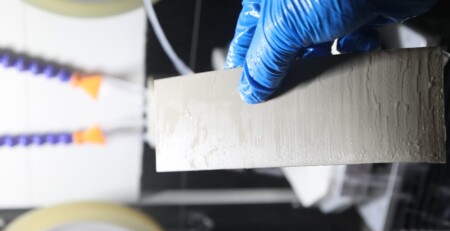
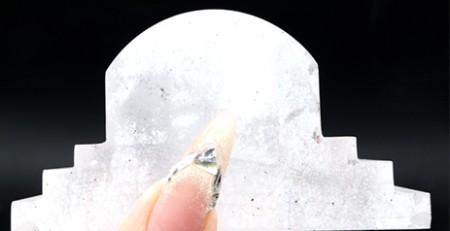
절단 디스플레이:
2. 레이저 커팅
A non-contact method using focused laser beams (usually CO₂ or ultrafast lasers):
– Material Removal Mechanism: Vaporization/melting through localized heating
– Typical Tolerance: ±0.05mm for standard systems
– Best Suited For: Thin glass (<3밀리미터), complex geometries, and rapid prototyping
Head-to-Head Comparison
1. Cutting Quality
| 매개변수 | 끝없는 다이아몬드 와이어 톱 | 레이저 커팅 |
| 엣지 치핑 | <10µm with optimized feed rate | 20-50µm thermal affected zone |
| 표면 거칠기 | Ra 0.2-0.5µm | Ra 0.5-2µm |
| 하부 손상 | Minimal micro-cracks | Potential micro-fractures |
Key Insight: For camera lenses and prisms requiring optical-grade finishes, wire saws provide superior edge integrity.
2. Material Versatility
– Wire Saws handle:
– High-hardness glasses (예), Corning Gorilla Glass 3)
– Composite materials (glass-ceramics like Zerodur)
– Temperature-sensitive coatings
– Lasers struggle with:
– Thick borosilicate (>5밀리미터) due to heat accumulation
– UV-transmitting glasses prone to thermal stress
- Production Efficiency
| Metric | Wire Saw (300mm/s) | 레이저 (500mm/s) |
| Throughput | 20-30 wafers/hour | 40-60 wafers/hour |
| Setup Time | 15-30 분 | 5-10 분 |
| 절삭 폭 | 0.15-0.3밀리미터 | 0.05-0.1밀리미터 |
Trade-off: Lasers offer faster processing but waste more material through wider kerf.
5 Decision-Making Factors
1. Part Thickness
– Choose Wire Saw If:
절단 >3mm optical glass (예), telescope mirrors)
Keyword Tip: “thick 광학 유리 절단 solution”
2. Tolerance Requirements
Wire saws maintain tighter tolerances for:
– Prism angle control (±15 arcseconds)
– Wafer-level optics uniformity
3. 비용 고려사항
| Cost Factor | Wire Saw | 레이저 |
| Initial Investment | $50K-$150K | $100K-$300K |
| Consumables | $0.10/meter diamond wire | $20/hour gas assist |
| 유지보수 | Lower (mechanical parts) | Higher (optics cleaning) |
- 열 민감도
Laser cutting risks:
– Stress birefringence in polarizing elements
– Annealing point distortion in phosphate glasses
5. Post-Processing Needs
Wire-sawn parts often require:
– 25% less polishing time vs. laser-cut surfaces
– No stress relief annealing
결론: When to Select Each Method
Opt for Endless Diamond Wire Saw When:
✓ Cutting thickness >3밀리미터
✓ Needing optical-grade edges (Ra<0.5μm의)
✓ Processing heat-sensitive coatings
Choose Laser Cutting When:
✓ Rapid prototyping of thin glass
✓ Complex contours with <0.1mm kerf
✓ Budget allows for higher operational costs
Pro Tip: Request sample cuts from suppliers—compare edge quality under 200x microscopy to validate claims.
자주 묻는 질문
Should I choose a diamond wire saw or laser for optical glass cutting?
Choose the wire saw when cutting glass thicker than 3 밀리미터, when you need optical-grade edges (Ra below 0.5 마이크로미터), or when processing heat-sensitive coatings and hard glasses like Corning Gorilla Glass 3. Choose laser for rapid prototyping of thin glass under 3 mm and complex contours needing a kerf below 0.1 밀리미터.
Does laser cutting damage optical glass?
It can. The localized heating creates a 20-50 micrometer thermal affected zone, risks micro-fractures below the surface, and can cause stress birefringence in polarizing elements or annealing-point distortion in phosphate glasses. Wire saw cutting is a cold abrasive process and avoids these thermal risks.
Which method costs more, wire saw or laser?
Laser costs more on both fronts: $100K-300K initial investment versus $50K-150K for a wire saw, plus about $20 per hour in gas assist versus roughly $0.10 per meter of diamond wire. Laser systems also demand more maintenance, mainly optics cleaning.
Which method is more precise?
The diamond wire saw: +/-0.03 mm standard and +/-0.02 mm with advanced controls, versus +/-0.05 mm for standard laser systems. Wire saws also hold prism angle control within +/-15 arcseconds, which is why they dominate prisms and wafer-level optics.
Ensoll 엔지니어링 팀의 검토.