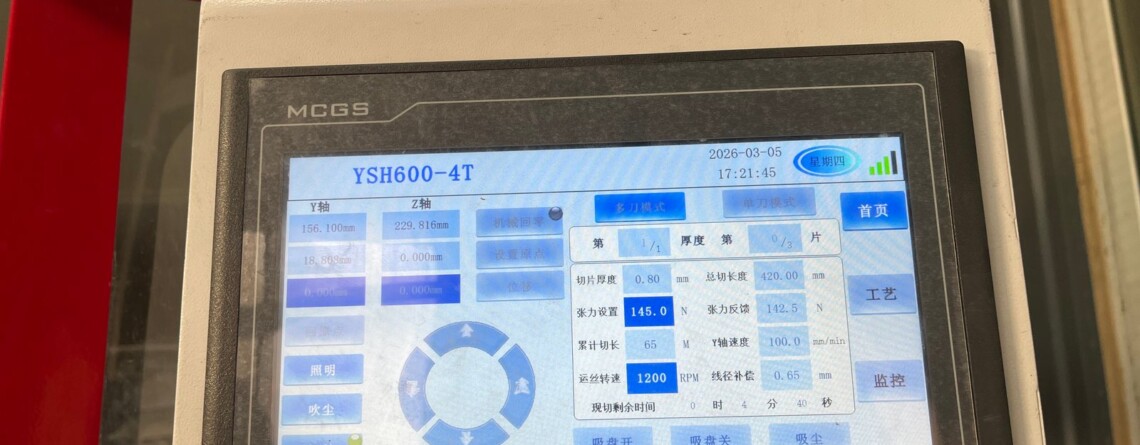
PMI 泡沫切割参数: 金刚线环设置参考
抽象: This reference sheet lists the process window validated in Ensoll’s PMI
(polymethacrylimide) structural foam slicing test on an ESH600-4T horizontal
金刚线锯机: 一个 0.60 x 3460 mm fully coated
金刚石线环, 100 mm/min wire travel speed, 145 N wire tension, 25 m/s wire speed,
60 s wire-bow tensioning time, 17 N·m cutting load and 400 mm cutting width, with dry cutting. It explains
what each parameter does on a cellular foam, which way to move it when a defect appears, and how to establish a
starting set for a new foam grade or slice thickness.
关键要点
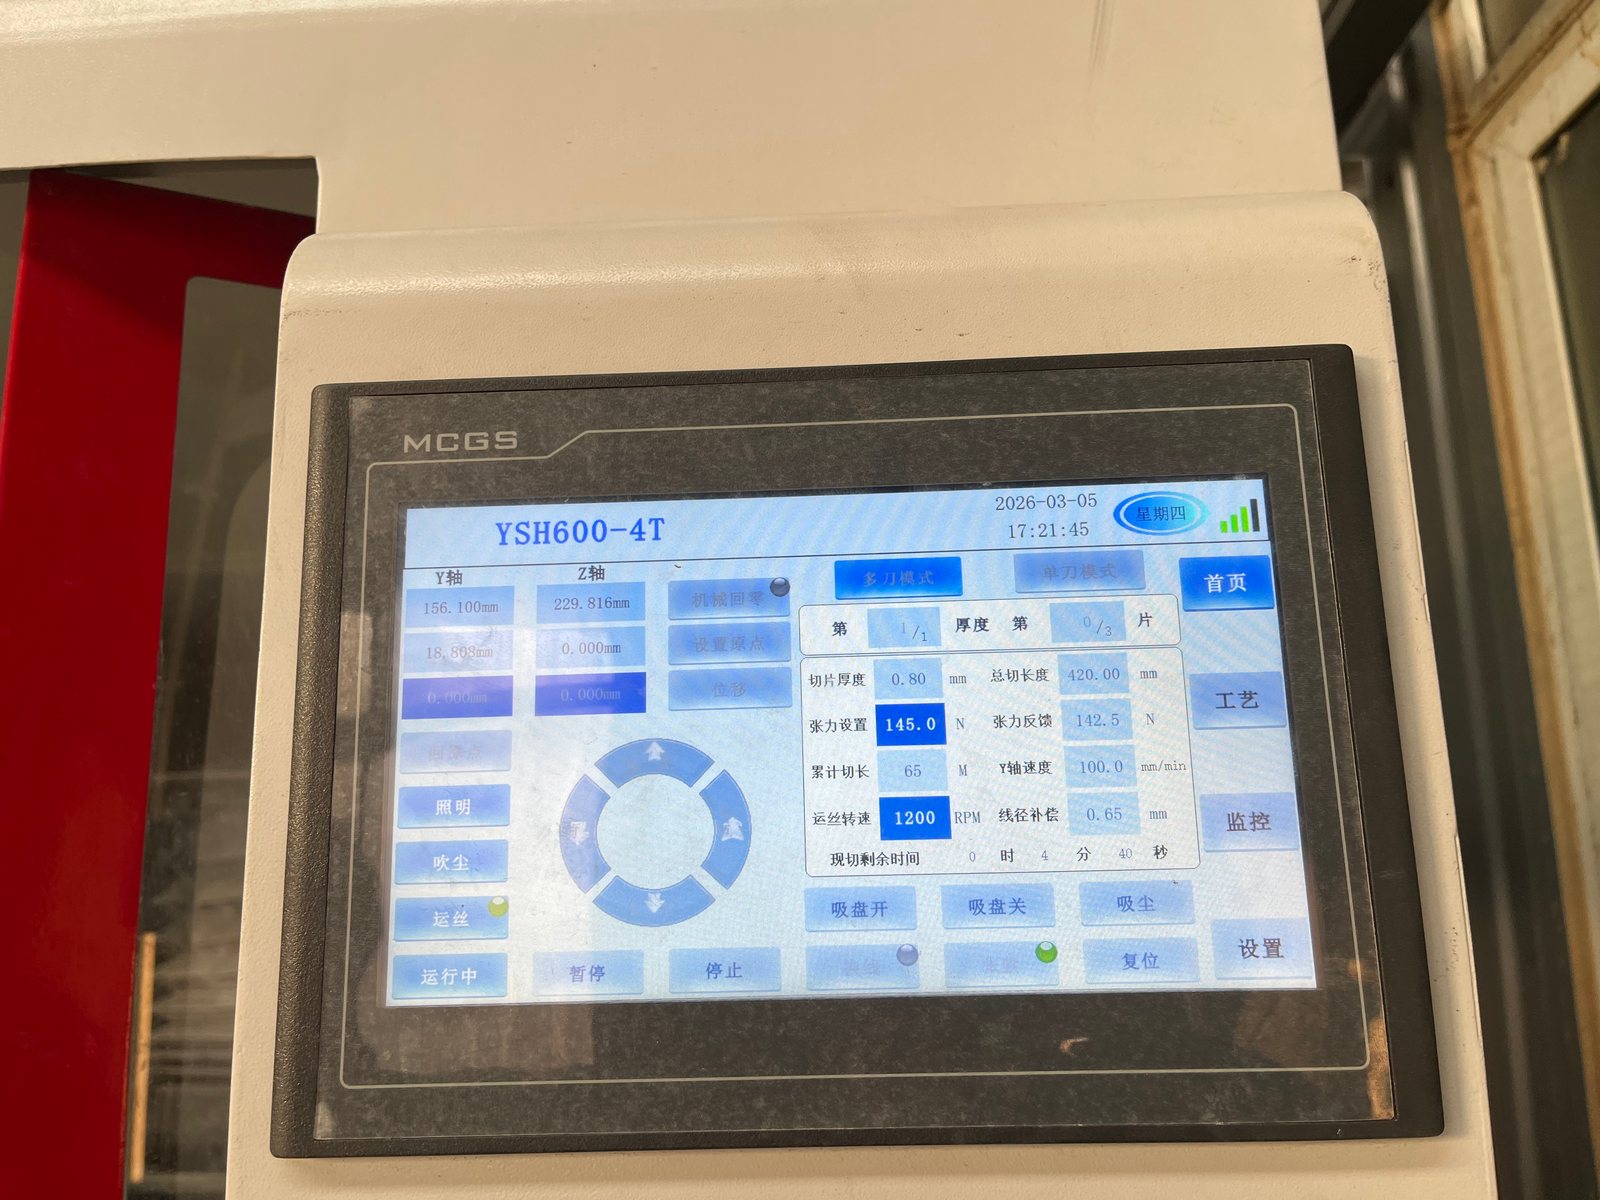
- Validated window for 0.8 mm PMI foam slices on an ESH600-4T: 0.60 x 3460 毫米全涂层线圈, 100 mm/min feed, 400 mm cutting width, 145 N tension, 25 m/s wire speed, 60 s wire-bow time, 17 N·m load, dry cutting.
- PMI foam fails by compression and tearing of the cell skeleton, not by brittle fracture, so feed rate – the load-setting parameter – is the first thing to reduce when a defect appears.
- Dry cutting is the default for PMI foam: coolant would enter the cells and would have to be cleaned and dried out afterwards.
- The load readout is a monitor, not a setting; a rising load trace during a cut is the earliest warning that a parameter has drifted out of band.
- This window produced TTV 0.013-0.050 毫米 (mean 0.036 毫米), thickness tolerance +/-0.043 毫米, average Ra 0.68-0.82 um and maximum chipping 5.5-7.1 um.
Why PMI Foam Needs Its Own Parameter Set
PMI foam is a low-density structural foam with a uniform cellular structure and good specific strength and
specific stiffness. Under a diamond wire it does not behave like a dense material: the abrasive grains act on the
foam skeleton, and the failure mode at excessive load is compression and tearing of the cells rather than clean
shearing. That is why parameters that work on a dense thermoplastic cannot simply be copied across. 这
validated PMI window below was established by matching machine structure, wire, cutting method and parameters to
the cellular structure of the material.
Validated Parameter Window for 0.8 mm PMI Foam Slices
| 参数 | 数值 |
|---|---|
| Wire diameter x loop length (毫米) | 0.60 x 3460 |
| Wire travel speed / 进给速度 (毫米/分钟) | 100 |
| 切割宽度 (毫米) | 400 |
| 导丝张力 (N) | 145 |
| 导丝速度 (米/秒) | 25 |
| Wire-bow tensioning time (秒) | 60 |
| 切割负荷 (N·m) | 17 |
| 冷却方式 | Dry cutting |
PMI foam slicing test
Workpiece conditions for this window: PMI foam at approximately MH 2 硬度, workpiece
400 mm x 400 mm x 50 毫米, target slice 400 mm x 400 mm x 0.8 毫米.
What Each Parameter Does
Wire diameter and loop length (0.60 x 3460 毫米)
The wire diameter sets the kerf and the stiffness of the cutting edge. 一个 0.60 mm fully coated wire loop gives a
stable abrasive edge for a 400 mm wide cut while keeping the kerf small. Loop length must match the machine’s
pulley geometry and is fixed by the machine model rather than chosen per job.
Wire travel speed / 进给速度 (100 毫米/分钟)
This is the parameter that governs cutting load most directly, and on foam it is the first one to reduce when a
defect appears. Feed too high and the skeleton takes a large local force; feed too low and the wire polishes
rather than cuts, which raises heat and wear without improving quality. 100 mm/min is the validated value for
0.8 mm slices.
切割宽度 (400 毫米)
The cutting width is the length of wire in contact with the workpiece. It scales the total load and therefore
the machine rigidity and tensioning required. 一个 400 mm contact length on a lightweight foam also raises the risk
of the workpiece moving, which is why the fixture and workpiece support matter as much as the numbers.
导丝张力 (145 N)
Tension keeps the wire straight under load. Too low and the wire bows, so kerf width wanders and the cut face
becomes uneven; too high and the wire and pulleys wear faster and break risk rises. The ESH600-4T uses spring
tensioning with force-sensor feedback, so tension can be held constant or varied with the cutting state, and is
reduced automatically in standby and during wire changes to limit wire fatigue.
导丝速度 (25 米/秒)
Wire speed sets how many abrasive grains pass the interface per second. On a low-density foam the removal rate
is limited by load rather than by abrasive delivery, so raising wire speed alone does not fix a poor cut – it
mostly adds wear. Keep it in the validated band and manage quality through feed and tension.
Wire-bow tensioning time (60 秒)
The tensioning time lets the wire settle into a stable bow before the cut starts. Skipping it leaves the first
millimetres of the cut under different conditions from the rest, which shows up as a thickness step at the entry
edge of a thin slice.
切割负荷 (17 N·m)
The load reading is the process monitor rather than a setting: it is what you watch to confirm that the
combination of feed, tension and wire speed is actually delivering a stable cut. A drifting or rising load during
a cut is the earliest warning that a parameter has moved out of band.
Adjustment Guide: Symptom, 原因, Action
| Symptom | Most likely cause | Action |
|---|---|---|
| Ragged or torn slice edge | Cutting load too high for a cellular foam | Reduce feed rate; verify wire tension before changing wire speed |
| Uneven cut face, wandering kerf | Wire bowing – tension too low | Raise tension toward 145 N and confirm the bow settles before entry |
| Thickness step at the entry edge | Cut started before the wire bow settled | Keep the full 60 s wire-bow tensioning time before feed engages |
| 切片始终厚或薄 | 尺寸偏移, 不是不稳定 | 在机器目标上应用厚度补偿; 不要通过进给来对抗它 |
| 切割过程中负载轨迹上升 | 参数漂移或线材磨损 | 停止, 检查线材状态和负载, 重新建立验证的窗口 |
| 表面抛光而非切割 | 进给速度对于线材速度过低 | 在验证范围内提高进给速度; 检查线材的磨粒状态 |
为新的泡沫或厚度建立参数集
验证窗口是一个起点, 不是普遍答案. PMI等级的密度和孔径不同,
切片厚度会改变被切割部件的刚度. 按此顺序操作:
- 先固定夹具. 在整个区域支撑工件,使线材无法
推动它. 在泡沫上, deflection of the workpiece reads as thickness variation and is easily mistaken for a
parameter problem. - Start from the validated window. 0.60 x 3460 mm wire, 100 mm/min feed, 145 N tension,
25 m/s wire speed, dry cutting. - Cut one slice and measure TTV. Use the same nine-point grid method described in our
TTV measurement guide so results are comparable with the reference data. - Move one parameter at a time. Feed rate first, then tension. Change wire speed only if feed
and tension are already at their limits. - Record the load curve. A stable load trace at the chosen settings is the evidence that the
process, not the operator, is controlling the cut.
Results Achieved with This Window
| Measure | Result across four 0.8 mm slices |
|---|---|
| Total thickness variation (TTV) | 0.013-0.050 毫米, average 0.036 毫米 |
| Thickness tolerance | +/-0.043 mm against 0.800 mm nominal |
| Average surface roughness Ra | 0.68-0.82 um |
| Maximum edge chipping | 5.5-7.1 um |
The thickness data showed a systematic negative offset rather than random scatter – the slices ran thin by
0.031 到 0.043 mm against a 0.800 mm nominal. That is a dimensional-compensation problem, not a stability
problem, and is corrected by adjusting the machine target thickness on the next run. The full measurement set
including all nine-point readings is published in the
PMI foam precision slicing test report.
Related Process Data
The same nine-point methodology applied to a dense thermoplastic, with cutting fluid instead of dry cutting,
is documented in the PEEK precision slicing test. A side-by-side comparison of the two
materials and their parameter sets is in
PEEK vs PMI foam: diamond wire cutting comparison.
常见问题
What cutting parameters were used to slice PMI foam to 0.8 毫米?
线材 0.60 x 3460 毫米, wire travel speed (进给速度) 100 毫米/分钟, cutting width 400 毫米, wire tension 145 N, wire speed 25 米/秒, wire-bow tensioning time 60 s and cutting load 17 N·m, on an ESH600-4T horizontal 金刚线锯机 using dry cutting and a fully coated wire.
Should PMI foam be cut dry or wet?
干. PMI foam is porous, lightweight and prone to absorbing liquids. Dry cutting keeps coolant out of the cells and removes the cleaning and drying steps that follow a wet cut, which helps preserve structural integrity and slice dimensional accuracy. This is the opposite of a dense thermoplastic such as PEEK, which is cut with continuous cutting fluid.
What wire type is used for PMI foam?
A fully coated diamond wire loop. The fully coated build raises grain bonding strength and distribution stability, sustaining continuous cutting capability and reducing the fluctuation caused by wire wear and grain pull-out. See the diamond wire loop product range.
What results did this parameter set achieve?
Four 400 mm x 400 mm PMI foam slices at 0.8 mm nominal thickness gave TTV 0.013-0.050 毫米 (average 0.036 毫米), thickness tolerance +/-0.043 毫米, average Ra 0.68-0.82 um and maximum edge chipping 5.5-7.1 um. Full data is in the PMI foam slicing test report.
What is the first setting to change if the PMI foam edge tears?
Reduce the feed rate. Tearing, local compression and an uneven cut face on a cellular foam are load-driven problems, not speed-driven ones: excessive load compresses the foam skeleton instead of shearing it. Lower the feed first, then re-check wire tension before touching wire speed.
Technical content reviewed by the Ensoll engineering team – a diamond wire loop manufacturer with 10+ 多年生产经验.