用金刚石线环切割PEEK: 精密切片测试
抽象: This article presents a precision slicing test on PEEK (polyether ether ketone) 使用它 金刚石线环. The workpiece was a 200 mm × 60 mm × 60 mm PEEK block provided by European customer H, sliced into 6.5 mm-thick pieces on an Ensoll ESO-GM gantry-type diamond wire loop cutting machine. We report the equipment and wire selection, cutting parameters, cooling strategy, and quantitative quality metrics including Total Thickness Variation (TTV), thickness tolerance, 表面粗糙度 (Ra), and edge chipping. The results show that with a rigid machine, a fully-coated diamond wire loop, continuous coolant, and well-matched parameters, diamond wire loop cutting can hold PEEK slicing to a thickness tolerance of ±0.037 mm, average TTV of 0.085 毫米, Ra below 1 微米, and edge chipping of no more than 6.7 微米.
- 一个 200 mm × 60 mm × 60 mm PEEK block was sliced into 6.5 mm pieces on the Ensoll ESO-GM machine (0.35 mm fully-coated diamond wire loop, 24 m/s wire speed, 150 N tension, 3 mm/min feed).
- Across three slices, TTV stayed within 0.072–0.098 mm (average 0.085 毫米) and thickness tolerance within ±0.037 mm.
- Average surface roughness was 0.80–0.91 μm Ra and maximum edge chipping was 6.7 μm — clean results for a tough thermoplastic that is prone to heat softening and burrs.
- The keys for PEEK are continuous cutting-fluid cooling, high machine rigidity, and conservative feed parameters that keep cutting heat under control.
1. Why PEEK Is a Different Cutting Challenge
The material in this test was PEEK supplied by European customer H, and the machining requirement was high-precision straight slicing. PEEK is a high-performance thermoplastic engineering material with high toughness, 耐磨性, and heat resistance. Its material removal mechanism under diamond wire cutting differs from typical hard and brittle materials such as 光学玻璃 和 技术陶瓷. Because PEEK has a degree of plasticity and toughness, the continuous action of diamond abrasive grains generates cutting heat. If heat dissipation is insufficient or cutting parameters are poorly matched, the machining zone heats up, the material softens locally, and cutting resistance rises — leading to dimensional deviation, edge burrs, and degraded surface quality.
To meet the dimensional stability and surface quality requirements of high-precision straight slicing of PEEK, Ensoll applied a diamond wire loop cutting solution adapted to PEEK’s machining characteristics: a dedicated machine for stable workpiece clamping and smooth wire travel; a matched diamond wire that keeps abrasive removal capability stable; continuous cutting-fluid cooling to carry heat away; and tuned wire speed and feed parameters that keep cutting load and machining temperature within a reasonable window, reducing softening, adhesion, and edge burrs. With equipment, wire, 冷却, and parameters properly matched, the slicing process stays stable and the dimensional accuracy, 厚度一致性, and surface quality of PEEK slices can be effectively controlled.
2. Test Material
材料: PEEK (polyether ether ketone)
硬度: 约 MH 6.5
工件尺寸: 200 mm × 60 mm × 60 毫米
切片尺寸: 6.5 mm × 60 mm × 60 毫米
3. 设备与线材选择
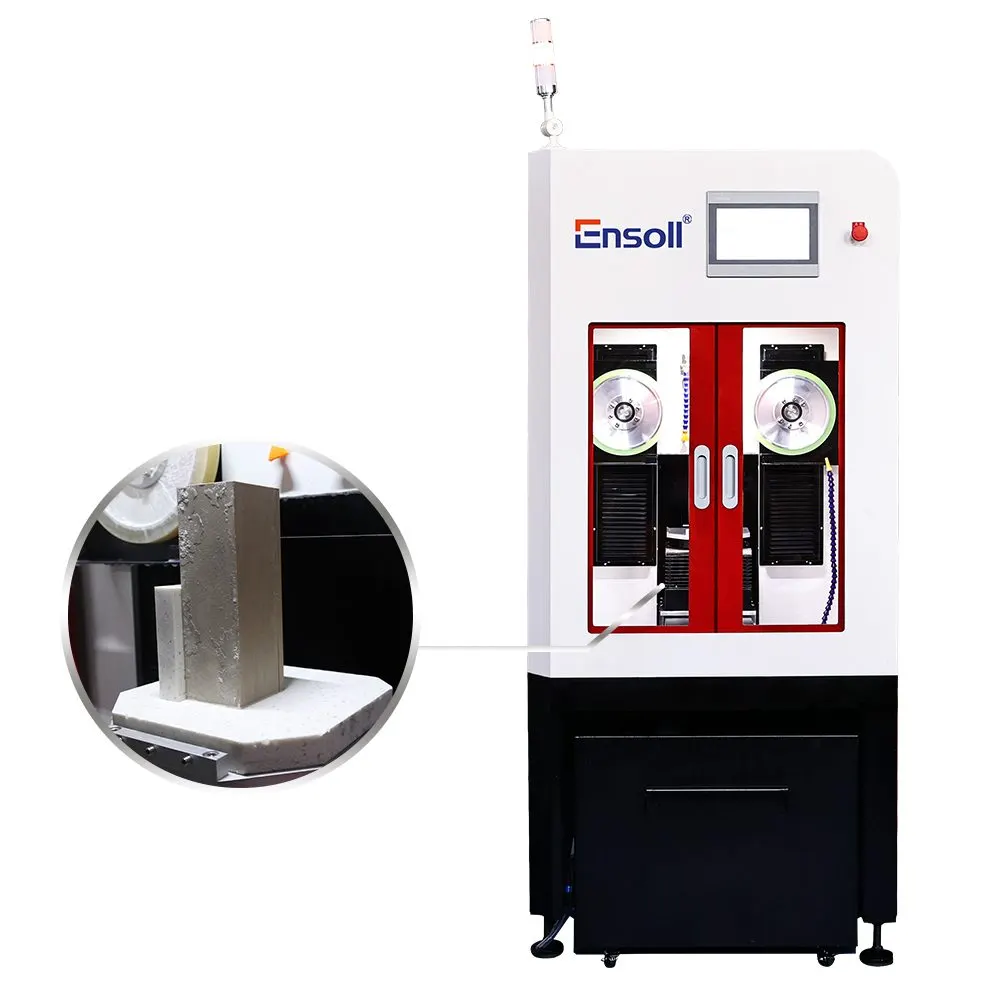
机器: ESO-GM. 鉴于PEEK的热塑性和韧性以及高精度直切要求, Ensoll选择了ESO-GM金刚石线循环切割机. 它可确保切割过程中运行稳定性和路径精度, 减少机床振动和切削负荷波动对PEEK加工质量的影响, 并限制材料变形, edge burrs, 以及由不均匀受力引起的尺寸偏差——提高PEEK片材的尺寸精度和切削表面质量.
冷却液: 切削液. 使用切削液作为冷却介质可改善切削区的散热和润滑, 减少切削热堆积和局部材料软化, 并在切削过程中限制变形和毛刺——有利于PEEK片材的尺寸稳定性和表面质量.
线材: 全包覆型. 一个 0.35 mm fully-coated diamond wire loop 被使用. 全包覆结构提高了磨料颗粒在线材芯上的结合强度和分布稳定性, 在切割过程中保持材料去除的连续性和均匀性,并减少线材磨损和切割状态波动对PEEK零件尺寸精度和表面质量的影响.
图 1. ESO-GM金刚石线循环切割机.
4. 切割方法及机器优势
龙门切割结构. 龙门设计提供高整体刚性和运行稳定性, 自上而下的垂直进给有助于保持金刚石线路径稳定, 减少力度变化对PEEK切缝位置和尺寸精度的影响. 机器还配备了雾气排放系统,用于排出切割过程中产生的油雾, 保持加工区域清洁,为PEEK稳定切割提供良好的工作条件.
智能张力控制. 系统根据加工状态实时调整金刚石线的张力,支持恒张力和变张力模式, 保持线材稳定运转. 稳定的线材张力减少切割路径波动, 限制因张力变化引起的局部不均负荷和断线风险, 并提高PEEK切片的尺寸一致性和加工稳定性.
断线记忆. 如果金刚石线断裂或机器异常停止, 系统会自动记录当前加工位置及相关运行状态. 更换线材后, 切割可以在记录的位置继续进行——减少因重新定位和再加工导致的尺寸偏差和材料损失, 提高PEEK切片的连续性, 并减少因重新定位带来的切缝质量波动.
高刚性一体式铸铁机架. 整体铸铁机架提高整体刚性和抗振性, 减少结构振动和长期微变形对导丝路径的影响. 对于像PEEK这样兼具韧性和可塑性的热塑性材料, 高刚性结构有助于在切割过程中减少振动和力波动, 保持导丝路径和切割状态稳定, 并限制材料变形, edge burrs, 以及因局部力变化引起的切缝尺寸波动——为精密PEEK切片提供稳定的机器基础,以实现尺寸精度和切缝质量控制.
5. 切割参数与冷却
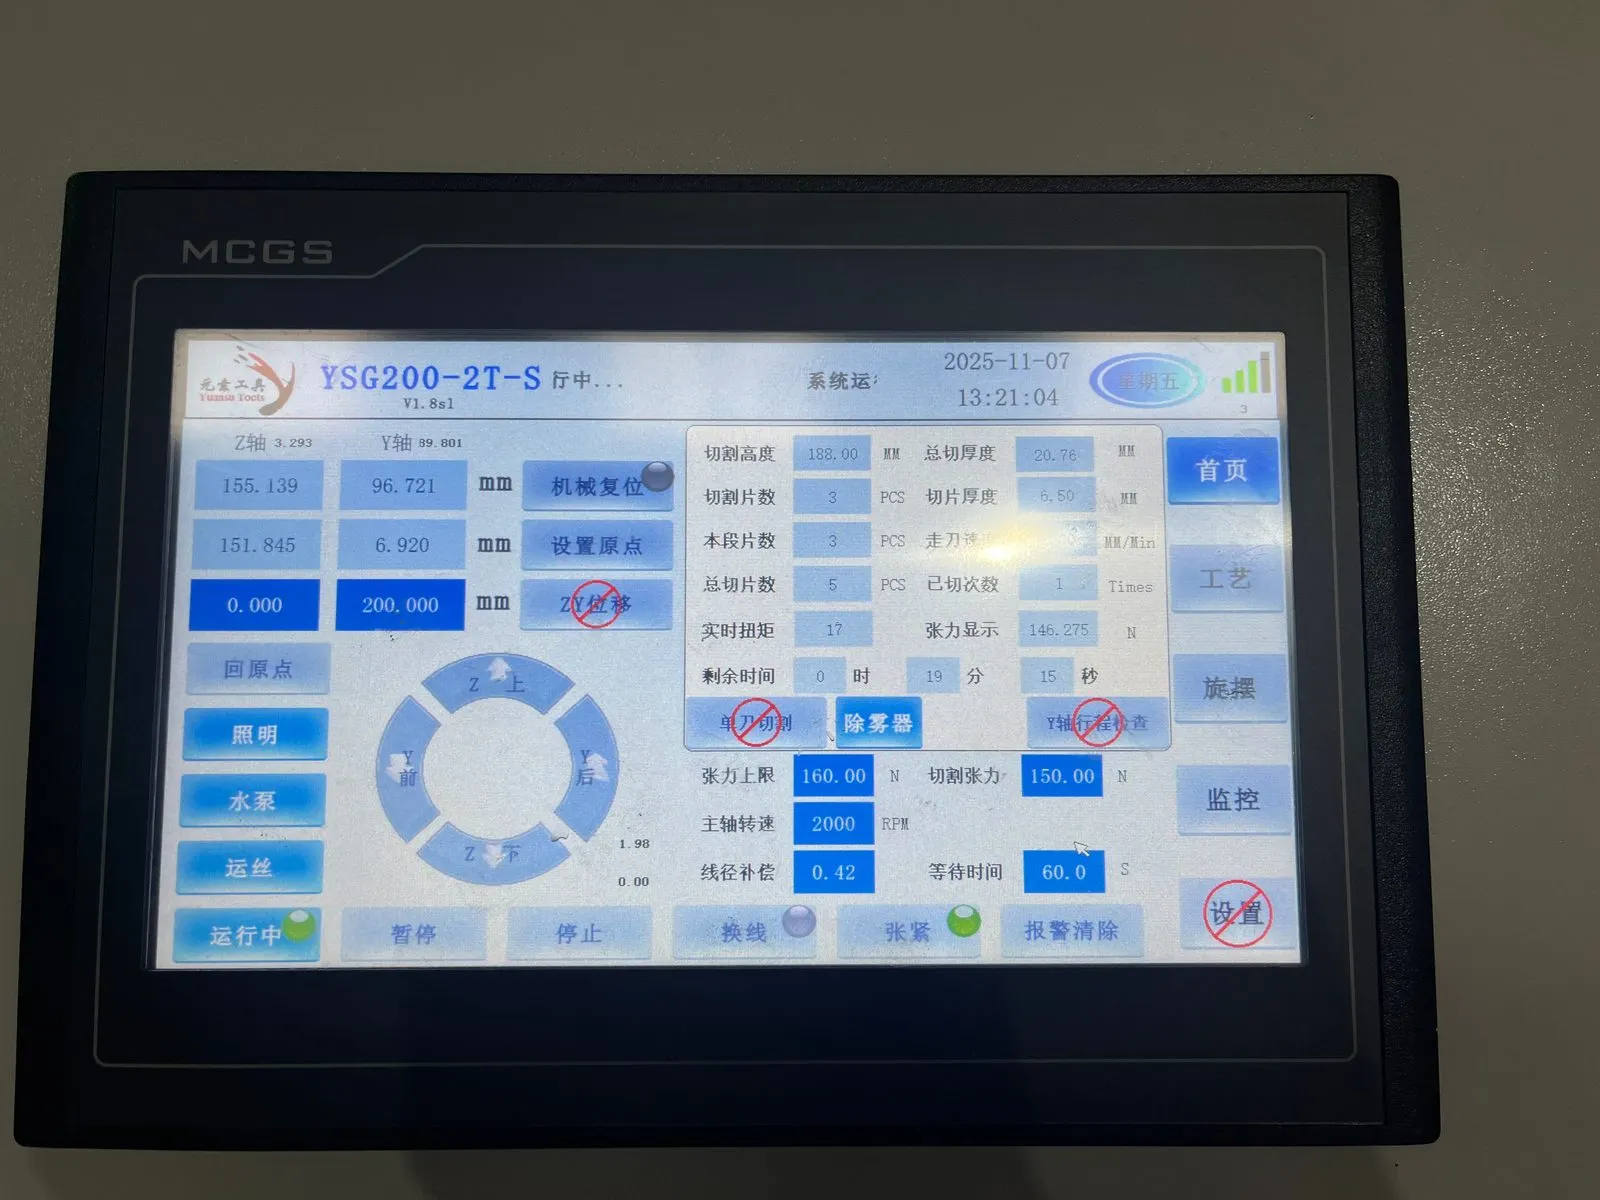
| 参数 | 数值 |
|---|---|
| 导丝直径 × 回路长度 (毫米) | 0.35 × 1880 |
| 进给速度 (毫米/分钟) | 3 |
| 切割宽度 (毫米) | 2 |
| 导丝张力 (N) | 150 |
| 导丝速度 (米/秒) | 24 |
| 导丝弓张紧时间 (秒) | 60 |
| 切割负荷 (牛·米) | 17 |
图 2. 切割工艺参数界面.
6. 切割结果
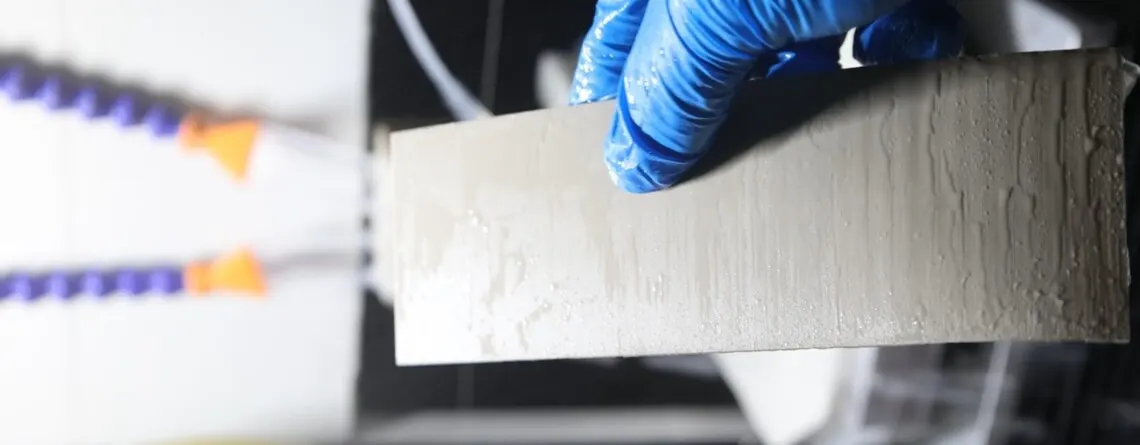
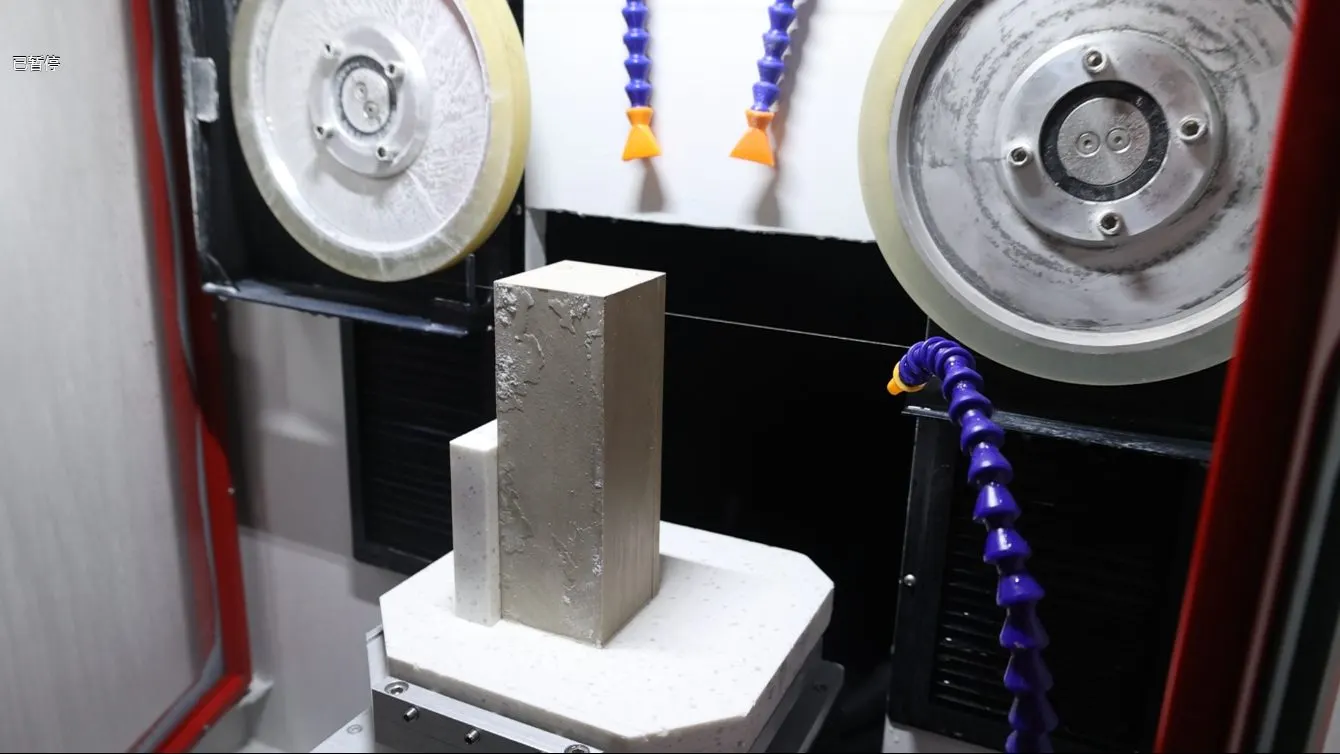
图 3. PEEK正在切割中.
6.1 TTV测试数据 (单位: 毫米)
TTV (总厚度变化) 在真空吸盘上采用九点网格双探针测厚法测量. 金刚线切割的PEEK片样本测得 6.5 mm × 60 mm × 60 毫米,公称厚度为 6.5 毫米. 测试前, 测量设备在恒温下预热,并用标准厚度块校准以减少零点漂移和系统误差. 无尘清洁后, 每个样本居中放置在真空吸盘上,通过负压固定以限制测量过程中的位置移动和局部变形. 然后依次在九个预设网格位置收集厚度数据, 最大值与最小值之差被作为样品的TTV, 用于评估PEEK切片的厚度均匀性和加工一致性.
| 样品 | 九点厚度值 | Tmax | Tmin | TTV |
|---|---|---|---|---|
| S01 | 6.499, 6.487, 6.430 / 6.443, 6.477, 6.528 / 6.467, 6.475, 6.527 | 6.528 | 6.430 | 0.098 |
| S02 | 6.517, 6.526, 6.505 / 6.500, 6.572, 6.567 / 6.526, 6.565, 6.540 | 6.572 | 6.500 | 0.072 |
| S03 | 6.570, 6.569, 6.579 / 6.560, 6.503, 6.556 / 6.507, 6.493, 6.497 | 6.579 | 6.493 | 0.086 |
Evaluation: 三片PEEK切片采用九点法进行测量. TTV值在0.072–0.098 mm之间,平均为 0.085 毫米, and the thickness fluctuation of each sample was similar — indicating that the diamond wire loop cutting process was generally stable and the slices had good thickness uniformity.
6.2 Thickness Tolerance Data (单位: 毫米)
Thickness tolerance was measured with the same nine-point grid method. Taking the nominal thickness of 6.500 mm as the reference, the deviation of each measured point from nominal was calculated, 最大正偏差, maximum negative deviation, and overall thickness tolerance were compiled to evaluate the dimensional accuracy and machining consistency of the PEEK slices.
| 样品 | Average thickness | Deviation |
|---|---|---|
| S01 | 6.481 | −0.019 |
| S02 | 6.535 | +0.035 |
| S03 | 6.537 | +0.037 |
| 最大正偏差 | +0.037 毫米 | |
| 最大负偏差 | −0.019 mm | |
| 厚度公差 | ±0.037 mm | |
Evaluation: Against the 6.500 mm nominal thickness, the average thicknesses of the three PEEK slices were 6.481, 6.535, 和 6.537 毫米, corresponding to deviations of −0.019, +0.035, 和 +0.037 毫米. 最大正偏差为 +0.037 毫米, 最大负偏差 −0.019 mm, 整体厚度公差 ±0.037 mm. S02 和 S03 略高于标称值,而 S01 显示轻微负偏差, 但样本间偏差较小,整体尺寸分布稳定——表明在钻石线环切割过程中材料去除均匀,PEEK 薄片厚度一致性好,尺寸控制良好.
6.3 表面粗糙度 Ra 数据 (单位: 微米)
表面粗糙度 (Ra) 根据 ISO 标准进行测试 4287 使用触针轮廓测量法. 采集每片 PEEK 切割表面三个代表性位置的轮廓数据——中心, 中左, and mid-right — and the Ra parameter was calculated to evaluate the surface roughness and machining quality of the slices after diamond wire loop cutting.
| 样品 | Ra-1 | Ra-2 | Ra-3 | 平均Ra |
|---|---|---|---|---|
| S01 | 0.92 | 0.86 | 0.95 | 0.91 |
| S02 | 0.81 | 0.76 | 0.84 | 0.80 |
| S03 | 0.87 | 0.82 | 0.90 | 0.86 |
Evaluation: The three-point method gave average Ra values of 0.91, 0.80, 和 0.86 μm for the three samples, with an overall distribution of 0.76–0.95 μm. Ra varied little between measurement positions, 表示各区域表面纹理均匀,且线材运行状态稳定及材料去除过程稳定. 总体, PEEK片材表面粗糙度低,表面加工质量良好, 满足下游精密应用的表面完整性要求.
6.4 边缘崩缺数据 (单位: 微米)
边缘崩缺通过使用工具显微镜的光学成像进行定量表征. 测试前, 清洁样品边缘,并校准仪器的放大倍数和测量刻度. 然后在显微镜下观察片材边缘; 定位可识别的边缘缺陷, 测量, 并记录, 每个点的缺陷尺寸及最大缺陷尺寸被用来评估PEEK片材的边缘完整性和加工质量.
| 样品 | 位置 1 | 位置 2 | 位置 3 | 位置 4 | 最大崩缺 |
|---|---|---|---|---|---|
| S01 | 4.8 | 5.6 | 5.1 | 6.3 | 6.3 |
| S02 | 4.2 | 5.0 | 5.5 | 6.0 | 6.0 |
| S03 | 4.6 | 5.4 | 5.9 | 6.7 | 6.7 |
Evaluation: The four-point method showed edge chipping distributed within 4.2–6.7 μm, with a maximum of 6.7 微米. Edge defects were small overall with limited measurement scatter, indicating stable material removal during diamond wire loop cutting and good edge integrity of the slices.
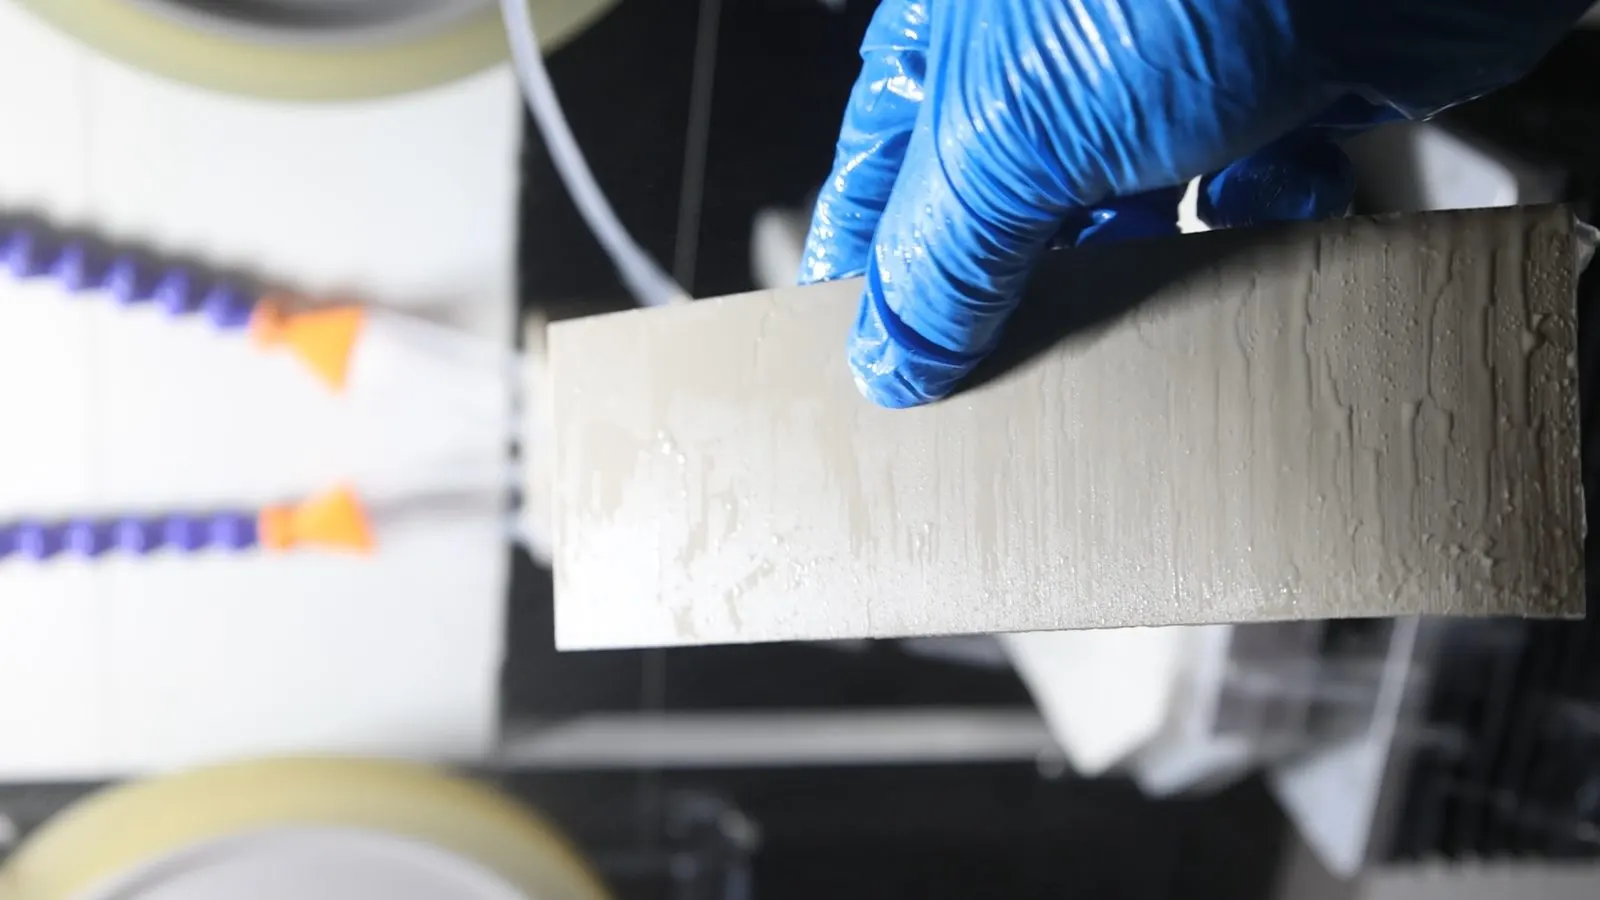
图 4. PEEK slices after cutting.
7. 结论
The good results of this high-precision PEEK slicing test came mainly from the proper matching of a dedicated cutting machine, cooling conditions, and cutting parameters. PEEK is a high-performance thermoplastic with high toughness, 耐磨性, and a degree of heat stability. Under diamond wire cutting it undergoes continuous abrasive action and generates cutting heat; when that heat cannot dissipate in time or parameters are mismatched, the machining zone heats up and the material softens locally, which can cause dimensional deviation, edge burrs, and surface-quality loss. The process was therefore optimized in three areas — machine selection, 冷却, and parameters — to keep cutting stable while controlling dimensional accuracy and surface quality.
Machine selection. For the motion stability, cutting accuracy, and rigidity that PEEK slicing demands, a dedicated 金刚线锯机 for precision PEEK machining was used. Its structural rigidity and running stability provide reliable mechanical conditions for smooth wire travel and stable workpiece cutting, reducing the influence of machine vibration, motion error, and wire-running fluctuation on the cutting path. Stable feed and motion control also reduces cutting-load variation, keeping the wire and the PEEK in a relatively stable cutting state and limiting dimensional deviation and edge-quality problems caused by force fluctuation.
冷却. Given PEEK’s thermoplasticity and its tendency to generate cutting heat, cutting fluid was used as the cooling medium to continuously cool and lubricate the cutting zone. The fluid promptly carries away the heat generated at the wire–PEEK interface and improves lubrication there, reducing the influence of cutting-heat buildup and local softening on the process. Good cooling keeps material removal stable and limits temperature-induced deformation, edge burrs, and dimensional fluctuation — improving the dimensional consistency and surface quality of PEEK slices.
Parameters. Wire speed and feed rate were matched to PEEK’s thermoplastic characteristics and the target slice size. Parameter settings were based on stable wire running and uniform material removal, avoiding excessive feed that would raise cutting load and concentrate heat, and avoiding mismatched parameters that would cause uneven removal and process fluctuation. With force and temperature rise kept in a suitable range, material removal stayed stable while efficiency was maintained — improving slice thickness consistency, 尺寸精度, 切割表面质量.
综上——尺寸精度, thickness tolerance, 表面粗糙度 (Ra), 和边缘质量——结果表明,使用专用设备, 适当的冷却, 以及合适的切割参数协同工作, 金刚石线环切割可以很好地满足PEEK高精度直切片的要求. 加工过程中, 机器运行, 冷却, 和材料去除都保持稳定, 切片的尺寸一致性和表面质量得到了有效控制. 对于像PEEK这样的热塑性材料, 适当匹配的设备, 冷却, 和工艺参数可以改善切割的热-机械状态和材料去除的稳定性, 为PEEK高精度直切片提供了工艺参考.
Related Process Data
本测试中使用的厚度测量方法另行记录在 nine-point TTV measurement guide. For the same measurement basis applied to a low-density structural foam cut dry on a horizontal machine, see PEEK vs PMI foam, and for that material’s process window, PMI foam cutting parameters.
常见问题
Can a diamond wire loop cut PEEK and other engineering plastics?
是的. Although PEEK is a tough thermoplastic rather than a hard-brittle material, a rigid machine, a fully-coated diamond wire loop, continuous cutting-fluid cooling, and conservative parameters deliver stable precision slicing. In this test, three PEEK slices achieved average TTV of 0.085 毫米, thickness tolerance of ±0.037 mm, average Ra below 1 微米, and maximum edge chipping of 6.7 微米.
What cutting parameters are recommended for slicing PEEK?
In this test: 一个 0.35 mm × 1880 mm fully-coated diamond wire loop at 24 m/s wire speed, 3 mm/min feed rate, 150 N wire tension, 2 mm cutting width, and cutting fluid as the cooling medium. The principle is to keep cutting load and heat generation low so the thermoplastic material does not soften at the kerf.
切割PEEK时为什么冷却液很重要?
当切割区受热时,PEEK会软化. 切削液持续从线材-材料界面带走热量并改善润滑, 防止局部软化,否则会导致尺寸偏差, edge burrs, 以及表面质量差.
金刚石线环切割PEEK可以达到什么表面光洁度和边缘质量?
In this test, 平均表面粗糙度为0.80–0.91 μm Ra (整体范围为0.76–0.95 μm, 按ISO标准测量 4287), 边缘崩边保持在4.2–6.7 μm以内,最大值为 6.7 微米.
此次PEEK切片测试使用的机器是哪种?
Ensoll ESO-GM门式金刚石线环切割机, 具有智能线张力控制系统, 线断点记忆功能, 雾气提取系统, 以及高刚性一体铸铁机架.
技术内容由Ensoll工程团队审核——一家金刚线环制造商 10+ 多年生产经验.