BG38 玻璃板切割使用金刚石线环: 5 毫米 测试数据
抽象: This application report documents a high-precision straight-slicing test on BG38
glass sheet supplied by a European customer. The workpiece measured 86 mm x 60 mm x 1 mm and was cut into strips
之 5 mm x 60 mm x 1 mm on an ESO-GM gantry diamond wire loop cutting machine, using
cutting oil as the cooling medium and a fully coated diamond wire. Measured results: total thickness variation
(TTV) 0.003-0.020 毫米 (average 0.014 毫米), thickness tolerance ±0.027 mm, surface roughness Ra 0.63-0.76 微米,
and maximum edge chipping 5.1-6.5 微米. Matching the machine structure, the oil cutting method and the process
parameters to the brittle behaviour of BG38 glass kept material removal stable and held strip dimensional accuracy
and cut-surface quality within a workable range.
关键要点
- BG38 is a hard, brittle glass with low fracture toughness, so the risk in wire slicing is edge chipping,
micro-cracking and thickness scatter rather than tool wear. - An 86 mm x 60 mm x 1 mm sheet was sliced into 5 mm x 60 mm x 1 mm strips on an ESO-GM gantry diamond wire loop
machine, with cutting oil and a fully coated diamond wire. - Across the three strips: TTV 0.003-0.020 毫米 (mean 0.014 毫米), thickness tolerance ±0.027 mm, Ra 0.63-0.76 微米,
maximum chipping 5.1-6.5 微米. - Sample S02 held TTV to 0.003 毫米, so the machine and parameter set clearly have the capability; the spread
between samples points at setup repeatability rather than the cutting process. - Two of the three strips ran thin (自 -0.027 毫米). That is a systematic offset, and it can be taken out with
dimensional compensation on the next run.
Sample test for a European customer | Diamond wire loop cutting process
Overview of the BG38 Glass Sheet Slicing Test
This test was carried out on BG38 glass sheet supplied by a European customer, with high-precision straight
slicing as the main requirement. BG38 belongs to the hard, brittle family of glasses: hardness is fairly high,
brittleness is pronounced and fracture toughness is low. Under the continuous abrasion of diamond grains, 切削
load and local heat build-up can concentrate stress inside the material, which is how chipping, micro-cracks, an
uneven cut face and strip dimensional deviation appear. The work therefore focused on matching machine stability,
cooling and lubrication, and the cutting parameters, so that load fluctuation and thermal effects through the cut
stayed low and the strip dimensions and cut-surface quality met the requirement set for
光学玻璃切割.
Because of what BG38 glass demands in cutting stability, dimensional accuracy and edge integrity, Ensoll applied
a diamond wire solution matched to glass machining. On the machine side, a dedicated gantry diamond wire loop
cutting machine was used, whose rigidity and running stability give the workpiece a firm clamping base and the wire
a steady path, cutting down the effect of machine vibration and motion error on the cutting trajectory and on strip
尺寸. On the consumable side, a diamond wire suited to glass keeps the abrasive grains removing material at a
steady rate, so wire wear does not show up as a change in strip dimensions. On the cooling side, 切削油
lubricates and cools the contact zone between wire and glass, which holds friction heat and its effect on the cut
face and edge in check. Wire running speed and feed rate were then adjusted against the properties of the BG38 sheet
and the target strip size, keeping the cutting load in a suitable band and reducing the local damage and edge
breakage that an excessive instantaneous load causes. Matching machine, wire, cooling conditions and parameters as
one set kept the slicing process stable and brought strip dimensional accuracy, 厚度一致性, cut-face
quality and edge integrity under control — a workable process basis for high-precision straight slicing of
BG38 glass sheet.
1. Test Object: Basic Information
- Material: BG38 glass sheet
- 硬度: approximately MH 6.5
- Workpiece dimensions: 86 mm x 60 mm x 1 毫米
- Cut dimensions: 5 mm x 60 mm x 1 毫米
2. Machine and Wire Selection
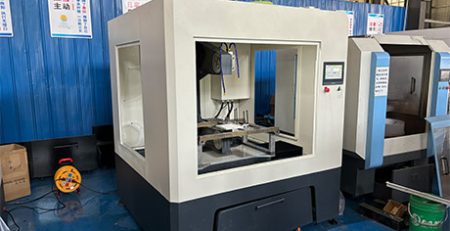
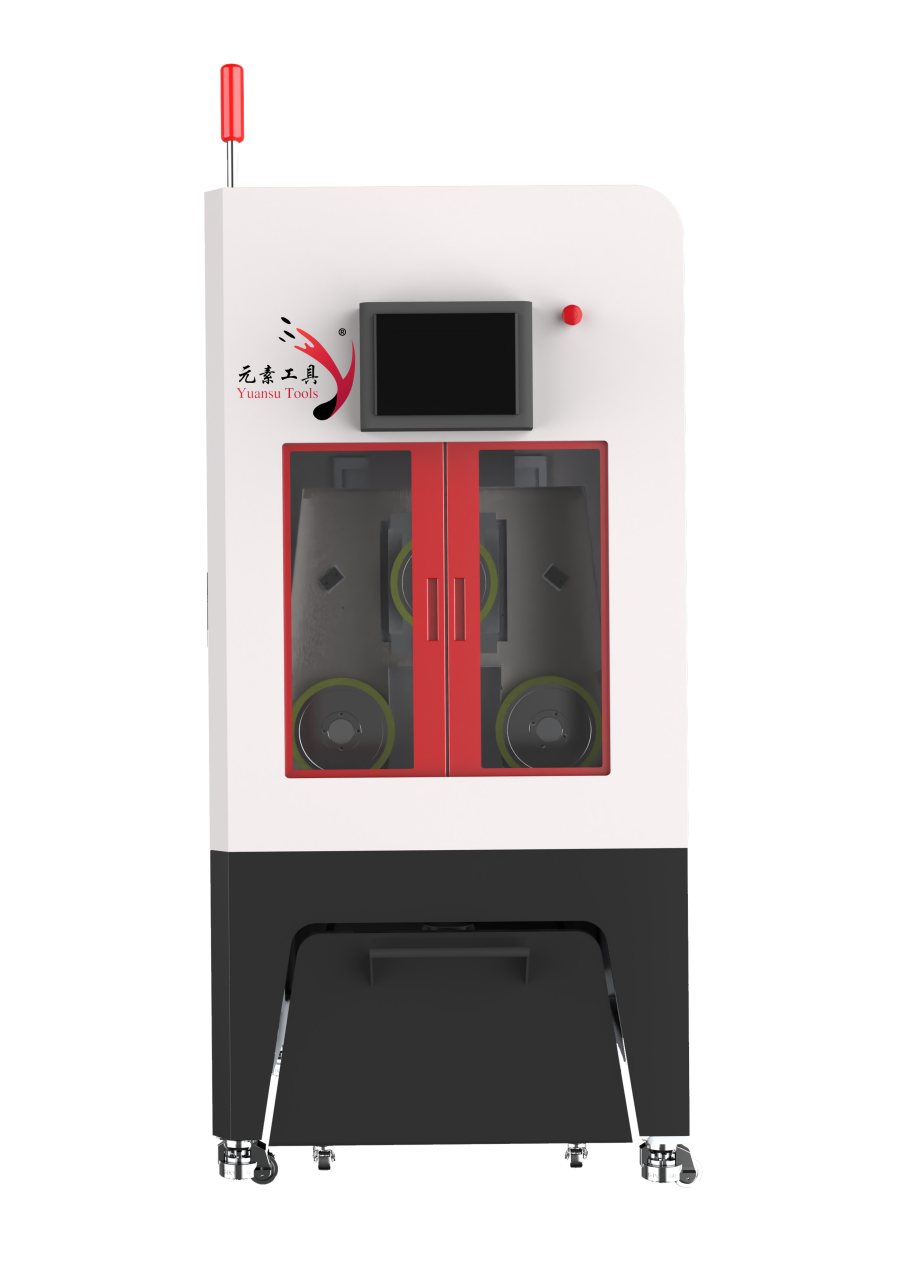
Machine type: ESO-GM. Given the brittleness of BG38 glass and the high-precision straight
slicing requirement, Ensoll选择了 ESO-GM diamond wire saw, the gantry machine
suited to glass machining. It holds running stability and trajectory accuracy through the cut, reduces the effect of
machine vibration and cutting-load fluctuation on machining quality, limits the chipping, micro-cracking and
dimensional deviation that uneven loading would otherwise produce, and so improves dimensional accuracy, cut-surface
quality and edge integrity in BG38 strips.
- Coolant type: 切削油. Cutting oil is used as the cooling and lubricating medium. It
improves heat dissipation and lubrication in the cutting zone, lowers friction and heat build-up through the cut,
and reduces the thermal and local stress variation the BG38 sheet sees. That lowers the risk of chipping,
micro-cracks and cut-face damage, which helps dimensional stability, surface quality and edge integrity. - Wire type: fully coated. A fully coated diamond wire raises the bond strength between grains
and the steel core and keeps grain distribution even, so the wire removes material continuously and steadily
through the cut. It reduces the effect of grain pull-out and wire wear on the cutting state, which limits
dimensional variation and edge damage in BG38 slicing.
3. 切割方法及机器优势
Gantry cutting method. The gantry structure gives the machine high overall rigidity and running
稳定性, and the top-down vertical feed helps keep the 金刚石线环 on a stable
path, reducing the effect of load variation on kerf position and dimensional accuracy in BG38 strips. The machine
also carries a mist extraction system that clears the oil mist produced during cutting, keeping the work zone clean
and the cutting area in good condition.
Intelligent tension control system. The system adjusts wire tension in real time according to
the machining state and supports both constant-tension and variable-tension modes, so the wire runs steadily
through the cut. Stable tension reduces trajectory fluctuation and limits the uneven local loading and wire-break
risk that tension variation brings, which cuts down the chipping, micro-cracks and dimensional deviation seen in
BG38 strips and improves consistency across the batch.
Breakpoint resume. If the wire breaks or the machine stops abnormally, the system records the
current cutting position and the associated running state. After a wire change the cut resumes from that position,
which reduces the dimensional deviation and material loss that re-positioning and repeat cutting cause, keeps strip
processing continuous, and limits kerf quality variation.
High-rigidity one-piece cast iron frame. The one-piece cast iron frame raises overall stiffness
and vibration resistance, lowering the effect of structural vibration and long-term micro-deformation on the wire
path. For a hard, brittle material such as BG38 glass, that rigidity reduces vibration and load fluctuation during
the cut, 保持导丝路径和切割状态稳定, and limits chipping, micro-cracks and kerf surface damage
caused by local load changes. It gives the dimensional accuracy and kerf quality of precision slicing a stable
machine basis.
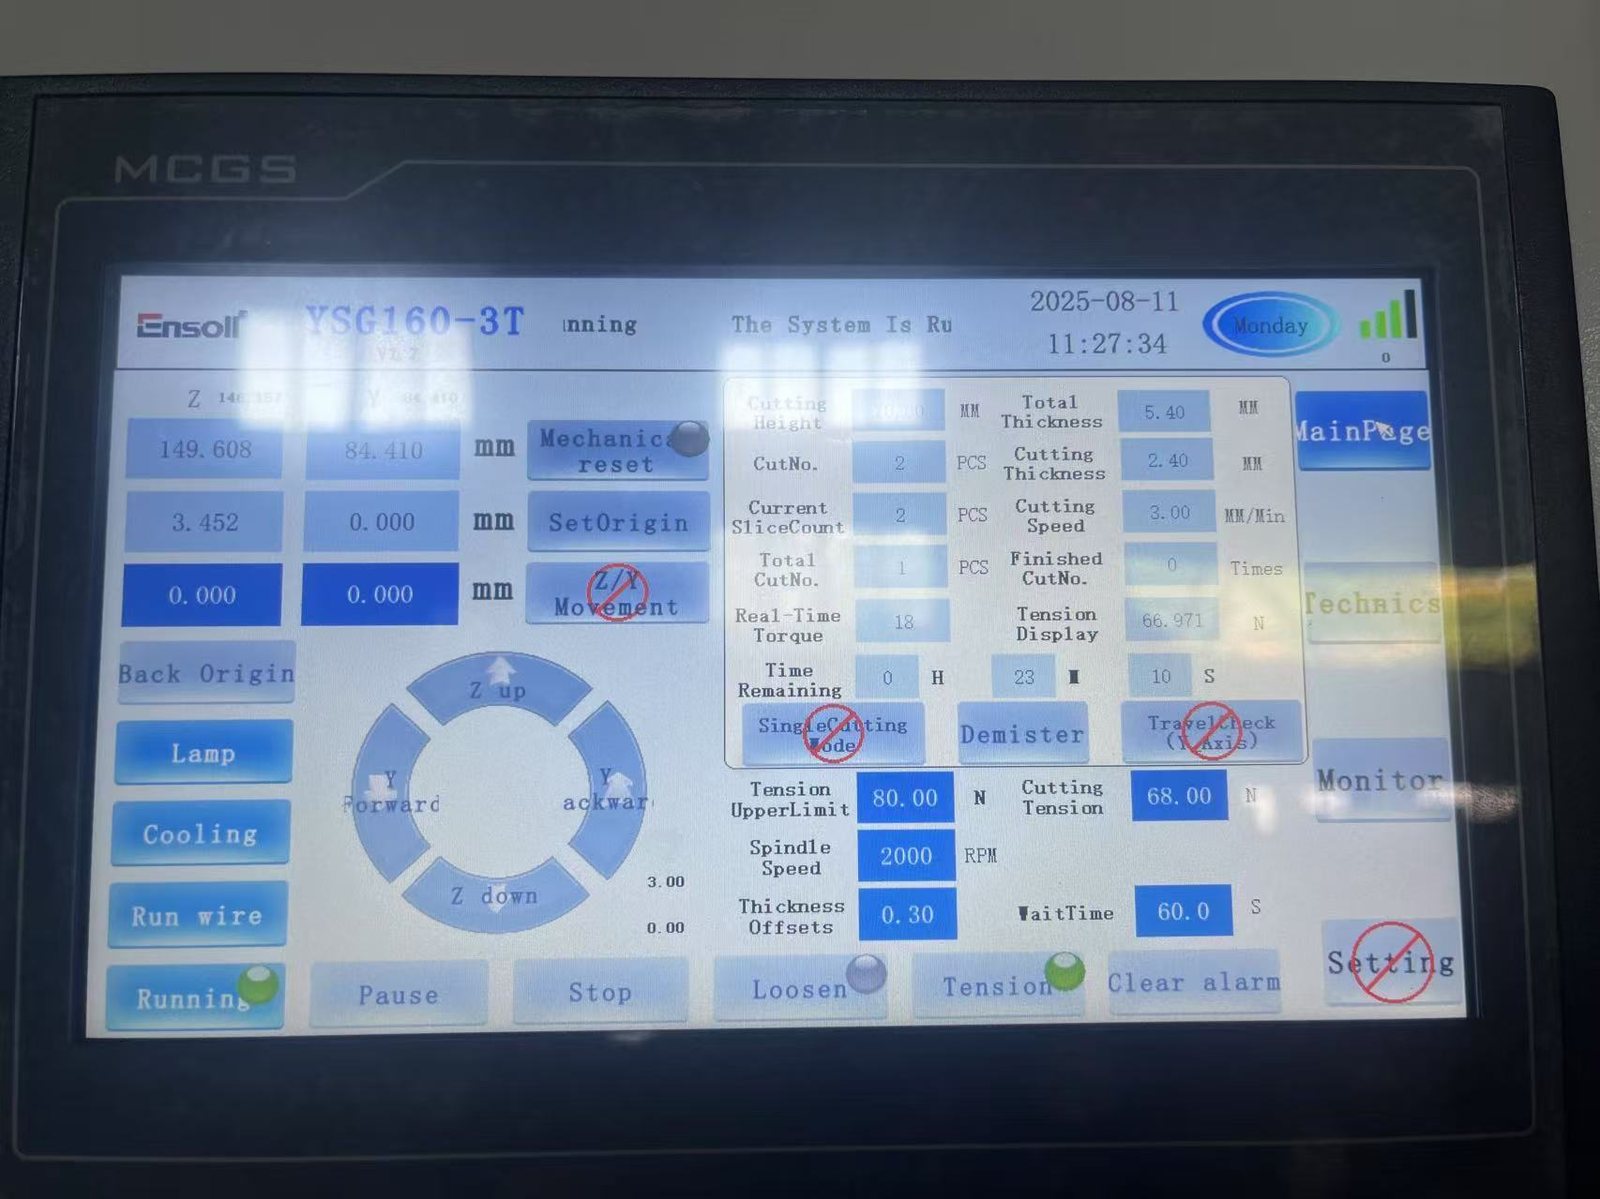
4. Parameter Settings and Cooling Method
| 参数 | 数值 |
|---|---|
| 线径 (毫米) | 0.25 x 1880 |
| Wire travel speed (毫米/分钟) | 3 |
| 切割宽度 (毫米) | 1 |
| Cutting wire tension (N) | 68 |
| 导丝速度 (米/秒) | 24 |
| Wire-bow time (秒) | 60 |
| 切割负荷 (N·m) | 18 |
5. Cutting Efficiency and Results
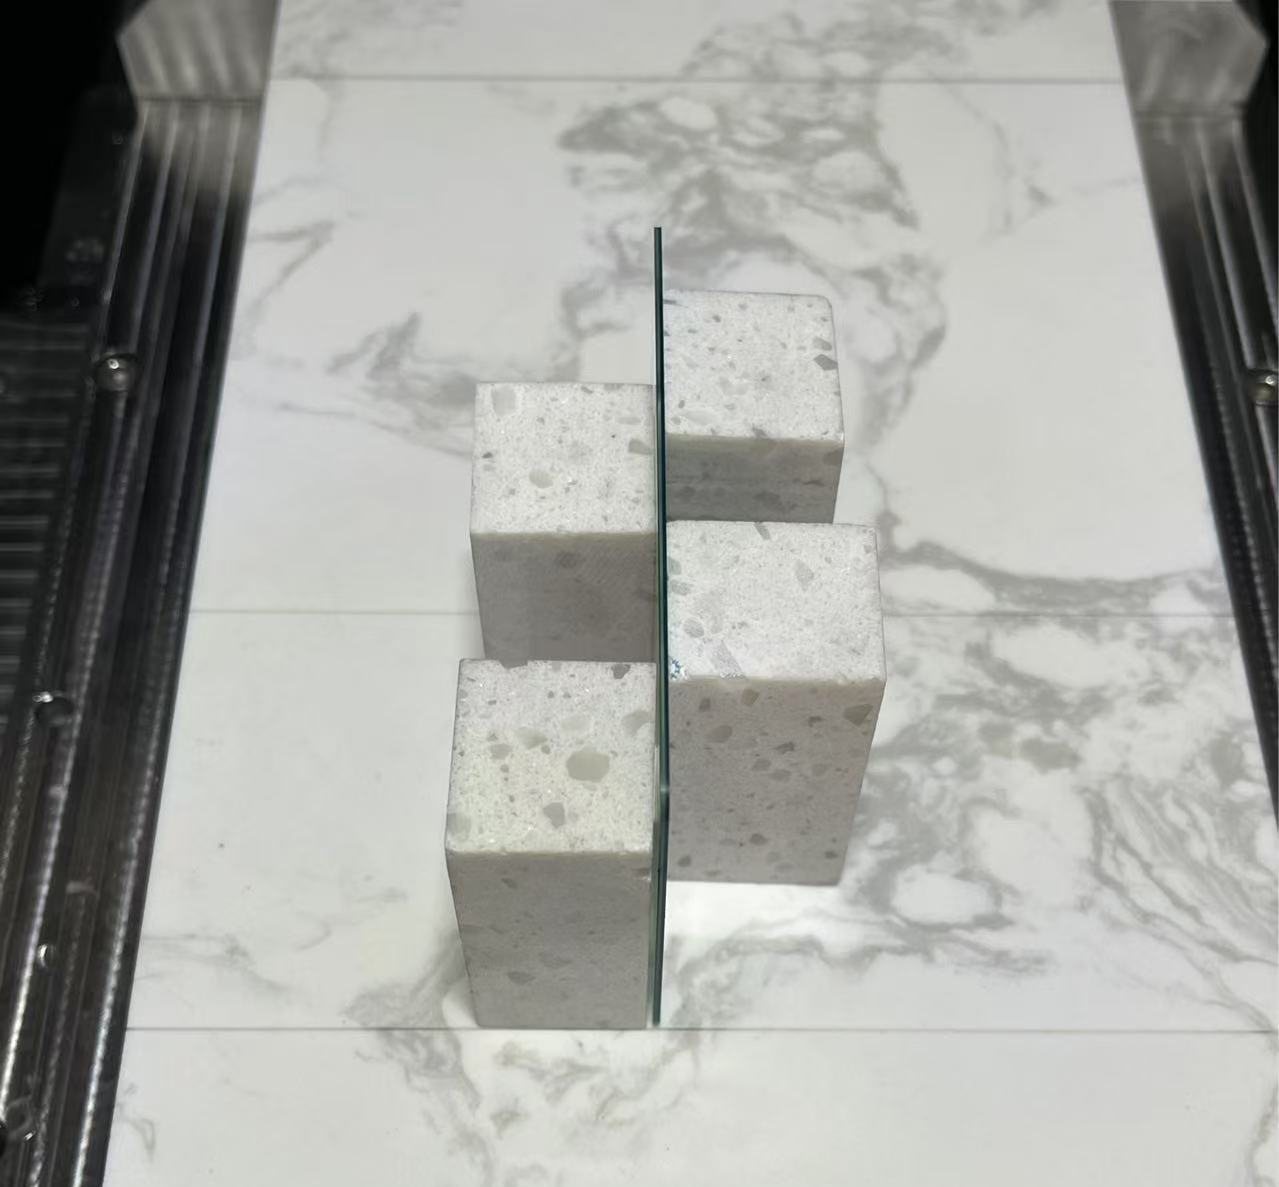
5.1 TTV测试数据 (毫米)
TTV (总厚度变化) was measured with a nine-point grid, dual-probe thickness method on a
vacuum-chuck stage, applied to BG38 strips produced by diamond wire loop cutting. The strips measured
5 mm x 60 mm x 1 毫米, with a nominal thickness of 5 毫米. Before measurement the instrument was thermally stabilised
and calibrated with a standard thickness block to reduce zero drift and systematic error. 无尘清洁后,
each sample was centred on the vacuum chuck and held by negative pressure, so that position shift, warping and local
deformation during measurement had less effect on the thickness readings. Thickness data were then collected in
sequence at the preset nine grid positions, and the difference between the largest and smallest reading across those
points was taken as the TTV of that sample, which is used to evaluate the thickness uniformity and machining
consistency of BG38 strips. The procedure follows the same nine-point method used in our
H-K9L optical glass cutting test.
| 样品 | Nine-point thickness readings (毫米) | Tmax | Tmin | TTV |
|---|---|---|---|---|
| S01 | 4.962, 4.969, 4.974 / 4.968, 4.972, 4.978 / 4.974, 4.981, 4.978 | 4.981 | 4.962 | 0.019 |
| S02 | 4.982, 4.983, 4.984 / 4.983, 4.984, 4.985 / 4.984, 4.983, 4.985 | 4.985 | 4.982 | 0.003 |
| S03 | 4.995, 4.998, 4.999 / 4.997, 5.001, 5.004 / 5.002, 5.010, 5.015 | 5.015 | 4.995 | 0.020 |
Evaluation: Three BG38 strips were tested for thickness uniformity with the nine-point method.
TTV ranged from 0.003 自 0.020 mm with an average of 0.014 毫米. Sample S02 showed the smallest variation, at
0.003 毫米. Overall the strip thickness distribution is fairly stable, which indicates good thickness control
through the diamond wire loop process.
5.2 Thickness Tolerance Data (毫米)
Thickness tolerance was measured by the same nine-point grid method, 跟 5.000 mm as the nominal thickness. 这
deviation of each measured point from nominal was calculated, and the maximum positive deviation, maximum negative
deviation and overall thickness tolerance were collated, to assess the dimensional accuracy and machining
consistency of the BG38 strips.
| 样品 | Average thickness (毫米) | 厚度偏差 (毫米) |
|---|---|---|
| S01 | 4.973 | -0.027 |
| S02 | 4.984 | -0.016 |
| S03 | 5.002 | +0.002 |
| Maximum positive deviation | +0.002 | +0.002 |
| Maximum negative deviation | -0.027 | -0.027 |
| Thickness tolerance | ±0.027 | ±0.027 |
Evaluation: 凭借 5.000 mm as the nominal thickness, the three BG38 strips averaged 4.973, 4.984
和 5.002 毫米, corresponding to thickness deviations of -0.027, -0.016 和 +0.002 毫米. The maximum positive deviation
was +0.002 毫米, the maximum negative deviation -0.027 毫米, and the overall thickness tolerance ±0.027 mm. Samples S01
and S02 sat slightly below nominal while S03 came in marginally above it; the spread between samples is small, which
indicates even material removal through the cut and good thickness consistency and dimensional control in the BG38
strips.
5.3 表面粗糙度 Ra 数据 (微米)
表面粗糙度 (Ra) was measured to ISO 4287 with a stylus profiler. Three representative positions were
profiled on the cut face of each BG38 strip — centre, mid-left and mid-right — and Ra was calculated at
each position to assess surface quality after diamond wire loop cutting.
| 样品 | Ra-1 | Ra-2 | Ra-3 | 平均Ra |
|---|---|---|---|---|
| S01 | 0.68 | 0.72 | 0.70 | 0.70 |
| S02 | 0.61 | 0.65 | 0.63 | 0.63 |
| S03 | 0.74 | 0.78 | 0.76 | 0.76 |
Evaluation: Three BG38 strips were measured for surface roughness by the three-point method.
Average Ra ranged from 0.63 自 0.76 微米, with little difference between measuring positions. That indicates a broadly
uniform cut face and a stable wire running and material-removal process.
5.4 边缘崩缺数据 (微米)
Chipping was measured by optical imaging on a toolmaker’s microscope to quantify edge defects on the BG38 strips.
Sample edges were cleaned before measurement, and the instrument magnification and measuring scale were calibrated.
The edge regions were then examined under the microscope, recognisable chips were located and measured, and the
defect size at each point was recorded. The largest chip on a strip was taken as the main index, giving an
assessment of edge integrity and machining quality after cutting BG38 glass.
| 样品 | 位置 1 | 位置 2 | 位置 3 | 位置 4 | 最大崩边 |
|---|---|---|---|---|---|
| S01 | 4.8 | 5.6 | 5.1 | 6.2 | 6.2 |
| S02 | 3.9 | 4.7 | 4.3 | 5.1 | 5.1 |
| S03 | 5.0 | 5.8 | 5.4 | 6.5 | 6.5 |
Evaluation: Three BG38 strips were inspected for edge chipping by the four-point method. Defect
sizes were generally small, with maximum chipping between 5.1 和 6.5 μm and little difference between measuring
points and between samples. That indicates a stable cutting state through the diamond wire loop process and good
edge integrity on the strips.
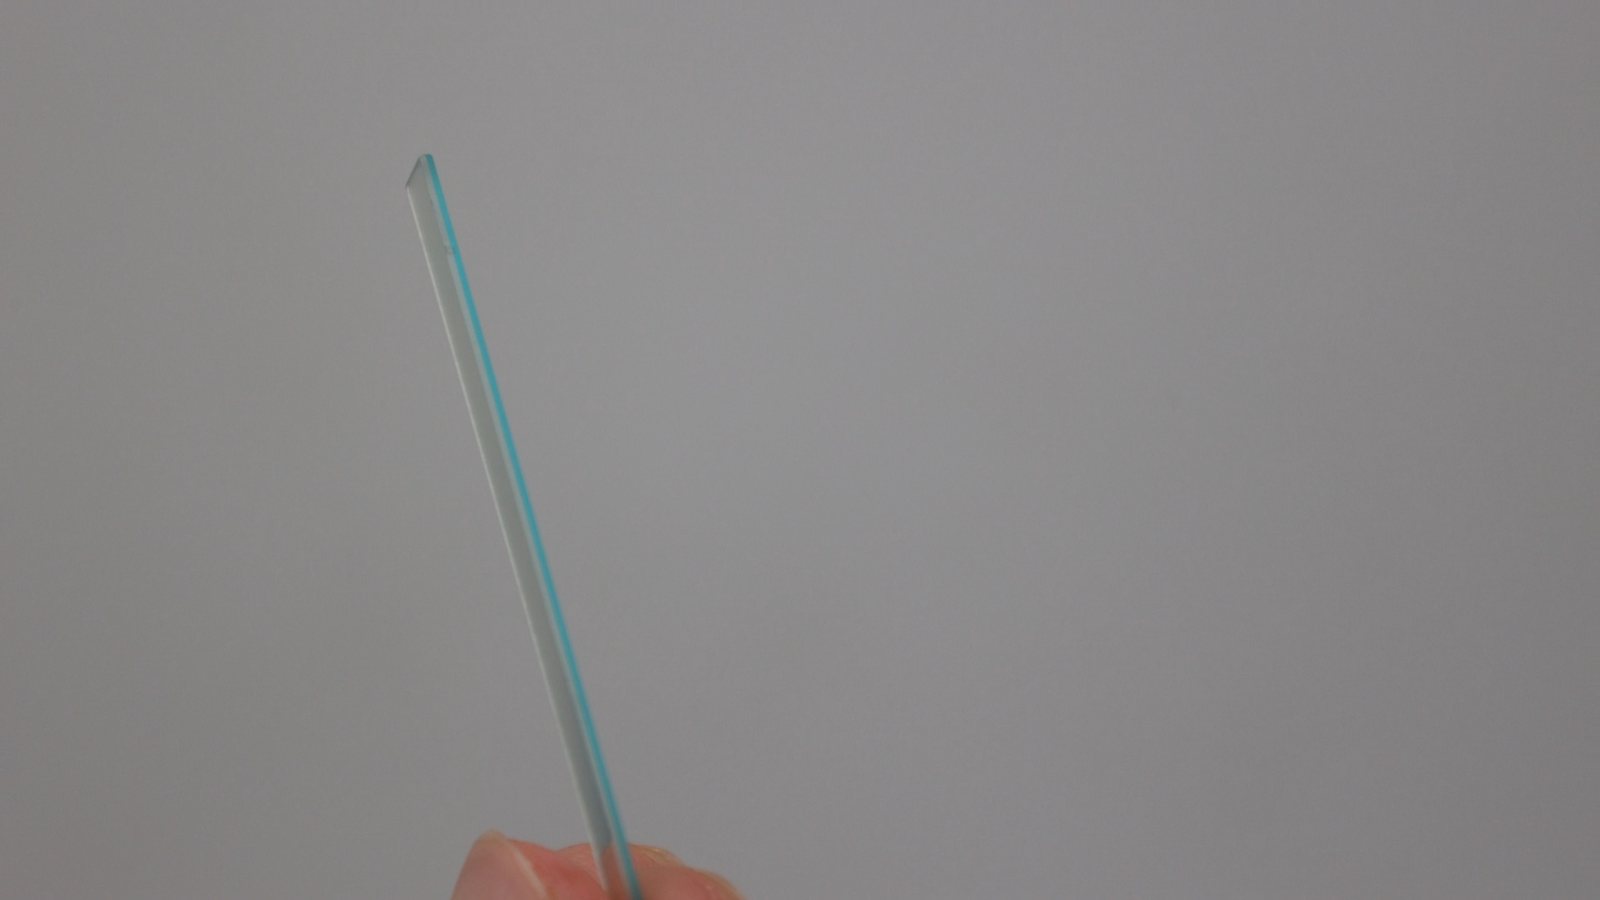
6. 结论
The high-precision slicing of BG38 glass sheet in this test produced good results, mainly because the dedicated
gantry cutting machine, the oil cutting method and the process parameters were matched as one set. Glass is a
classic hard, brittle material: hardness is fairly high, brittleness is pronounced and fracture toughness is low,
and during diamond wire loop cutting the material is easily affected by local cutting load and heat build-up, which
produces chipping, micro-cracks, an uneven cut face and strip dimensional deviation. Aimed at the machining
behaviour of glass and the requirement for high-precision straight slicing, this work therefore adjusted machine
selection, cutting method and process parameters in a targeted way, holding strip dimensional accuracy and
cut-surface quality in check while keeping the cutting process stable.
First, machine selection. Given what glass sheet slicing demands in machine rigidity, motion
stability and cutting accuracy, a dedicated gantry diamond wire loop cutting machine was selected. The gantry
structure provides good overall rigidity and running stability, which gives the workpiece firm clamping and the wire
a reliable mechanical basis for steady running. The top-down vertical feed helps hold the cutting trajectory stable
and reduces the effect of machine vibration, motion error and load variation on cut position and dimensional
准确性. Stable feed and motion control also narrow the cutting-load variation, so the glass is removed under
comparatively steady conditions, which lowers the risk of local chipping and strip dimensional deviation and gives
high-precision glass sheet slicing a stable machine basis.
Second, cutting method. Given the properties of the material, oil cutting was used, with cutting
oil as the cooling and lubricating medium. Cutting oil improves lubrication and heat dissipation in the contact zone
between wire and glass, lowering friction and heat build-up through the cut and reducing the effect of local
temperature rise and thermal stress on the glass and the cut section. Good cooling and lubrication also help hold
the cutting zone in a steady state and reduce the cutting fluctuation that higher friction or concentrated heat
would cause, so cut-face damage, edge breakage and surface defects become less likely. That is a necessary
condition for keeping glass slicing quality stable.
Third, 工艺参数. Given the brittle behaviour of glass and the target strip size, wire
running speed and feed rate were matched accordingly. Parameters were set to keep the wire running stably and
material removal even, avoiding a feed rate so high that the cutting load rises, and avoiding a parameter
combination that causes local heating, stress concentration and brittle fracture. Targeted adjustment of the
cutting parameters kept material removal comparatively steady and, while meeting machining efficiency, reduced
impact and load fluctuation through the cut, which improved strip thickness consistency, cut-face quality and edge
integrity.
Taken together, the results for strip dimensional accuracy, thickness tolerance, 表面粗糙度 (Ra) 和
cut-edge quality show that, through coordinated matching of a dedicated gantry cutting machine, oil cutting and
suitable cutting parameters, diamond wire loop cutting meets the requirements of high-precision straight slicing for
glass sheet. The machined samples performed well in dimensional accuracy, 厚度一致性, cut-surface quality
and edge integrity, which indicates that matching machine structure, cooling and lubrication method and process
parameters to the hard, brittle character of glass improves material removal and process stability, and provides a
process reference for high-precision straight slicing of glass-type brittle materials.
常见问题
Can a diamond wire loop cut BG38 glass sheet into 5 mm strips?
是的. In this test an 86 mm x 60 mm x 1 mm BG38 sheet was sliced into strips of 5 mm x 60 mm x 1 mm on an ESO-GM
gantry machine. Measured TTV was 0.003 自 0.020 mm with an average of 0.014 毫米, thickness tolerance was
±0.027 mm, and maximum edge chipping was 5.1 自 6.5 微米, which is a workable basis for precision glass strips.
Why is cutting oil used instead of water for BG38 glass?
Cutting oil lubricates and cools the contact zone between wire and glass. In this test it improved heat
dissipation in the cutting zone and lowered friction and heat build-up through the cut, which reduced the thermal
and local stress variation in the BG38 sheet and lowered the risk of chipping, micro-cracks and cut-face damage. 这
machine carries a mist extraction system to clear the oil mist produced during the cut.
What surface quality can be expected when cutting BG38 glass?
Surface roughness was measured to ISO 4287 with a stylus profiler at three positions per strip. Average Ra ranged
from 0.63 自 0.76 μm with little variation between measuring positions, and maximum edge chipping measured by optical
microscopy was 5.1 自 6.5 微米, indicating a uniform cut face with good edge integrity.
Why did the BG38 strips come out slightly thin?
凭借 5.000 mm as the nominal thickness, the three strips averaged 4.973, 4.984 和 5.002 毫米, so two of them ran
thin by 0.016 自 0.027 毫米. That is a systematic offset rather than random scatter, and it can be corrected directly
through cutting parameters and dimensional compensation on the next run.
Where can I find more process data on diamond wire loop cutting?
Ensoll publishes comparable test data for other glass and hard-to-cut materials, including an H-K9L optical glass
cutting test and a guide to the cost structure of optical glass manufacturing and cutting. For general process
questions, see the 金刚石线圈切割技术常见问题.
Technical content reviewed by the Ensoll engineering team – a diamond wire loop manufacturer with 10+ 多年生产经验.