金属管精密切片: 金刚石线环
Sample test for a European customer · Diamond wire loop cutting process
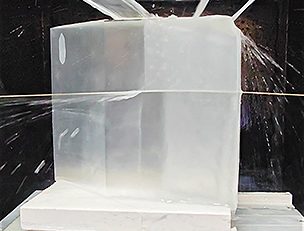
- Thin-wall metal tubes were precision-sliced with a fine diamond wire loop, producing burr-free edges.
- The process avoids the heat-affected zones of laser cutting and the deformation of blade cutting. The same trade-off is quantified on a brittle semiconductor in our comparison of laser cutting vs diamond wire saw.
- Full cutting parameters, TTV data, and surface photos are included for engineering reference.
概述
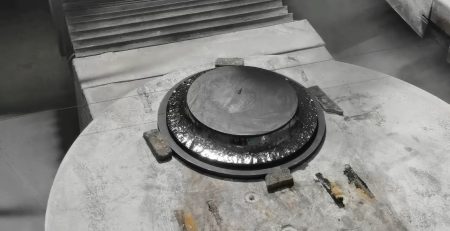
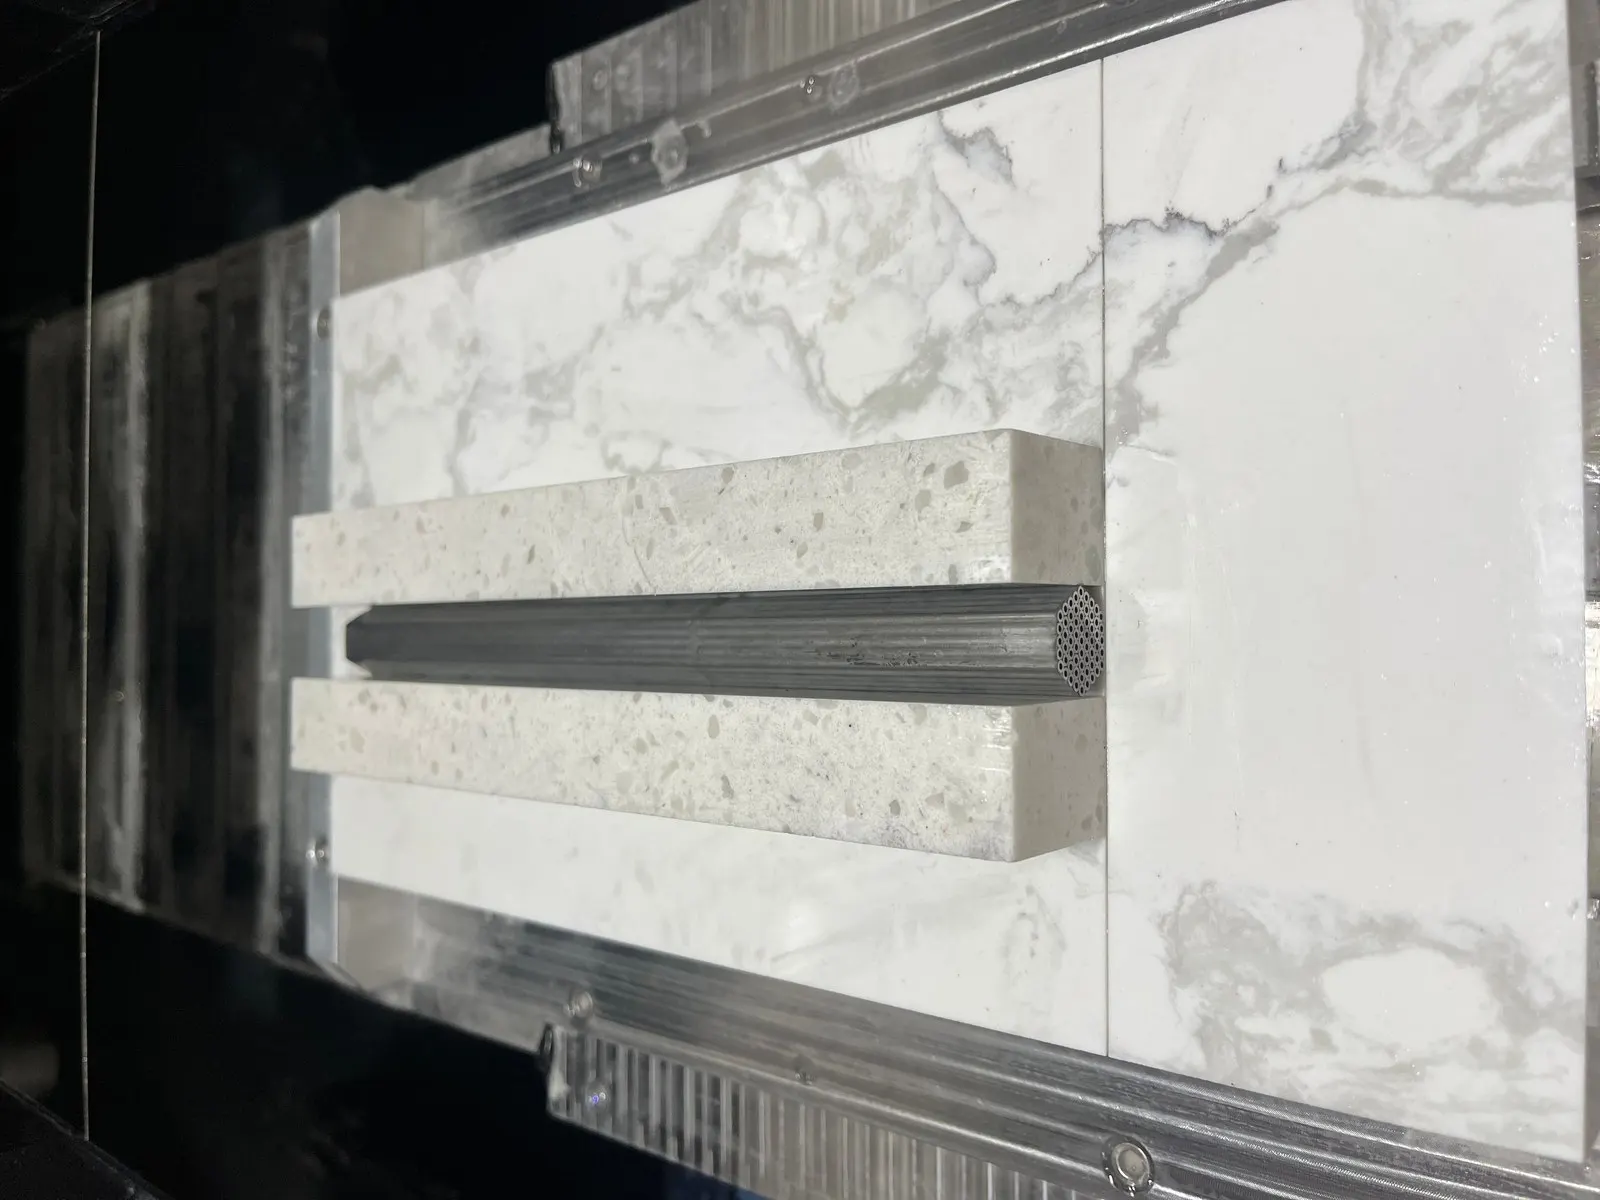
The workpiece in this test was a metal tube sample supplied by a European customer (Company E), who required high-precision straight slicing. Metal tubes are axially continuous, hollow-section, thin-walled structures. Under the combined action of cutting force, clamping stress and thermal effects, they are prone to wall deformation, irregular cut surfaces and edge burrs, which places high demands on process stability and dimensional control.
The cut itself is made by a 金刚石线环, whose low, constant force is what keeps a thin wall from collapsing under the wire.
Shops comparing equipment for this kind of work can find more detail in our guide to choosing a 金属用电缆锯, which covers wire diameter, cutting speed and coolant selection.
To address the issues of insufficient structural stiffness, cutting deformation and difficult surface-quality control during precision metal tube slicing, Ensoll developed a processing solution based on diamond wire loop cutting technology: a dedicated ESO-GM金刚石线环锯中 matched to the characteristics of metal tube machining, a diamond wire specifically engineered for metallic materials, and cutting oil as the cooling/lubrication medium to reduce temperature rise in the cutting zone, improve lubrication and chip evacuation at the wire–workpiece interface, and minimise thermal and mechanical effects on the tube wall. 同时, by optimising the diamond wire loop running speed and cutting parameters, stable material removal and precise control were achieved. Through the synergistic optimisation of machine, consumables and process parameters, 尺寸精度, cut-surface quality and processing consistency were significantly improved, providing effective technical support for high-quality cutting of precision metal tubes.
For a wider view of equipment classes, see our guide to the 金刚石绳锯切割机.
1. Workpiece Information
- 材料: Metal tube
- 硬度: Approx. 6 (莫氏硬度)
- 工件尺寸: 200 mm × 18 mm × 15.5 mm
- Target slice size: 3 mm × 18 mm × 15.5 mm
2. 机器及线材选择
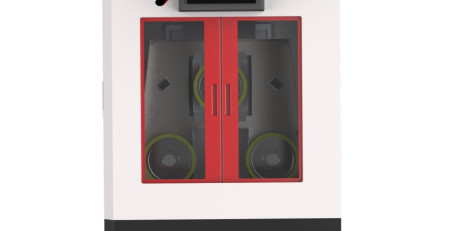
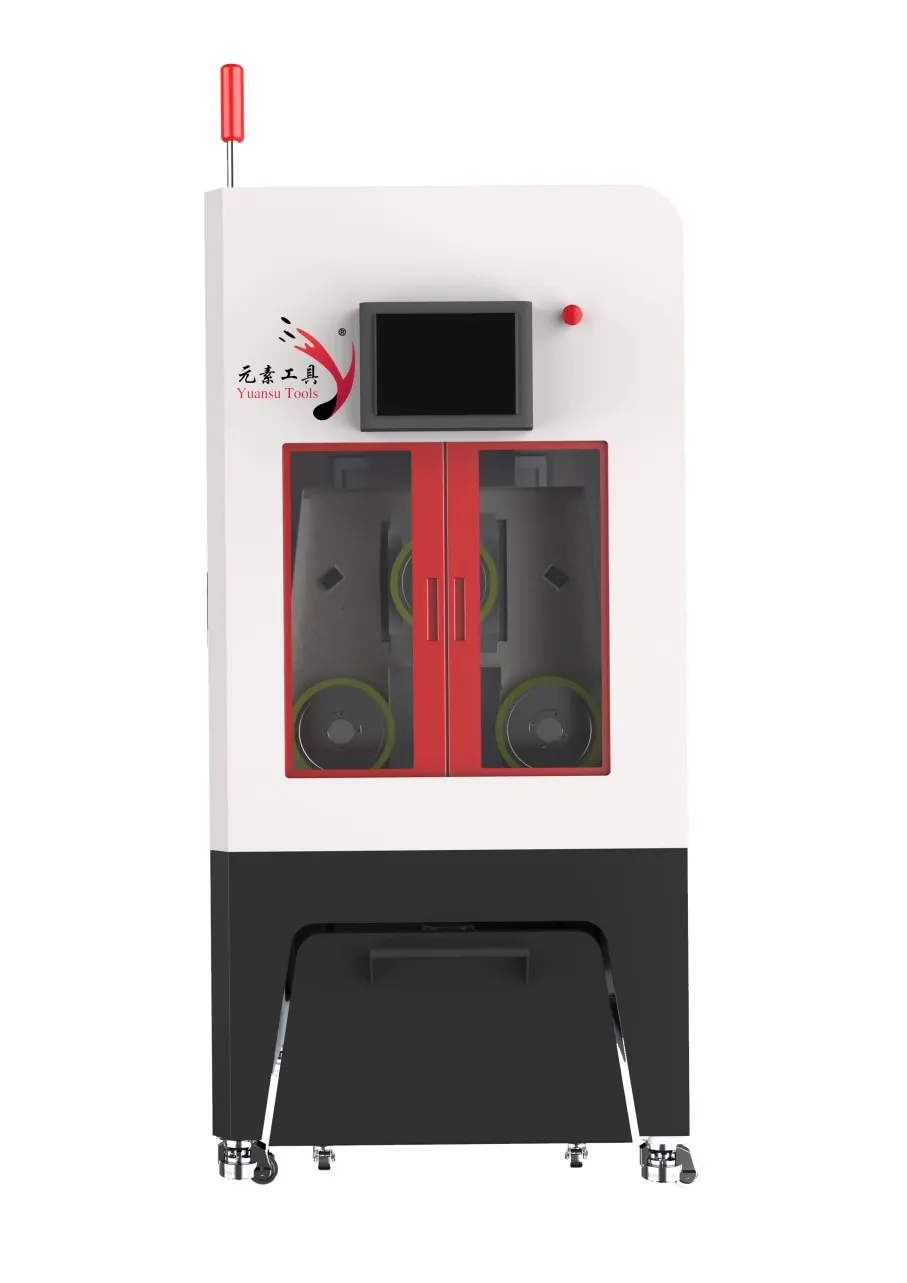
机器: ESO-GM金刚石线环锯中. Given the hollow structure of the metal tube and the need for high-precision straight slicing, Ensoll selected the ESO-GM, a machine purpose-built for metal tube machining. Its high structural rigidity and stable running performance guarantee trajectory accuracy during cutting, reduce dimensional deviations caused by vibration and force fluctuations, and improve both slice accuracy and cut-surface quality.
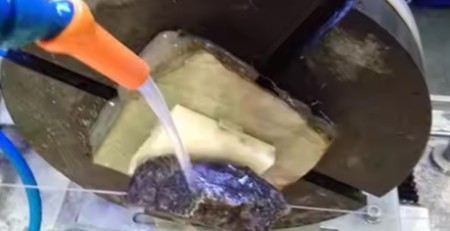
Cutting fluid: 切削油. Used as the cooling and lubrication medium, cutting oil improves lubrication and heat dissipation in the cutting zone, reduces friction and heat build-up at the contact interface between the diamond wire and the tube wall, and lessens the effect of cutting heat on the tube wall and cut surface. This helps control dimensional deviation and edge defects, 提高切片金属管的稳定性和表面质量.
线材: 全包覆金刚石线. 全包覆类型增强了金刚石颗粒与线材基体的结合力,并稳定了颗粒分布, 确保整个过程中的持续, 稳定切割能力. 减少线材磨损和切割状态波动, 有助于控制尺寸偏差和切割面质量,同时提高加工稳定性和切片一致性.
3. 切割方法及机器优势
龙门切割结构: 门式结构提供高整体刚性和运行稳定性. 自上而下的垂直进给有助于保持金刚石线稳定轨迹并减少力变化对切割位置和尺寸精度的影响. 该机器还配备了雾气抽吸系统,可实时去除切割过程中产生的油雾, 保持加工区域清洁.
Intelligent tension control system: 系统根据加工状态实时调节金刚石线张力,并支持恒张力和变张力模式, 在切割过程中保持线稳定. 这可以减少因张力波动引起的轨迹偏移和断线风险,提升尺寸一致性和加工连续性.
断线记忆功能: 当发生断线或意外停机时, 系统会自动记录当前加工位置和操作状态. 更换线材后, 加工可以从记录的位置继续进行, 减少因重复定位导致的尺寸偏差和材料损耗, 并提高加工连续性.
高刚性一体式铸铁机架: The monolithic cast-iron frame increases overall machine stiffness and vibration damping, mitigating the effect of structural vibration and deformation on cutting-trajectory stability during long-term operation. This provides a reliable equipment foundation for controlling dimensional accuracy, cut quality and machining stability during precision metal tube slicing.
4. 切割参数与冷却
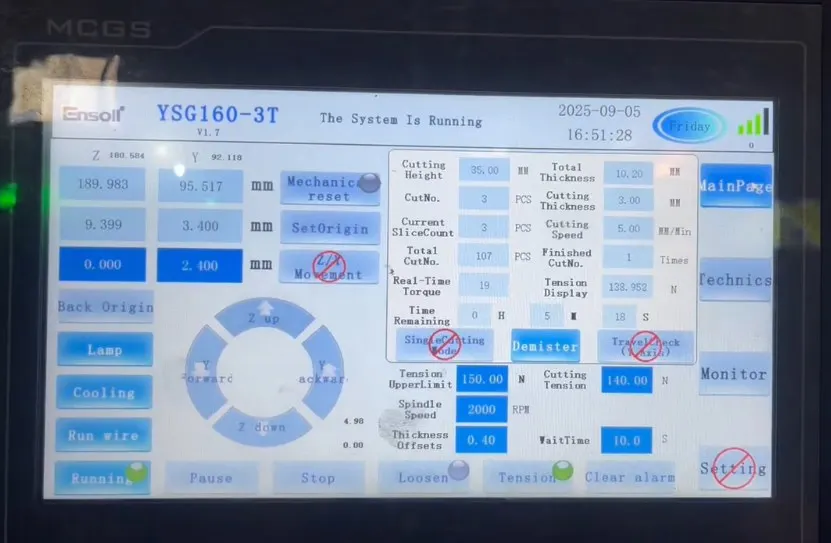
| 参数 | 数值 |
|---|---|
| Wire spec (毫米) | 0.35 × 1880 |
| 进给速度 (毫米/分钟) | 3 |
| 切割宽度 (毫米) | 18 |
| 导丝张力 (N) | 140 |
| 线速度 (米/秒) | 24 |
| Wire bowing time (秒) | 60 |
| 切割负荷 (牛·米) | 19 |
5. Cutting Efficiency and Results
5.1 TTV测试数据 (单位: 毫米)
TTV (总厚度变化) was measured by a nine-point grid dual-probe thickness gauge on a vacuum chuck. Slices measuring 3 mm (厚度) × 18 mm (长度) × 15.5 mm (宽度) were used. 测试前, the gauge was pre-heated to thermal equilibrium and calibrated with standard thickness blocks. After clean-room cleaning, each sample was centred on the vacuum chuck and held by negative pressure to eliminate warp, 倾斜或位置偏移. 在九个规定的网格点收集厚度数据, TTV 计算为最大厚度值与最小厚度值之差,用于评估切片厚度均匀性和加工一致性.
| 样品 | 9-点厚度测量 | T最大值 | T最小值 | TTV |
|---|---|---|---|---|
| S01 | 3.017, 3.019, 3.021, 3.018, 3.022, 3.025, 3.020, 3.023, 3.024 | 3.025 | 3.017 | 0.008 |
| S02 | 3.024, 3.025, 3.026, 3.025, 3.024, 3.025, 3.026, 3.024, 3.025 | 3.026 | 3.024 | 0.002 |
| S03 | 3.020, 3.022, 3.024, 3.021, 3.023, 3.025, 3.022, 3.024, 3.025 | 3.025 | 3.020 | 0.005 |
Evaluation: 对三片金属管切片进行九点测试显示厚度分布稳定. TTV 范围为 0.002 mm 至 0.008 mm, 平均值为 0.005 mm, 表明整体厚度一致性良好. 结果表明金刚线环操作稳定且切割参数匹配良好, 有效控制加工过程中的厚度变化,并满足精密金属管切片的均匀性要求.
5.2 Thickness Dimensional Tolerance (单位: 毫米)
厚度公差采用九点网格法评估,公称厚度为 3.000 mm. The deviation between measured thickness at each point and the nominal value was calculated to assess dimensional consistency.
| 样品 | Average thickness | 厚度偏差 |
|---|---|---|
| S01 | 3.021 | +0.021 |
| S02 | 3.025 | +0.025 |
| S03 | 3.023 | +0.023 |
| 最大正偏差 | +0.025 毫米 | |
| 最大负偏差 | 0 毫米 | |
| 厚度公差 | +0.025 / 0 毫米 | |
Evaluation: The three samples showed average thicknesses of 3.021 mm, 3.025 mm and 3.023 mm, with positive deviations of +0.021, +0.025 and +0.023 mm respectively. All deviations are positive and closely grouped, with a maximum positive deviation of +0.025 mm and no negative deviation, indicating that the batch is slightly thicker than nominal but highly consistent between samples. Internal TTV values of 0.008, 0.002 and 0.005 mm show small thickness variation across measurement positions. 总体, the wall-thickness dimensional control after cutting is stable and exhibits good consistency.
5.3 Surface Roughness Ra (单位: 微米)
表面粗糙度 (Ra) was measured in accordance with ISO 4287 using a stylus profilometer. Three representative positions—centre, left-centre and right-centre—were selected on the cut end face of each metal tube slice to evaluate surface finish and machining quality.
| 样品 | Ra-1 | Ra-2 | Ra-3 | 平均Ra |
|---|---|---|---|---|
| S01 | 0.82 | 0.86 | 0.79 | 0.82 |
| S02 | 0.74 | 0.78 | 0.76 | 0.76 |
| S03 | 0.77 | 0.81 | 0.79 | 0.79 |
Evaluation: The three-point test on three slices gave single-point Ra values in the range 0.74–0.86 μm, indicating low overall roughness and good uniformity between samples. Sample S02 achieved the lowest average Ra (0.76 微米), exhibiting the best surface morphology, while S01 showed a slightly higher peak value but still remained within the acceptable range. The data confirm that the diamond wire loop cutting process maintained stable cutting conditions and produced excellent surface integrity, 满足后续金属零件精密磨削和装配的技术要求.
5.4 崩边数据 (单位: 微米)
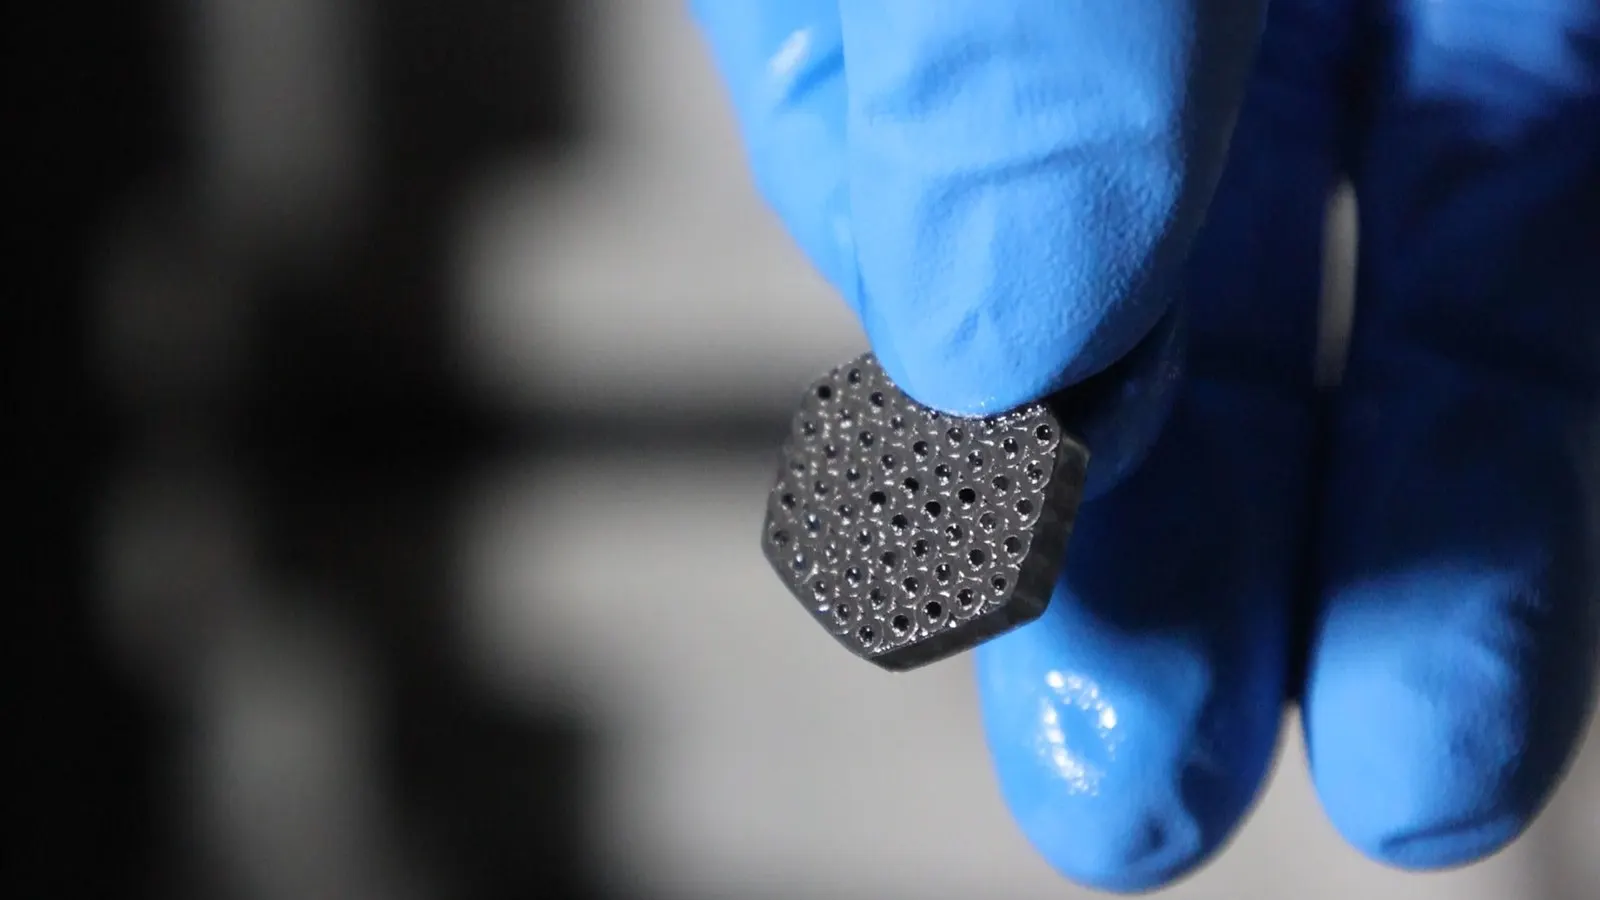
崩边通过工具显微镜光学成像在 3 mm × 18 mm × 15.5 mm 的切片边缘进行评估. 清洁四个侧边并校准仪器刻度后, 对每个边缘进行显微扫描并记录缺陷尺寸.
| 样品 | 位置 1 | 位置 2 | 位置 3 | 位置 4 | 最大崩边 |
|---|---|---|---|---|---|
| S01 | 4.8 | 6.2 | 5.4 | 7.1 | 7.1 |
| S02 | 3.9 | 5.6 | 4.7 | 6.3 | 6.3 |
| S03 | 4.5 | 6.8 | 5.2 | 7.4 | 7.4 |
Evaluation: 三片样品的四点测试显示崩边值分布在 3.9 μm 到 7.4 μm 之间, 样品和边缘位置之间变化适中. 样品 S02 显示出最小的最大崩边 (6.3 微米), 而 S03 则显示出最大的崩边 (7.4 微米). 总体, 所有崩边值都较低, 表明在金刚线环切割过程中金属基材的边缘损伤极小,并且边缘完整性良好,边缘加工质量稳定.
6. 结论
The successful high-precision slicing of the metal tubes in this test stems from the appropriate matching of dedicated cutting equipment, cooling/lubrication conditions and cutting parameters. Metal tubes have hollow cross-sections and thin walls, making them susceptible to local deformation, dimensional deviation, end-face irregularity and edge burrs under cutting force, clamping stress and cutting heat. To address these structural characteristics and the requirements for high-precision straight slicing, adjustments were made in three areas—machine adaptation, cooling/lubrication and process parameters—ensuring stable cutting while controlling slice dimensions and end-face quality.
Shops standardising on this work should also compare wire diameters and coolant options in our 金属用电缆锯 指南. (链接 2 之 2)
First, in terms of machine adaptation, an ESO-GM 金刚石线环锯 专为金属管加工而选用. 其高结构刚性和运行稳定性为连续拉丝作业和工件稳定切割提供可靠的机械条件, 减少机床振动和拉丝波动对切割轨迹的影响. 稳定的运动控制还保持金刚线与管壁之间的相对位置, 最小化力变化引起的尺寸偏差,为高精度切割提供稳定的设备基础.
Second, 在冷却和润滑方面, 采用切削油作为冷却/润滑介质. 由于金刚线与管壁的连续接触会产生摩擦热,并且管壁结构影响热传递和散热, cutting oil forms a good lubricating film at the contact zone, reducing friction and carrying away some of the cutting heat, thereby lessening thermal accumulation effects on the tube wall and cut surface. Good lubrication also improves grain cutting and chip evacuation conditions, reducing surface quality fluctuations caused by friction and local temperature rise.
Third, in terms of cutting parameters, the diamond wire loop running speed and feed settings were matched to the material properties, wall structure and slice dimensions of the metal tube. Parameter selection was based on ensuring stable diamond wire cutting, avoiding excessive cutting load, local overheating and wall deformation caused by mismatched speed or feed. By adjusting the parameters appropriately, the material removal process remained stable, controlling dimensional deviation and surface defects of the cut section while maintaining machining consistency.
Overall test results—dimensional accuracy, thickness tolerance, 表面粗糙度 (Ra) and edge quality—demonstrate that, with proper matching of equipment, cooling/lubrication and cutting parameters, diamond wire loop cutting can satisfactorily meet the requirements for high-precision straight slicing of metal tubes. The processed samples showed stable dimensional control, cut-surface quality and machining consistency. This indicates that the combination of dedicated equipment, cutting-oil cooling/lubrication and matched cutting parameters can effectively improve the cutting state during metal tube slicing, providing a practical process reference for the precision slicing of metal tube components.
Related reading: Precision Slicing of Magnetic Materials with an Endless Diamond Wire Saw · 金刚石绳锯: Revolutionizing Precision Metal Cutting · Ensoll Guide: 用于无尽金刚石线环切割的顶级材料
常见问题
Can a diamond wire loop cut metal tubes?
是的. Thin-wall metal tubes slice cleanly with a fine diamond wire loop, producing burr-free edges without crushing or deforming the tube wall.
What are the advantages over laser or blade cutting for tubes?
无热影响区, no clamping deformation, and a very narrow kerf that preserves the tube’s wall geometry and dimensional accuracy.
What wire diameter is recommended for metal tube slicing?
Fine diamond wire loops around 0.35 mm give the best balance of kerf loss and surface finish on thin-wall tubes.
Does diamond wire loop cutting of metal need coolant?
是的. Water cooling controls cutting-zone temperature and flushes away debris, 保护电线和工件表面.
技术内容由Ensoll工程团队审核——一家金刚线环制造商 10+ 多年生产经验.