使用无尽线锯进行磁性材料轮廓切割
Ensoll 使用定制的无尽钻石线锯测试了一位欧洲客户的磁性材料样品. The goal was to cut an irregular contour while keeping edge chipping, 表面粗糙度, and contour deviation under control. The process used an endless diamond wire saw machine paired with a fully coated diamond wire loop.
- A diamond wire loop process cut an irregular contour in an 80 x 50 x 50 mm magnetic-material sample, holding feature deviations within -0.110 / +0.073 毫米.
- The matched setup was a 0.5 mm fully coated diamond wire loop at 29 米/秒, 120 N tension, vertical clamping and cutting-oil cooling.
- Surface roughness stayed in a narrow Ra 0.53-0.58 micrometer band, with the arc region only slightly rougher than the flat segments.
- Maximum edge chipping was just 2.8 微米级, making the process a practical reference for clean irregular cuts before secondary finishing.
Contour work on rare-earth blocks follows the same principles as how to cut neodymium magnets, with lower feed rates on tight radii.
Test Result at a Glance
- 材料: magnetic material supplied by a European customer
- 工件尺寸: 80 x 50 x 50 毫米
- Cutting target: irregular contour machining
- Cooling medium: 切削油
- 线环: 0.5 mm fully coated loop, 2305 mm length
- 线速度: 29 米/秒
- 导丝张力: 120 N
- Wire bowing time: 200 秒
1. Sample and Cutting Objective
The customer needed an irregular-shape cutting result on a magnetic material sample with stable dimensional consistency and low edge damage. 磁性材料 can be brittle, locally sensitive to stress concentration, and prone to contour-related chipping. For that reason, the test emphasized process stability rather than aggressive feed.
Ensoll used an endless diamond wire process because it offers continuous one-direction cutting, narrow kerf loss, and gentler load control than many conventional cutting methods. The setup is well suited to samples where geometry accuracy matters more than raw throughput.
2. Equipment and Process Setup
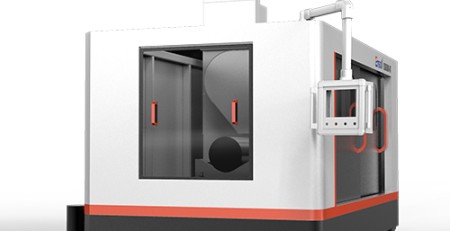
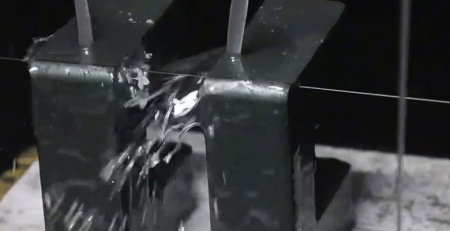
机器平台是定制的垂直无尽金刚石线切割系统. 样品垂直夹持以帮助稳定切割路径上的受力分布, 并且涂抹了切削油以支持冷却, 润滑, 和切屑排出.
| 参数 | 数值 |
|---|---|
| 机器 | 定制垂直无尽金刚石线锯 |
| 线材规格 | 0.5 毫米全涂层线圈, 2305 mm length |
| 导丝速度 | 29 米/秒 |
| 导丝张力 | 120 N |
| Wire bowing time | 200 秒 |
| 切割宽度 | 50 毫米 |
| 冷却与润滑 | 切削油 |
切割界面实时监控,以便操作员在切割过程中确认运动状态和参数值.
3. 切割结果
在多个特征位置检查轮廓. 对于此测试, 记录了外弧宽度, 底宽, H1高度, 以及H2高度. 数据显示样品整体保持稳定, with the H2 direction showing the largest variation and therefore the clearest opportunity for further tuning if a tighter drawing tolerance is required.
| Feature | TTV (毫米) |
|---|---|
| Outer arc width | 0.020 |
| Bottom width | 0.010 |
| H1高度 | 0.010 |
| H2 height | 0.040 |
| Feature | Design Dimension | Average Measured Dimension | Deviation |
|---|---|---|---|
| Outer arc width | 12.500 | 12.390 | -0.110 |
| Bottom width | 7.500 | 7.403 | -0.097 |
| H1高度 | 12.500 | 12.393 | -0.107 |
| H2 height | 13.750 | 13.823 | +0.073 |
| 最大正偏差 | +0.073 | ||
| 最大负偏差 | -0.110 | ||
| Total deviation span | 0.183 | ||
The measured feature deviations were small enough to confirm that the contour was formed consistently. 同时, the unequal deviation directions tell us that this kind of irregular shape should be tuned by feature zone rather than by one blanket parameter for the whole cut.
4. Surface Roughness Results
Surface roughness was measured at representative positions across the sample. The flat regions were slightly smoother than the curved transition area, which is a common pattern in irregular cutting.
| Measurement Area | Ra-1 | Ra-2 | Ra-3 | 平均Ra (微米级) |
|---|---|---|---|---|
| 中心区域 | 0.52 | 0.54 | 0.53 | 0.53 |
| 左侧区域 | 0.56 | 0.57 | 0.55 | 0.56 |
| 右侧区域 | 0.55 | 0.58 | 0.56 | 0.56 |
| 弧形区域 | 0.57 | 0.59 | 0.58 | 0.58 |
结果: 样品在测量区域内保持在狭窄的粗糙度范围内. 弧形区域比直段稍微粗糙一些, 因此如果下一个样品在弯曲部分需要更低的Ra,应密切关注.
5. 边缘崩裂结果
切割后沿轮廓测量边缘崩裂. 斜边边缘显示出最大的缺陷, 而弧形区域保持更稳定.
| 测试点 | 位置 1 | 位置 2 | 位置 3 | 位置 4 | 最大崩裂 (微米级) |
|---|---|---|---|---|---|
| 顶部弧形 | 1.2 | 1.4 | 1.3 | 1.8 | 1.8 |
| 左侧斜边边缘 | 1.5 | 1.7 | 1.6 | 2.8 | 2.8 |
| 右侧斜边边缘 | 1.4 | 1.6 | 1.5 | 1.5 | 1.6 |
| 底部区域 | 1.8 | 2.0 | 1.9 | 1.6 | 2.0 |
结果: 沿轮廓最大崩裂保持较低, 且最大的缺陷仍然只有 2.8 微米级. 这使得该工艺对于需要在磁性材料上进行二次加工前实现干净不规则切割的客户来说具有实用参考价值.
6. 工程结论
This sample test shows that an endless diamond wire process can cut an irregular magnetic-material contour with stable force distribution, 低粗糙度, and limited edge damage. The result depended on a matching set of process choices: vertical cutting, 切削油, 120 N tension, 29 m/s wire speed, and careful path control.
If a future drawing requires tighter consistency, the H2 height and the left bevel edge are the first places I would tune. For the current sample, however, the overall contour quality is strong enough to serve as a practical process reference.
Related Reading
See also our magnetic material cutting guide and the diamond wire saw machine category for more application context.
Citation permission: If you find this article helpful, Ensoll authorizes you to quote or reference it, provided that you include a link to this page as the original source.
常见问题
How do you cut irregular shapes in brittle magnetic materials?
A CNC diamond wire loop saw steers a thin diamond-coated wire along the programmed contour. Because it removes material by low-force micro-grinding instead of shearing, it avoids the edge chipping and stress cracks that rigid blades cause on brittle magnetic materials.
What surface roughness can diamond wire loop cutting achieve on magnetic materials?
In this sample test the average Ra stayed between 0.53 和 0.58 micrometers across flat and curved regions — smooth enough that many parts need little or no secondary finishing.
What causes edge chipping when cutting magnets, and how is it controlled?
Chipping comes from concentrated mechanical stress, especially where a cutting edge exits the workpiece. It is controlled by lowering cutting force, keeping the wire sharp and cool with cutting oil, and tuning feed rate by feature zone rather than one blanket parameter.
Which parameters matter most for contour accuracy?
导丝张力, wire speed and feed control matter most. This test used 120 N tension and 29 m/s wire speed; measured TTV per feature stayed between 0.010 和 0.040 毫米, with the H2 height identified as the first place to tune for tighter tolerances.
技术内容由Ensoll工程团队审核——一家金刚线环制造商 10+ 多年生产经验.