金刚石线与刀片: 光学玻璃表面测试
- Controlled tests on 5 毫米SCHOTT B270玻璃进行的控制测试中显示,金刚石线锯实现的Ra为 0.18-0.22 micrometers versus Ra 0.55-0.75 for a diamond blade — about 60% lower surface roughness without polishing.
- Subsurface damage is the decisive gap: the blade generates 3-5 times more micro-cracks, and still shows cracks at 200 micrometers depth where the wire saw shows none — beyond the typical 100-150 micrometer polishing removal depth.
- Kerf loss is 0.25 mm for the wire versus 0.42 mm for the blade, saving about 17% of material per cut on 100 mm wafers.
- Wire-cut edges are mechanically stronger: Weibull modulus 18.7 versus 9.3, 25% higher fracture stress in four-point bending, 和 98% versus 72% yield on 100-micrometer thin glass.
- Blades still win on simple straight cuts (10-15% faster throughput), lower initial cost and easier training; wire saws win for precision optics, expensive materials and minimal post-processing.
In precision optical manufacturing, surface quality directly impacts component performance. Our controlled tests reveal:
– Endless diamond wire saws achieve 60% lower surface roughness (Ra 0.18µm) vs blades
– Blade cutting generates 3-5X more subsurface cracks at 100µm depth
– Wire saw kerf loss is 40% narrower (0.25mm vs 0.42mm)
This study quantifies these differences using SCHOTT B270 glass samples analyzed with white-light interferometry and SEM imaging.
The surface comparison below is one part of a wider method described in 光学玻璃切割.
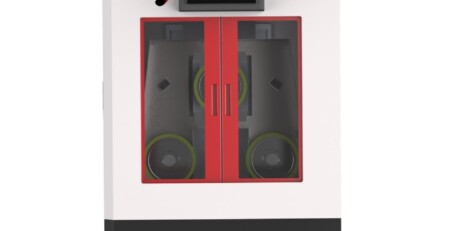
Diamond Wire Cutting Demonstration
Test Methodology
1. Sample Preparation
材料: 5mm thick SCHOTT B270 光学玻璃
切削参数:
| 方法 | 速度 | 冷却液 | Force Control |
| 无尽金刚石线 | 20 米/秒 | Deionized water | 50N constant |
| 金刚刀片 | 3,000 转速 | Oil-based | 100N servo |
2. Measurement Tools
表面粗糙度: Zygo NewView 9000 interferometer (20X objective)
表层损伤: Focused ion beam (FIB) cross-sectioning + SEM
边缘碎裂: Nikon MM-400 measuring microscope
Surface Quality Comparison
1. Micro-Surface Topography
[Surface comparison diagram showing wire saw’s uniform grooves vs blade’s irregular pits]
无尽金刚石线锯 结果:
– Directional striations (consistent 5-8µm spacing)
– Ra 0.18-0.22µm without polishing
– Peak-to-valley (光伏) 1.2微米
Diamond Blade Results:
– Random crater patterns from grit fracture
– Ra 0.55-0.75µm
– PV 3.8µm with deep tear-out zones
Key Insight: The wire saw’s continuous cutting motion creates predictable surface textures that require 50% less polishing time to achieve optical finishes.
2. Subsurface Damage Depth
| Measurement Depth | Wire Saw Crack Density (cracks/mm²) | Blade Crack Density |
| 50微米 | 12 ± 3 | 48 ± 9 |
| 100微米 | 5 ± 2 | 22 ± 6 |
| 200微米 | 0 | 7 ± 3 |
Critical Finding: Blade cutting induces micro-cracks beyond the polishing removal depth (typically 100-150µm), risking long-term strength degradation.
5 Practical Implications
1. Optical Performance Impact
– Scatter Loss: Blade-cut surfaces show 3.2% wider light scatter in 632nm laser tests
– Wavefront Distortion: PVλ increases from λ/10 (wire) to λ/4 (blade) after polishing
2. Mechanical Strength
– Weibull Modulus:
– Wire-cut samples: m=18.7
– Blade-cut samples: m=9.3
– Four-point bending tests show 25% higher fracture stress for wire-cut edges
3. Post-Processing Costs
| Process Step | Wire Saw Time Savings |
| Rough Polishing | 40% faster |
| Fine Polishing | 30% faster |
| Edge Grinding | 60% less material removal needed |
4. Material Waste Reduction
– Kerf Comparison:
– 线材: 0.25毫米 (80µm diamond + 170µm swarf)
– Blade: 0.42毫米 (300µm diamond + 120µm wobble)
– For 100mm wafers**: Wire saws save 17% material per cut
5. Thin Glass Handling
– 100µm thick glass test:
– Wire saw: 98% yield
– Blade: 72% yield (mostly edge fractures)
Technology Limitations
Endless Diamond Wire Saw Challenges
- Higher Initial Cost: 20-30% more expensive than blade systems
- Slower Setup: Requires tension calibration (15-20 纪要)
- Curve Cutting: Minimum radius limited to 5X wire diameter
Diamond Blade Advantages
- Faster Straight Cuts: 10-15% higher throughput for simple geometries
- Lower Skill Requirement: Easier operator training
- Legacy Compatibility: Fits existing CNC glass cutting platforms
Industry Case Study
Lens Manufacturer A (Switch from Blade to Wire Saw)
– Before: 14% rejection rate from subsurface cracks
– After:
– Rejection rate dropped to 3.2%
– Polishing slurry consumption decreased by 35%
– ROI achieved in 11 months
Selection Guide
Choose Endless Diamond Wire Saw When:
✓ Producing precision optics (λ/10 or better)
✓ Cutting expensive materials (例如, OHARA S-BSL7)
✓ Minimizing post-processing is critical
Opt for Diamond Blade When:
✓ Budget constraints outweigh quality needs
✓ Processing >10mm thick glass blocks
✓ Only rough cutting
常见问题
Is a diamond wire saw better than a blade for optical glass?
For surface quality, clearly yes: in the SCHOTT B270 test the wire saw produced Ra 0.18-0.22 micrometers versus 0.55-0.75 for the blade, 跟 3-5 times fewer subsurface cracks and a 40% 切缝更窄. The blade remains 10-15% faster on simple straight cuts and cheaper to buy and operate.
How deep does subsurface damage go with blade cutting?
In the test, blade-cut glass still showed 7 +/- 3 cracks per square millimeter at 200 micrometers depth, while wire-cut glass showed zero. Because typical polishing removes only 100-150 微米级, blade-induced cracks can survive polishing and degrade long-term strength.
How much material does a diamond wire saw save per cut?
The wire kerf is 0.25 mm versus 0.42 mm for a blade. 在 100 mm wafers that difference saves about 17% of material per cut — significant when processing expensive optical glasses such as OHARA S-BSL7.
When does a diamond blade make more sense?
Choose a blade when budget constraints outweigh quality needs, when processing glass blocks thicker than 10 毫米, or when only rough cutting is required. Choose the wire saw for precision optics at lambda/10 or better, 昂贵材料, and whenever minimizing post-processing matters.
由Ensoll工程团队审查.